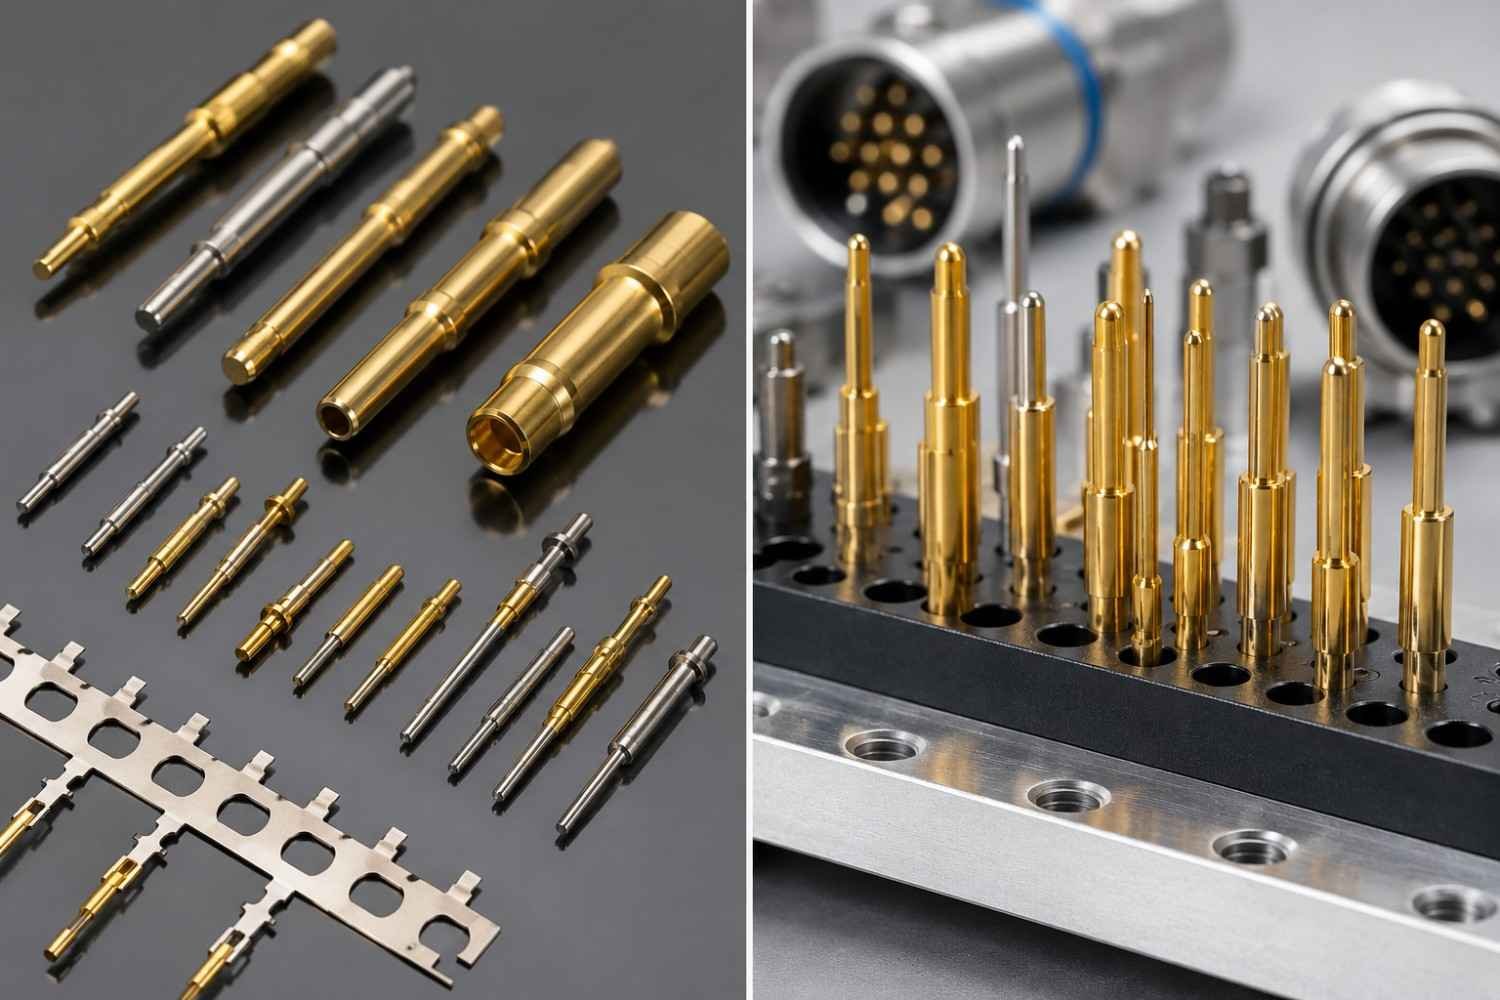
Automotive connector pins are small, cheap per piece and unforgiving in volume. A single out-of-tolerance pin can stop a harness line, and a single mixed-up part number can reach a vehicle. This case study covers 500,000 Swiss-turned pins made for an automotive wire harness programme, held to ±0.005mm and delivered in three weeks with no defects reported. The client, a connector manufacturer in Austria, has since placed its sixth repeat order.
Project at a glance
- Industry
- Automotive connectors, wire harness
- Client
- Purchasing manager, Austria
- Parts
- Machined connector pins
- Quantity
- 500,000 pins
- Process
- Swiss-type CNC turning
- Tolerance
- ±0.005mm
- Delivery
- Three weeks
- Relationship
- Sixth repeat order
- 500,000connector pins in one programme
- ±0.005mmheld on Swiss-turned features
- 3 weeksfrom order to delivery
- 0 defectsreported by the client
“Sourced 500,000 connector pins from MW+ for our automotive harness project. Swiss-turned to ±0.005mm, delivered in three weeks with no defects reported. We’re on our 6th repeat order.”
Purchasing Manager, Connector manufacturer, Austria
Why automotive connector pins are a volume problem, not a tolerance problem
Holding ±0.005mm on one Swiss-turned pin is routine for a good shop. Holding it on half a million, on schedule, with nothing mixed up, contaminated or damaged in plating, is a different discipline. Automotive connector pins fail programmes in three ways, and only one of them is dimensional.
- Drift. Tool wear slowly moves a diameter across a long run. Without statistical control, the first 50,000 pins are perfect and the last 50,000 are not.
- Mixing. Pin families look alike. Two part numbers differing by a groove position or a plating thickness can end up in the same bag, and the harness maker finds out on the crimp line.
- Surface. The contact surface carries current for the life of the vehicle. Scratches, burrs and plating defects are functional failures, not cosmetic ones.
What the client needed
The client was the purchasing manager of a connector manufacturer in Austria, sourcing pins for an automotive harness project. The order was 500,000 connector pins, Swiss-turned to ±0.005mm, needed in three weeks. Client names, part numbers and plating specifications are not published.
| Requirement | Why it matters in a harness | How it was met |
|---|---|---|
| ±0.005mm on critical diameters | Mating force, contact normal force and crimp fit | Swiss-type turning, in-process gauging, statistical control |
| 500,000 pieces in three weeks | The harness line was scheduled around the delivery | Capacity planned across parallel machines at quote stage |
| Zero defects at the customer | Automotive supply chains measure quality in parts per million | Controls against drift, mixing and handling damage |
| Plating to specification | Contact resistance and corrosion over vehicle life | Plating specification, thickness and adhesion checked per lot |
| Repeatability for future orders | Harness programmes run for years | Programme, fixtures and inspection plan retained |
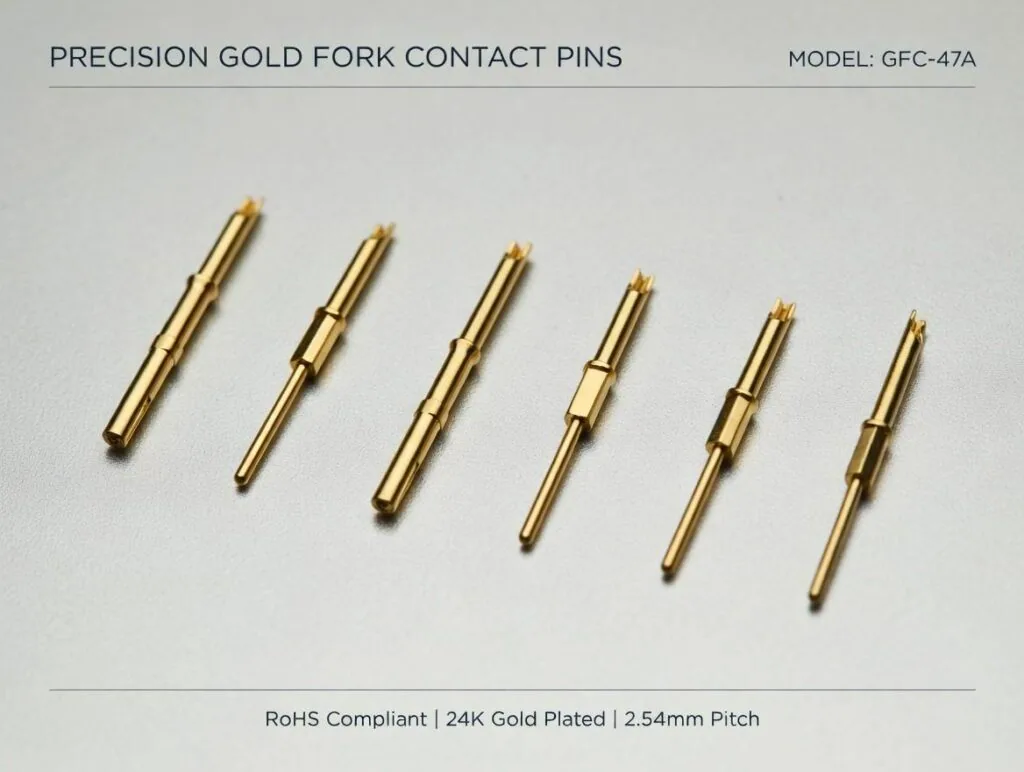
How Swiss-turned pins are made
Connector pins are the part Swiss-type lathes were built for. The bar feeds through a guide bushing, the tool cuts right next to that support, and a long, thin pin is turned complete without ever overhanging a collet. Front and back features are finished in one cycle, with the sub-spindle picking up the part for back-working. Our Swiss turning cells run pins from under Ø1mm upward.
Bar quality matters more on pins than on most parts. Swiss-type lathes need straight, round bar that fits the guide bushing closely, because any play at the bushing shows up as diameter variation on the pin. Precision-ground bar costs more per kilogram but pays for itself on a long run of Swiss-turned pins by keeping diameters stable and reducing stops.
| Step | Operation | What it controls |
|---|---|---|
| 1 | Bar inspection, certificate and lot logged | Alloy, temper and traceability |
| 2 | Turn contact diameter, shoulders and grooves | The ±0.005mm features |
| 3 | Drill or form the crimp barrel or solder cup | Wire fit and crimp performance |
| 4 | Form the contact tip radius or chamfer | Mating force and damage-free insertion |
| 5 | Part-off, back-work on the sub-spindle | Rear face and burr control |
| 6 | Clean and deburr | Surfaces ready for plating |
| 7 | Plating per specification | Contact resistance and corrosion protection |
| 8 | Final inspection, count, label and pack | Right part, right quantity, right bag |
Choosing the material for connector pins
Material choice sets conductivity, strength, machinability and cost, and it is usually fixed by the connector designer. It is still worth knowing what each option means for the machine shop, because it drives cycle time and tool life across a half-million-piece run.
| Alloy (typical) | Electrical conductivity, % IACS | Machinability | Where it is used |
|---|---|---|---|
| Free-machining brass (CuZn39Pb3 / C38500) | about 26–28 | Excellent, the benchmark | General signal and power pins |
| Tellurium copper (C14500) | about 90–93 | Good | High-current pins where losses matter |
| Phosphor bronze (C51000) | about 15 | Fair | Pins needing spring properties |
| Beryllium copper (C17200) | about 22–25 when aged | Fair, with handling controls | High-strength spring contacts |
Leaded brasses machine best, but their lead content relies on exemptions under EU RoHS and end-of-life vehicle rules that are reviewed from time to time. Confirm the current status with your compliance team when you specify the alloy. For a deeper look at alloy and geometry choices, see how to specify a machined connector pin.
Plating automotive connector pins
Plating is where many pin programmes go wrong, because it happens after machining and multiplies any surface problem the machining left behind. The main systems each suit a different duty.
| Plating system | Specification example | Typical duty | Watch-point |
|---|---|---|---|
| Gold over nickel | ASTM B488 for the gold layer | Low-voltage signal contacts, many mating cycles | Nickel underplate thickness controls diffusion and wear |
| Tin, often over nickel | ASTM B545 | Low-cost contacts, few mating cycles | Fretting corrosion under vibration |
| Silver | Customer or OEM specification | High-current contacts | Tarnish in sulphur-bearing atmospheres |
| Selective plating | Per drawing zones | Gold only where the contact mates | Zone boundaries must be defined on the drawing |
Connector systems as a whole are qualified against performance specifications such as USCAR-2, which test the assembled connector for resistance, vibration, thermal shock and more. Pins that are dimensionally perfect but badly plated will pass incoming inspection and fail that qualification, so plating thickness and adhesion are checked per lot.
Worked example: how 500,000 pins fit into three weeks
Three weeks sounds tight for half a million parts, and it is. The arithmetic shows why capacity has to be planned at the quote stage, not after the order arrives. The figures below are illustrative assumptions for a typical pin, not the client’s actual cycle times.
- Cycle time: assume 12 seconds per pin on a Swiss-type lathe.
- Effective hours: assume 20 productive hours a day per machine, after bar changes, checks and tool changes.
- Output per machine: 20 × 3,600 ÷ 12 = 6,000 pins per day.
- Machine-days needed: 500,000 ÷ 6,000 ≈ 84 machine-days.
- Machines in parallel: to finish machining in about 10 working days, 84 ÷ 10 ≈ 8 to 9 machines running the same part.
That leaves roughly a week for plating, final inspection, packing and air freight, which is itself typically 2 to 5 business days to Europe. The lesson for buyers: a three-week delivery on high-volume pins depends on the supplier committing parallel machines at quote stage. Ask how many machines will run your part.
Running the same pin on eight or nine machines also creates a risk: eight or nine slightly different processes. That is why every machine runs the same programme revision and every machine’s output is gauged and charted separately.
For the wire harness maker, the practical takeaway is to share the harness build schedule with the pin supplier. When the supplier knows which weeks the crimp lines will run, a large order can be split so that the first deliveries arrive while later lots are still being plated. That protects the wire harness line if anything slips, and it costs nothing but a conversation at the quote stage.
How zero defects was protected
“No defects reported” is the phrase in the quote that a purchasing manager values most, and it is not luck. These are the controls that protect it on a high-volume pin order.
| Risk | Control |
|---|---|
| Diameter drift from tool wear | In-process gauging and control charts per machine, Cpk target 1.67 or better |
| A bad setup running for a shift | First-off approval on every machine at every start and after every tool change |
| Mixing of similar part numbers | Line clearance between jobs, one part number per work area, sealed and labelled containers |
| Handling damage to contact surfaces | Parts collected without tumbling against each other, protective packing |
| Plating out of specification | Thickness and adhesion checks per plating lot before release |
| Wrong quantity or label | Count verification and label check at packing, lot number on every bag |
Sampling at final inspection follows an agreed plan based on ISO 2859-1, but sampling alone cannot deliver zero defects on 500,000 parts. Prevention does that. Our quality assurance system runs under IATF 16949 for automotive work, and PPAP Level 3 is available on request.
The result
The client received 500,000 connector pins, Swiss-turned to ±0.005mm, in three weeks, with no defects reported. The programme is now on its sixth repeat order. Those are the client’s own figures, as published on our homepage, and they are the only outcome claims on this page.
About this case study. The client quote is published on our homepage as given. Client name, part numbers, alloy and plating specification are not published. The capacity example uses illustrative figures, and the route and controls describe how MW+ runs high-volume pin programmes.
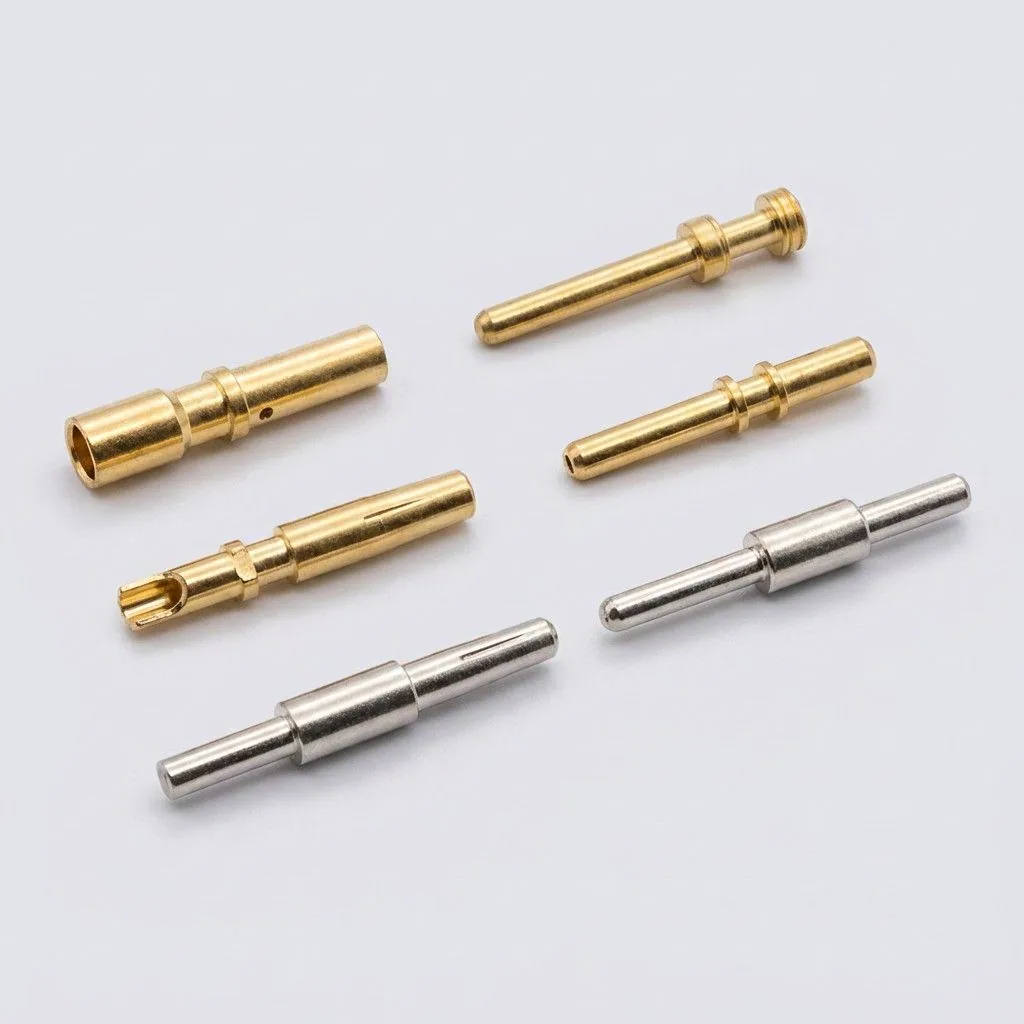
How pins are inspected at volume
A pin is too small for a hand micrometer to be the main tool and too numerous for a CMM to measure every piece. Inspection of automotive connector pins therefore uses a mix of fast gauging in the process and precise methods at release.
| Characteristic | Method | When |
|---|---|---|
| Contact and shoulder diameters | Optical shaft measurement or air gauging | First-off, then at set intervals per machine |
| Lengths and groove positions | Optical shaft measurement | First-off and sampled through the run |
| Crimp barrel bore | Pin gauges, go and no-go | Sampled per lot |
| Tip radius and chamfers | Optical profile comparison | First-off and sampled |
| Plating thickness | X-ray fluorescence to ASTM B568 | Every plating lot |
| Plating adhesion | Qualitative adhesion tests to ASTM B571 | Every plating lot |
| Burrs, scratches, plating defects | Visual under magnification | Sampled per the agreed plan |
The point of this split is speed without blind spots. Gauges at the machine catch drift within minutes, while the release checks prove the finished, plated pin meets the drawing.
How to write a connector pin drawing that quotes cleanly
Most delays on pin quotes come from drawings that leave the supplier guessing. These are the items that should always be explicit.
- Plated or unplated dimensions. State which diameters apply after plating. A 2 µm gold-over-nickel stack changes a diameter by several micrometres.
- Plating zones. For selective plating, dimension the zone boundaries, not just the word “contact area”.
- Contact surface finish. An Ra value on the mating zone, because plating copies the surface beneath it.
- Burr requirement. A clear burr limit at the crimp barrel mouth and rear face, where burrs damage wire strands.
- Material and temper. The alloy designation and temper, plus any restricted-substance requirements.
- Packing. Bulk, layered or reeled, and quantity per bag, since packing affects handling damage.
A drawing that covers these points lets a supplier quote automotive connector pins accurately the first time, with fewer questions and no surprises at first article.
What repeat orders depend on
A sixth repeat order means the process survived five handovers between batches. Four habits make that possible.
- Keep the process, not just the drawing. Programme revisions, tooling lists and gauge settings are archived with the part, so batch six starts where batch five ended.
- Re-qualify, don’t re-invent. Each new order starts with first-off approval against the drawing, not a fresh development.
- Report changes before making them. Any change to material source, plating supplier or process is notified to the client first, as IATF 16949 change control requires.
- Plan capacity with the forecast. Sharing the annual forecast lets the supplier hold machine time rather than squeeze each order in.
When Swiss turning is the wrong route for connector pins
- Stamped and formed contacts. At tens of millions of pieces a year, a stamped and rolled contact from strip is far cheaper than a turned pin, if the design allows it.
- Very simple, short pins. Pins with a length-to-diameter ratio under about 3:1 can run on conventional CNC lathes or multi-spindle automatics at lower cost.
- Press-fit pins for circuit boards. Compliant press-fit zones are usually stamped. Turned pins suit solder or crimp terminations better, as our guide to connector pins in PCB assembly explains.
Frequently asked questions
What tolerance can you hold on Swiss-turned pins?
±0.005mm on critical diameters in volume, as on this programme, with ±0.001mm possible on selected features. The limit on a pin is usually measurement and plating build-up rather than the lathe, so plated dimensions should be specified clearly.
How many connector pins can you produce per month?
It depends on the pin’s cycle time and how many machines the programme is given. This client’s 500,000 pins shipped in three weeks. Send the drawing and your volumes, and we will confirm capacity and machine allocation in the quote.
Do you plate connector pins in-house?
Plating is controlled under the same lot traceability as machining, with thickness and adhesion verified per plating lot before release. Tell us the plating system and thickness at quote stage, including any selective plating zones.
How do you prevent mixed part numbers?
Line clearance between jobs, one part number per work area, sealed and labelled containers and a label check at packing. Mixing is the most common serious defect in pin supply, so it is treated as a process risk, not an inspection problem.
Can you provide PPAP for automotive connector pins?
Yes. We work under IATF 16949, and PPAP Level 3 submissions are available on request, quoted per programme.
Which materials do you use for connector pins?
Free-machining brass, tellurium copper, phosphor bronze and beryllium copper are the common choices, plus stainless steel for some sensor pins. The connector designer normally fixes the alloy; we flag machinability and cost effects at the DFM stage.
What do you need to quote automotive connector pins?
A drawing with plated and unplated dimensions, the alloy, the plating specification, order and annual quantities, and your PPAP or documentation requirements. An engineer returns a quote and DFM feedback within 24 hours.
Sourcing pins for a harness or connector programme?
MW+ is a precision CNC machining company in Shenzhen and a connector pin manufacturer for automotive, industrial and electronics programmes. For the process side, read our guide to Swiss machined pins. For another automotive programme, see the EV housing machining case study.
Send the drawing and your volumes. You will get a price, a lead time with the machine allocation behind it, and written DFM feedback within 24 hours on your automotive connector pins.