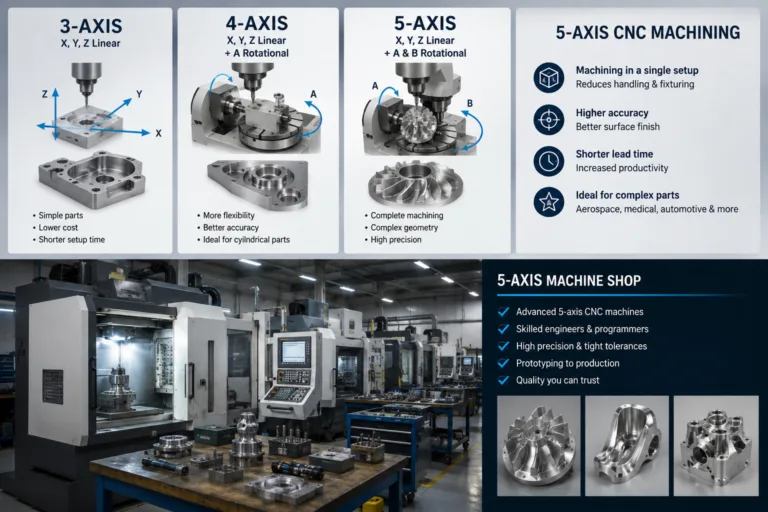
Most drawings carry a note in the title block that nobody re-reads: general tolerances per some standard, some class. That note governs every dimension the designer did not tolerance individually, which on a typical part is the great majority of them. Getting the machining tolerance standards right on precision machined parts therefore matters more than the individual callouts do — and at least one of the standards in common circulation has been withdrawn.
Key takeaways
- ISO 2768-2:1989 is withdrawn and has been replaced by ISO 22081:2021. A second edition of ISO 2768 is in publication to replace ISO 2768-1:1989.
- General tolerances are looser than engineers assume. On a 100 mm dimension, ISO 2768-m permits ±0.3 mm — a 0.6 mm zone, wider than IT11.
- ISO and ASME disagree by default. ISO GPS applies the independency principle of ISO 8015:2011; ASME Y14.5-2018 applies the envelope requirement. The same drawing means different things.
- Industry adds a second layer. AS9100D, ISO 13485 and IATF 16949 do not set tolerances; they set what evidence you must produce that the tolerance was met.
- Name the edition on the drawing. “Per ISO 2768-m” no longer identifies a single document.
On this page
- What a tolerance standard actually does
- The general-tolerance standards, and which are still current
- How loose is a general tolerance, really?
- Why does the same drawing mean different things under ISO and ASME?
- Which standards does each industry actually impose?
- Geometric tolerancing and surface texture
- What tolerance standards change about cost
- How a drawing should reference its standards
- When a tolerance standard is the wrong tool
- Frequently asked questions
What a tolerance standard actually does
A tolerance standard does three separate jobs, and confusing them is the root of most specification disputes.
It defines a vocabulary: what “flatness” means as a measurable quantity, what a datum is, how a tolerance zone is shaped. It supplies default values, so a drawing need not tolerance every dimension individually. And it sets a decision rule, stating how a measured result is compared with the specification to declare a part good or bad.
Those three jobs live in different documents. Vocabulary and geometric control sit in ISO 1101:2017 or ASME Y14.5. Default values sit in ISO 2768 and its successors, or in the drawing’s own title block. The decision rule sits in ISO 14253-1:2017. A drawing that names one and is silent on the others has left the supplier to choose, and suppliers do not all choose alike.
The general-tolerance standards, and which are still current
This is where the most common error on live drawings sits. ISO 2768 was published in two parts in 1989: Part 1 for linear and angular dimensions, Part 2 for geometrical features. Their status now differs.
| Document | Covers | Status | What to use instead |
|---|---|---|---|
| ISO 2768-1:1989 | General tolerances for linear and angular dimensions | Published; a second edition is in publication to replace it | Name the edition; watch for ISO 2768 (2nd edition) |
| ISO 2768-2:1989 | General geometrical tolerances without individual indications | Withdrawn | ISO 22081:2021 |
| ISO 22081:2021 | General geometrical and general size specifications | Published and confirmed | — |
| ISO 286-2:2010 | Standard tolerance classes and limit deviations for holes and shafts | Published | — |
| ASME Y14.5-2018 | Dimensioning and tolerancing, including general rules | Published | — |
Two practical consequences. A drawing still calling out “ISO 2768-mK” is invoking a withdrawn part for its geometrical half, and a supplier is entitled to ask what governs instead. And because ISO 22081 works differently from ISO 2768-2 — it requires a general geometrical specification to be stated rather than supplying a table of classes — migrating a drawing set is not a find-and-replace on the title block. It is a decision about what the general geometrical requirement actually is.
How loose is a general tolerance, really?
Much looser than most engineers picture. ISO 2768-1 sets permissible deviations that widen with nominal size, and at the sizes typical of machined components they are generous.
| Nominal size range | Class f (fine) | Class m (medium) | Class c (coarse) | Class v (very coarse) |
|---|---|---|---|---|
| 6 to 30 mm | ±0.10 mm | ±0.20 mm | ±0.50 mm | ±1.00 mm |
| over 30 to 120 mm | ±0.15 mm | ±0.30 mm | ±0.80 mm | ±1.50 mm |
| over 120 to 400 mm | ±0.20 mm | ±0.50 mm | ±1.20 mm | ±2.50 mm |
| over 400 to 1000 mm | ±0.30 mm | ±0.80 mm | ±2.00 mm | ±4.00 mm |
Worked example: a general note against the ISO 286 grades
Take a 100 mm dimension and express each tolerance as a total zone, then compare it with the standard tolerance grades of ISO 286-2:2010, which for the 80–120 mm range are IT9 = 87 µm, IT10 = 140 µm and IT11 = 220 µm.
- ISO 2768-m: ±0.30 mm, a 600 µm zone — wider than IT11 by a factor of nearly three.
- ISO 2768-f: ±0.15 mm, a 300 µm zone — still wider than IT11.
- A specific callout of ±0.05 mm: a 100 µm zone, sitting between IT9 and IT10.
- A specific callout of ±0.005 mm: a 10 µm zone, tighter than IT5 at this size.
The general note, in other words, constrains almost nothing on a machined part; ordinary milling and turning clear it without effort. Everything that costs money on the drawing is in the individual callouts, and the gap between the note and a tight callout is not one grade but five or six. That is why a drawing review that reclassifies two dimensions from specific back to general usually saves far more than tuning the general class does. The sibling article on what ±0.005 mm means in production works through the other end of that range.
Why does the same drawing mean different things under ISO and ASME?
Because the two systems have opposite defaults on the relationship between size and form, and neither prints that default on the drawing.
Under ASME Y14.5, Rule #1 — the envelope requirement — applies unless the drawing says otherwise: a feature of size at maximum material condition must fit within a perfect-form boundary, so the size tolerance implicitly limits form. Under ISO GPS, the fundamental rule is independency, stated in ISO 8015:2011: size and form are independent requirements unless the envelope requirement is explicitly invoked on the drawing.
| Question | ASME Y14.5-2018 default | ISO GPS default |
|---|---|---|
| Does a size tolerance limit form? | Yes — Rule #1, the envelope requirement | No — independency principle, ISO 8015 |
| How is the opposite obtained? | State independency on the feature | Apply the envelope modifier to the feature |
| Which document defines the geometric symbols? | ASME Y14.5 | ISO 1101 and the related GPS parts |
| Which document defines the conformity decision? | Stated by the drawing or the contract | ISO 14253-1, unless agreed otherwise |
The practical failure is a bent or tapered shaft that measures in size at every cross-section. Under ASME it fails on Rule #1; under ISO, with no form control added, it conforms. Neither answer is wrong — but a drawing that names ASME Y14.5 in the title block while the design office works to ISO habits will eventually produce a part that both sides believe is correct and neither can use. Naming the system is a five-word change that removes an entire class of dispute.
Which standards does each industry actually impose?
A common misreading is that AS9100D or ISO 13485 sets tolerances. They do not. They set what evidence must exist that the tolerance on the drawing was met, who may approve a change to it, and how long the record must be kept. Tolerance values come from the drawing; the sector standard governs the paperwork around them.
| Sector | Quality system normally required | What it adds on top of the drawing |
|---|---|---|
| Aerospace and defence | AS9100D, with special processes under NADCAP | First article inspection to AS9102, full configuration control, and no unapproved process change |
| Medical devices | ISO 13485:2016 | Design history and device master records, validated processes, traceability to the lot |
| Automotive | IATF 16949, which replaced ISO/TS 16949 | PPAP submission, control plans, and a stated capability index on designated characteristics |
| General industrial | ISO 9001:2015 | Documented inspection and control of non-conforming output |
Where sampling replaces full inspection, the plan should be named rather than assumed: ISO 2859-1:2026, which supersedes the 1999 edition, is the usual reference for inspection by attributes indexed by acceptance quality limit. And where a capability index is required, it should be stated against a named characteristic, because a Cpk figure without a characteristic is not a commitment. MW+ works to Cpk ≥1.67 on controlled characteristics and holds ISO 9001:2015, AS9100D, ISO 13485, IATF 16949 and NADCAP approvals, which is what makes the evidence layer above possible rather than aspirational.
Geometric tolerancing and surface texture
Two further standard families attach to almost every precision drawing, and both have moved recently enough that drawings in circulation disagree.
Geometric tolerancing
ISO 1101:2017 and ASME Y14.5-2018 both define form, orientation, location and run-out controls, and both express them in feature control frames. They are not interchangeable in detail: datum reference systems, the treatment of material condition modifiers, and the interpretation of profile tolerances all differ. A drawing should name one and use it consistently. In practice, a geometric control is very often what the function requires, and tightening a size tolerance instead is a costly and indirect substitute.
Surface texture
The profile surface-texture standards were reorganised in 2021. ISO 21920-2:2021 now defines the parameters, superseding ISO 4287; ISO 21920-3:2021 covers specification operators including sampling length and filtering, superseding ISO 4288; and ISO 21920-1:2021 covers drawing indication, superseding ISO 1302. Drawings still circulate under both conventions, and a bare “Ra 0.8” without a sampling length is ambiguous under either. MW+ produces Ra 3.2 µm as-machined, Ra 0.4 µm fine-machined and Ra 0.1 µm polished, and the parameter set that governs should be stated so that the measurement matches the intent.
What machining tolerance standards change about cost
Standards do not have a price, but the choices they force do. Four mechanisms account for nearly all of it.
Process selection. A tolerance grade that milling and turning cannot hold repeatably pushes the feature to grinding, honing or a second finishing operation, which is a change of route rather than a change of speed.
Inspection scope. A general tolerance can be verified by sampling with hand instruments. A tight geometric callout needs a coordinate measuring machine, a documented measurement uncertainty and a longer routine per part. The instrument’s capability is established under ISO 10360-2:2009, and the uncertainty it reports is subtracted from the tolerance under ISO 14253-1 before conformity can be declared.
Documentation. Sector standards add first article reports, control plans and traceability records, all of which take engineering time whether or not a single part is rejected.
Rework and disposition. Tighter bands produce more borderline parts, and each borderline part needs a decision, which needs a person. That cost is usually invisible in a quote and very visible in a schedule.
None of these is a reason to avoid tight tolerances where they are needed. They are reasons to apply them only where they are, which is why CNC precision parts are best specified feature by feature rather than by tightening a whole drawing. The related guide on specifying tolerance in an RFQ covers how to put this into a purchasing document.
How a drawing should reference its standards
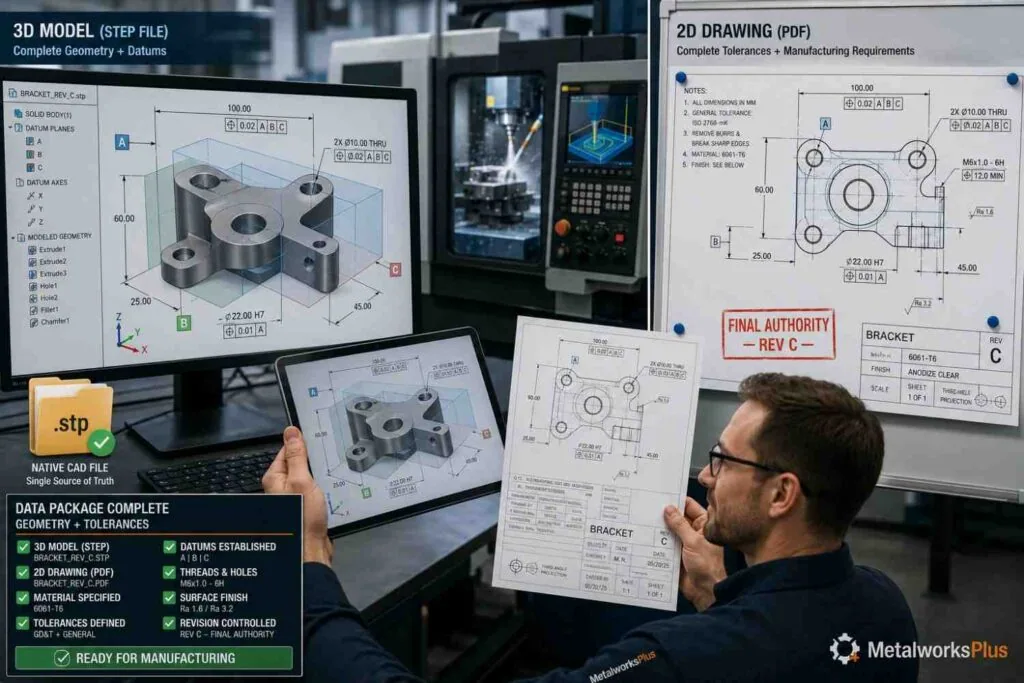
Six lines in the title block settle almost everything a supplier would otherwise have to guess.
| What to state | Why it matters |
|---|---|
| Dimensioning system and edition — ISO GPS or ASME Y14.5-2018 | Sets whether size limits form by default |
| General linear tolerance standard, class and edition | Governs every untoleranced dimension on the part |
| General geometrical requirement | ISO 2768-2 is withdrawn; ISO 22081 requires a stated specification |
| Surface texture parameter, value, sampling length and governing edition | Removes the ambiguity between the ISO 4287 and ISO 21920 conventions |
| Decision rule for conformity, and the reference temperature | Determines how measurement uncertainty is handled at inspection |
| Which characteristics are critical to function | Directs inspection and capability effort where it is earned |
MW+ quotes from STEP, IGES, DXF, DWG, SolidWorks and PDF files and returns a quotation within 24 hours; where a drawing is silent on these six points, the reply will normally ask about them before the price, because the answers change the process. You can request a CNC machining quote with the drawing attached, and CNC machining quality control is set up around exactly these references rather than a generic inspection routine.
When a tolerance standard is the wrong tool
Standards are defaults, and defaults are wrong often enough to be worth checking. Four cases.
The general class is too loose to be useful
On a part where most dimensions genuinely matter, a general note at class m is a formality that constrains nothing, and the drawing ends up carrying a specific tolerance on nearly every dimension. At that point the general note is noise; a tighter class, or a stated per-drawing default, communicates the intent better.
The geometry is not what the standard assumes
General tolerance tables are built around prismatic features with ordinary proportions. Thin-walled, long and slender, or freeform parts move under their own weight and clamping, and a table-derived limit may be unachievable in a way the standard never contemplated. Those parts need an agreed measurement set-up as much as a tolerance value.
The sector standard is being used as a tolerance
“Must be AS9100” is not a dimensional requirement, and a supplier cannot machine to it. Sector standards govern evidence. If the real requirement is a capability index or a first article report, say that instead; it is cheaper to satisfy and unambiguous.
Conformance would depend on a measurement nobody can make
Where the available instrument’s uncertainty is a large fraction of the tolerance, most conforming parts cannot be proven conforming and the specification generates disputes rather than quality. Either the measurement capability rises or the tolerance widens; a standard reference does not resolve it. The comparison of ±0.01 mm against ±0.005 mm is a useful check before committing, and the requirements for holding ±0.001 mm show where the limit genuinely sits.
Frequently asked questions
Our drawings all say ISO 2768-mK. Do we have to change them?
Not urgently, but you should decide what the K class now means to you. The K refers to ISO 2768-2, which is withdrawn, so the reference no longer points to a live document. The options are to state an equivalent general geometrical specification under ISO 22081, to replace the general geometrical note with explicit controls on the features that need them, or to keep the legacy reference and agree with each supplier what it means. The first two are more durable; the third works until a dispute.
Is ISO 2768 the same as an IT grade?
No. ISO 2768 gives permissible deviations for untoleranced dimensions by size range and class; ISO 286 gives standard tolerance grades used to build fits between holes and shafts. As the worked example above shows, a general class on a 100 mm dimension is several grades looser than IT11. They serve different purposes and appear in different places on a drawing.
Which system should a new drawing set use, ISO or ASME?
Choose by where the parts will be made and reviewed rather than by preference. Both are complete and rigorous. What causes problems is mixing them — ASME symbols with ISO defaults, or an ISO title block on a drawing whose author assumed Rule #1. Pick one, state it, and train to it.
Does a tighter general class improve quality?
Rarely, and it can reduce it. Tightening the general class raises inspection effort across every untoleranced dimension, which dilutes attention from the features that actually control function. Concentrating effort on a small number of identified critical characteristics produces better outcomes than spreading it evenly.
What should a supplier send back as evidence?
A dimensional report keyed to the drawing, with measured values rather than pass flags, the instrument used and its stated uncertainty, and the temperature or a statement of thermal equilibrium. Where a sector standard applies, add the first article report or PPAP package it calls for. Every MW+ order ships with a certificate of conformance, a CMM inspection report and material certificates, with AS9102 first article inspection or PPAP Level 3 quoted per programme.
Do plastics and castings use the same standards?
The geometric and surface-texture standards apply broadly, but general dimensional tolerances do not transfer. Moulded, cast and welded components have their own general tolerance standards reflecting how those processes behave, and applying a machining table to them produces requirements that no process can meet. Where a machined feature is added to a cast or moulded blank, the machined feature takes the machining standard and the rest does not.
How do these standards interact with volume?
The standards themselves do not change with quantity, but the evidence burden does. At prototype quantities a first article report and full dimensional inspection are proportionate; at volume, capability data and a sampling plan carry the argument more efficiently. MW+ delivers standard prototypes in 3–5 business days, 48-hour express where needed, and volume production in 10–15 business days, with no minimum order quantity — and the documentation set changes shape across that range even though the drawing does not. Larger programmes are covered under machine parts manufacturing, and general capability under CNC machining services.