Microfluidic channel design should connect the required flow to the finished channel geometry, fluid properties and available pressure. For a first calculation, use a defined hydraulic-resistance model; for manufacture, specify the channel profile and an inspection plan that can verify it. Hydraulic resistance relates the pressure difference across a flow path to its volumetric flow rate. The chip, connecting tubing and fittings must be considered as parts of the fluidic system. [1]
Illustrative application guide: This is a design-review exercise, not a completed MetalWorksPlus customer project. Every dimension, tolerance, fluid property and operating point used below is assumed. Calculated values are predictions for an ideal channel, not measured results, production capabilities, a pressure rating or biological performance. The recommendations describe questions to resolve before releasing a microfluidic prototype.
Contents
Define the fluidic system and controlled feature
Start the review with a one-page requirements sheet. Identify the working fluid, intended temperature range, required flow at the relevant outlet, pressure-measurement locations and whether the controller will regulate flow or pressure. Mark the inlet, outlet and any branches on the drawing. Fluigent distinguishes channel resistance inside the chip from the resistance of external connections; a channel-only calculation should therefore not be labelled as the pump requirement. [1]
For this exercise, consider one straight groove that will be closed by a rigid cover. Treat the assembled fluid passage as the controlled feature. Ask the designer to identify which drawing controls the base, cover, their relationship and the final internal height. Do not silently equate a depth measured on an open part with an accepted assembled channel. If a bonding layer, gasket or cover deformation is part of the proposed construction, assign responsibility for assessing it before using the ideal calculation.
Keep the application boundary explicit. A useful review package states whether the immediate objective is geometry verification, a flow experiment or a complete functional demonstration. For this example, the objective is comparing dimensional choices for a straight passage. It does not include a mixing requirement, optical performance, cell compatibility, sterility or a validated seal. Each additional objective needs its own evidence and acceptance plan.
Choose a hydraulic-resistance model and keep units consistent
For a rectangular channel with height h smaller than width w, the approximation used here is:
Rh ≈ 12 μ L / [w h3 (1 − 0.63 h/w)]Δp = Rh Q
Here, Rh is hydraulic resistance in Pa·s/m³, μ is dynamic viscosity in Pa·s, L is channel length in m, w and h are in m, Q is volumetric flow in m³/s and Δp is pressure difference in Pa. Dilissen and colleagues present this resistance approximation in Equation 6 of their methods section. It is used here only as a mathematical reference; their fabricated device and experiments are not MW+ project evidence. [2]
The teaching model assumes a long, rigid, uniform rectangular passage, fully developed steady flow of an incompressible Newtonian liquid, constant viscosity and no slip at the walls. MEMSolver’s rectangular-channel documentation identifies the long, narrow-channel, rigid-wall and low-Reynolds-number limitations of this type of resistance calculation. Use the present example for its shallow cross-sections, rather than extending the approximation to arbitrary profiles or near-square channels without review. [3]
Assumed common inputs: width 1.000 mm; length 50.0 mm; viscosity 1.00 mPa·s; density 1,000 kg/m³; flow 10.0 µL/min. These are convenient hypothetical inputs, not certified properties of a named fluid. A real calculation should identify the fluid-property source and its applicable temperature and composition.
Convert before substituting: 1.000 mm = 0.001000 m; 50.0 mm = 0.0500 m; 1.00 mPa·s = 0.00100 Pa·s; and 10.0 µL/min = 1.6667 × 10⁻¹⁰ m³/s. The pressure calculation then has units of (Pa·s/m³) × (m³/s) = Pa. Keep full precision internally and round the displayed results only at the end.
Compare three assumed channel depths
The first table asks a practical design question: what changes in this ideal passage when depth changes but width, length, fluid properties and imposed flow stay fixed? Channel volume is calculated as V = w h L; mean velocity is u = Q/(w h). These are geometric calculations for the assumed rectangular section. Rounded corners, ports, junctions and connecting tubing are excluded.
For an additional model check, calculate Dh = 2 w h/(w + h) and Re = ρ u Dh/μ, using mean velocity for u. Equations 4–5 in the cited paper define Reynolds number and rectangular-channel hydraulic diameter. [2]
| Assumed depth (µm) | Calculated channel Δp (Pa) | Calculated channel volume (µL) | Calculated mean velocity (mm/s) | Calculated Re (dimensionless) |
|---|---|---|---|---|
| 100 | 106.72 | 5.00 | 1.667 | 0.303 |
| 150 | 32.72 | 7.50 | 1.111 | 0.290 |
| 200 | 14.30 | 10.00 | 0.833 | 0.278 |
The pressure values use the resistance equation above. [2] The other columns are derived from the stated inputs. At 100 µm, for example, Rh is approximately 6.4034 × 10¹¹ Pa·s/m³. Multiplying by the converted flow gives 106.72 Pa across the modelled channel.
Read the table as a trade study. Within these assumptions, increasing depth reduces the predicted pressure requirement while increasing contained volume and reducing mean velocity at the same flow. The low calculated Reynolds numbers are consistent with the viscous-flow premise of this example; they do not validate the actual assembled device. Do not select the deepest option solely because its calculated pressure is smallest. Bring the required sample volume, flow behaviour and manufacturable profile back into the decision.
Check microfluidic channel dimensions at fixed pressure
The second table asks a different question: if the controller holds pressure constant, how does an assumed depth variation affect predicted flow? Set the pressure difference to the nominal result for the 100 µm channel, shown here as 106.7236 Pa; retain the full calculated value internally. Hold width, length and viscosity fixed. Consider a hypothetical depth specification of 100 ± 5 µm. This tolerance is an exercise input, not a recommendation or an MW+ capability claim.
| Assumed actual depth (µm) | Calculated resistance change from nominal (%) | Calculated flow at fixed pressure (µL/min) | Design-review question |
|---|---|---|---|
| 95 | +16.24 | 8.60 | Can the application accommodate this lower predicted flow? |
| 100 | 0.00 | 10.00 | Is this assumed nominal operating point appropriate? |
| 105 | −13.32 | 11.54 | Can the application accommodate this higher predicted flow? |
For each row, recompute resistance with the same approximation, then calculate Q = Δp/Rh. [2] The percentage is 100 × (Rh/Rnominal − 1). The asymmetric results come from the model equation; a symmetric dimensional interval does not produce a symmetric flow interval.
Use this result to choose the next review step. If a proposed application cannot accommodate the calculated range, revisit the dimensional budget or operating approach before requesting a tighter tolerance. This is a one-variable sensitivity study. It is not a worst-case assembly stack because width, length, fluid viscosity, cover behaviour and measurement uncertainty have not been varied. A real tolerance study should state which variables are held fixed and which combinations are being evaluated.
Prepare the microchannel machining drawing around the finished profile
Published micromilling research distinguishes directly machining a microfluidic device from machining a mould used to produce one. Guckenberger and colleagues describe micromilling as a prototyping route for plastic microfluidic devices and discuss practical fabrication considerations. Their reported equipment, materials and achieved results must not be transferred to another supplier as guaranteed capability. [4]
Identify the route and dimension the relevant surfaces
State whether the supplied component is the fluid-contacting part, a mould or an intermediate prototype. For a direct-machined base, show the channel section and identify the datum used for depth. For a mould, ask the team to document how the eventual device dimensions will be established. Keep those routes separate in the drawing revision and inspection request.
Provide both nominal geometry and functional limits. Ask the manufacturer to mark any proposed changes to corner radii, floor profile, channel ends or port transitions rather than interpreting an ideal rectangle as permission to substitute a different cross-section. If the offered profile differs from the analytical section, require a revised model or an agreed comparison method. Do not approve the geometry solely from a top-view image.
Resolve access, edges and material condition before quotation
Use the micro-machining service page as the starting point for discussing the feature package. Ask for a review of tool access, proposed machining sequence, workholding, edge treatment and how the specified profile would be checked. Request application-specific confirmation of the proposed dimensions instead of treating the example’s 100 µm depth as a published minimum.
Specify the material and relevant delivered condition. Ask who will approve contact with the intended fluid, cleaning chemistry and closure method. Where those decisions remain open, mark them as unresolved rather than inserting a generic “compatible” statement. Likewise, identify the channel regions where burrs, residue or edge treatment need explicit review. Agree on an acceptance description and a way to observe it; “deburr completely” alone is not a complete inspection instruction for this prototype.
Separate dimensional inspection from assembled flow validation
Build two linked records. The first concerns the manufactured component: drawing revision, material record, width, depth, length, profile and agreed visual checks. The second concerns the assembled experiment: cover configuration, fluid identity and condition, pressure locations, commanded operating point, observed flow and any leakage observation. Treat these as proposed records for the application, not evidence that MW+ has performed the tests.
Ask how the critical dimension will be measured
Request the proposed measurement method, accessible surfaces, sampling locations and uncertainty information before accepting a tolerance. For example, ask whether depth will be assessed at the channel entrance, middle and exit, and whether the method can distinguish the specified floor from nearby surface features. These are review questions, not prescribed sampling quantities or a claim that a particular instrument is suitable.
Record the difference between a nominal CAD section and the inspected profile. If a nonuniform result is found, retain the position information rather than averaging it into an apparently conforming single value without engineering review. Decide in advance who will judge deviations and whether the fluid model needs updating.
Write a reproducible flow-check plan
For the prototype experiment, document where pressure is measured and what external components are installed. Fluigent’s pressure/flow guidance treats the fluidic path as a combination of internal and external resistance; this supports recording tubing and connection details when interpreting a result. [5] Specify the intended stabilization criterion, measurement method and acceptance band through the responsible engineering team. Do not create a pass limit from the example’s rounded calculations.
If observed flow differs from prediction, use a structured comparison: verify the input values, actual profile, assembled configuration and measurement arrangement before assigning a cause. A dimensional inspection report, a leak observation and a flow measurement answer different questions. Preserve each result with its conditions rather than allowing one to stand in for all three.
Release a reviewable microfluidic prototype package
Before requesting manufacture, confirm that the package identifies the intended fluid, controlled geometry, dimensional limits, closure responsibilities, unresolved material questions, proposed inspection and planned assembly test. Keep assumed quantities visibly marked. Attach the calculation with units and revision so a reviewer can reproduce both tables or replace the inputs.
For component context, review precision machined components alongside the drawing. Then discuss the channel, cover and inspection requirements through MW+ CNC manufacturing services. Send MetalWorksPlus the drawing revision, material request, expected prototype quantity and the open technical questions. Ask for a feature-specific feasibility response; this guide establishes no quotation, qualification or guaranteed process window.
Frequently asked questions
What channel depth should I specify?
Use the required fluidic behaviour and the complete assembly to develop a candidate geometry, then review manufacture and inspection. The three depths in Table 1 are assumed comparison points, not preferred sizes or a universal design range.
Does a 100 µm groove guarantee the calculated flow?
No. The example uses a defined rectangular passage and fixed assumed inputs. Compare the actual assembled profile and operating conditions with those assumptions before using the calculation as a prediction for a device.
Can the pressure in Table 1 be used as a pump setting?
It represents the calculated difference across the ideal channel only. Include the external fluidic path and pressure-measurement arrangement in the system review before specifying a pump setting. [1]
Is the second table a production tolerance recommendation?
No. It demonstrates a sensitivity calculation using an invented ±5 µm interval. Select an actual tolerance through functional analysis, a manufacturability discussion and a suitable inspection plan.
Does this guide demonstrate an MW+ microfluidic project?
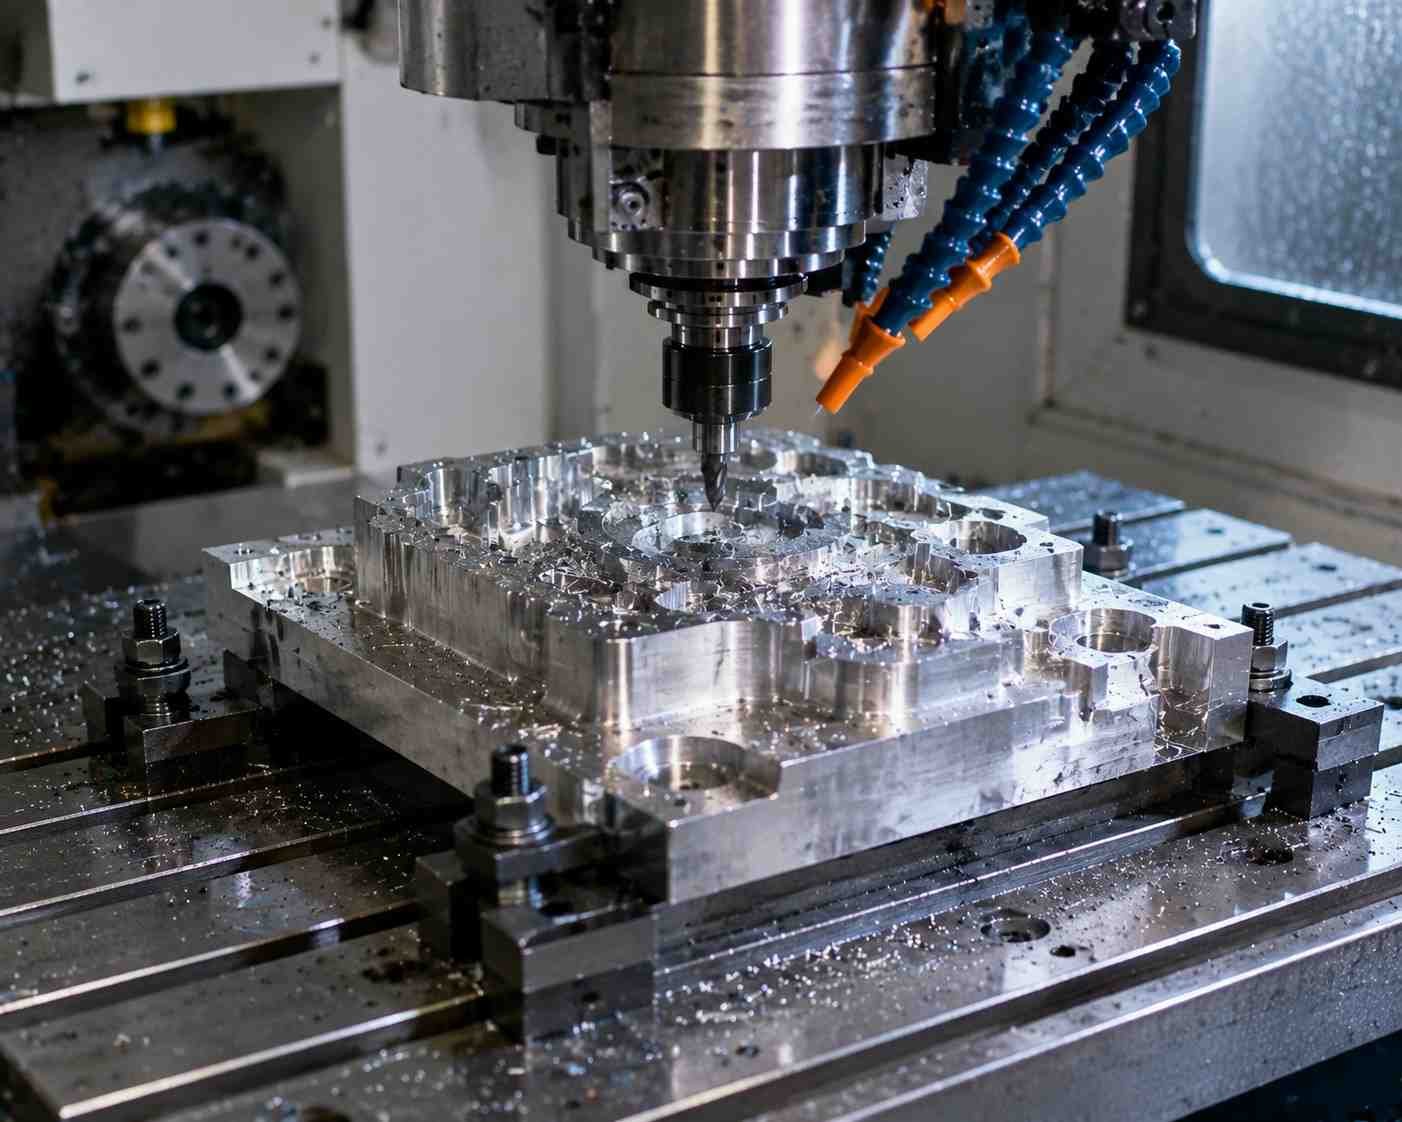
No. It is an illustrative engineering study. The process photograph provides milling context and does not document the modelled channel, a customer device or a measured flow test.
Technical references and evidence boundaries
- Fluigent: Microfluidic resistance. Manufacturer explanation of pressure, flow and internal/external fluidic resistance.
- Dilissen et al.: Characterisation of biocondensate microfluidic flow using array-detector FCS, BBA General Subjects 1868 (2024), 130673, DOI 10.1016/j.bbagen.2024.130673. Equations 4–6 are the mathematical references; experimental and biological findings are outside this guide’s claims.
- MEMSolver: Rectangular channel resistance. Official model documentation and applicability assumptions.
- Guckenberger et al.: Micromilling: a method for ultra-rapid prototyping of plastic microfluidic devices, Lab on a Chip 15 (2015), 2364–2378, DOI 10.1039/C5LC00234F. Fabrication-method context; author record also available through PubMed. Reported process results are not MW+ capabilities.
- Fluigent: Flow-rate-to-pressure calculator guidance. System-resistance and calculation-input context.
References checked 30 October 2026. Calculations are independently reproduced from the stated assumptions; no measured customer or MW+ project data are presented.