Alloy selection is a machining decision before it is a metallurgical one. The grade you write on the drawing sets the cutting speed, the tool life, the achievable tolerance, the number of passes and, in several cases, whether the feature can be cut at all. Choosing it purely on a strength number and leaving the shop to cope is how a part becomes expensive for reasons nobody can trace back to a decision.
This guide is written for the engineer specifying a machined industrial component — a valve body, a pump housing, a shaft, a bracket that carries load at temperature. It gives nominal properties with units, the machining limits each family runs into, and the situations where the tougher alloy is the wrong answer. For the process range behind these limits, see MW+ CNC machining services.
Key takeaways
- Thermal conductivity predicts machining difficulty better than strength does. Ti-6Al-4V carries a nominal thermal conductivity near 6.7 W/m·K against roughly 167 W/m·K for aluminum 6061-T6, so the heat stays in the cutting edge instead of leaving in the chip.
- Work hardening, not hardness, is what defeats tools in austenitic stainless and nickel superalloys. A rubbing tool creates the hard layer that destroys the next pass, which is why light cuts are the wrong instinct in these grades.
- MW+ machines 70+ grades and holds general machining to ±0.01mm under ISO 2768-m, precision features to ±0.005mm and critical features to ±0.001mm, at a process capability of Cpk ≥1.67.
- Surface finish runs from Ra 3.2µm as-machined, to Ra 0.4µm fine-machined, to Ra 0.1µm polished. Roughness parameters are defined in ISO 21920-2 (superseding ISO 4287); state which parameter you mean, not just a number.
- Property values published in references such as MatWeb are nominal. When a property is load-bearing, design against the actual mill certificate for the heat you receive, not against a table.
- Every MW+ order ships with a certificate of conformance, a CMM inspection report and material certificates traceable to the mill heat, against the relevant ASTM material specification.
- How do you choose an alloy for a machined industrial component?
- Nominal properties of common industrial alloys
- What makes an alloy hard to machine?
- The five alloy families and what each is actually for
- What tolerance and surface finish can each process hold?
- Should a part be machined before or after heat treatment?
- Material certification and traceability
- When the high-performance alloy is the wrong choice
- Frequently asked questions
How do you choose an alloy for a machined industrial component?
Choose an alloy by working through four constraints in order: the service environment the part must survive, the mechanical property that actually governs the design, the manufacturing route the geometry forces, and the availability of the grade in the form and size you need. Reversing that order — picking a familiar grade first and checking service life afterwards — is the origin of most late material changes.
The governing property is usually one thing, not a list. A pressure-retaining body is governed by yield strength at temperature, a rotating shaft by fatigue, a sealing face by hardness and surface integrity. Naming it makes the shortlist short.
| Constraint | Question to answer | What it eliminates |
|---|---|---|
| Service environment | Peak and continuous temperature, chemistry, chloride or sour service exposure | Grades that corrode, creep or embrittle in that environment |
| Governing property | Which single property fails first — yield, fatigue, hardness, stiffness, creep? | Grades that meet the strength number but fail the governing mode |
| Manufacturing route | Thin walls, deep pockets, small internal radii, cross-drillings, hardened features | Grades that cannot be cut to that geometry economically |
| Form and availability | Bar, plate or forging, in the size required, with the certification you need | Grades that are correct on paper and unobtainable on schedule |
Nominal properties of common industrial alloys
The table below lets you compare candidate grades on the four numbers that most often decide a machined part: density, tensile strength, thermal conductivity and hardness. All values are nominal published figures for the stated condition and are given as a starting point for shortlisting, not for design. When a property is load-bearing, work from the mill certificate for the heat you actually receive.
| Alloy and condition | Density (g/cm³) | Tensile strength (MPa) | Thermal conductivity (W/m·K) | Typical hardness | Typical machined use |
|---|---|---|---|---|---|
| Aluminum 6061-T6 | 2.70 | 310 | 167 | 95 HB | Housings, brackets, general structure |
| Aluminum 7075-T6 | 2.81 | 572 | 130 | 150 HB | Highly loaded aerospace structure |
| Stainless 304 | 8.00 | 505 | 16.2 | 70 HRB | General corrosion service, fittings |
| Stainless 316L | 8.00 | 485 | 16.3 | 70 HRB | Chloride and marine service, medical |
| 17-4 PH stainless, H900 | 7.80 | 1310 | 17.9 | 40-44 HRC | Valve internals, shafts, high-strength corrosion parts |
| Alloy steel 4140, quenched and tempered | 7.85 | 655-1020 | 42.6 | 28-34 HRC | Shafts, gears, gearbox components |
| Tool steel H13, hardened | 7.80 | 1200-1700 | 28.6 | 44-54 HRC | Die casting dies, hot-work tooling |
| Titanium Ti-6Al-4V | 4.43 | 950 | 6.7 | 36 HRC | Weight-critical structure, implants |
| Nickel alloy Inconel 718, aged | 8.19 | 1240-1450 | 11.4 | 38-45 HRC | Turbine and hot-section hardware |
| Brass C360 | 8.50 | 340-470 | 115 | 60-80 HRB | High-volume turned fittings and pins |
Read the thermal conductivity column alongside the strength column, because together they predict cost. Inconel 718 and Ti-6Al-4V are both strong and both poor conductors, the combination that punishes tooling. In brass C360 and aluminum 6061-T6, heat leaves in the chip and cycle times stay short.

What makes an alloy hard to machine?
An alloy is hard to machine when heat stays at the cutting edge, when the material hardens under the tool rather than shearing away, when it chemically attacks the tool at temperature, or when it is too soft and gummy to break a chip. Hardness alone is a poor predictor: hardened H13 at 50 HRC is more tractable than annealed Inconel 718, because the nickel alloy work-hardens and holds heat.
| Material behavior | What happens at the cutting edge | What it costs you | Grades where it dominates |
|---|---|---|---|
| Low thermal conductivity | Heat concentrates in the tool rather than leaving with the chip | Reduced cutting speed, shorter tool life, high-pressure coolant required | Ti-6Al-4V, Inconel 718 |
| Work hardening | The surface hardens ahead of the tool; a rubbing pass ruins the next one | Forced heavier depth of cut, scrapped parts from dwell marks | 304 and 316L stainless, nickel alloys |
| Chemical reactivity at temperature | Tool coating and substrate degrade against the workpiece | Specific coated grades required, tighter tool change intervals | Titanium alloys |
| Gummy, ductile chip | Long stringy chips wrap the tool and mar the finish | Chip-breaking geometry, slower unattended running | Soft aluminum, low-carbon steel, copper |
| Abrasive constituents | Hard particles wear the flank mechanically | Faster predictable tool wear, more frequent offsets | Cast iron, high-silicon aluminum, some tool steels |
For a buyer, the consequence is that “difficult” alloys are not quoted higher only because the metal costs more. They are quoted higher because the machine runs slower, tooling is consumed faster, and the inspection routine deepens. Ask which of the five behaviors above drives your quote, and the number stops looking arbitrary.
Worked example: what the thermal number costs in cycle time
Spindle speed follows from cutting speed and tool diameter: n = (1000 × Vc) ÷ (π × D), with n in rev/min, Vc in m/min and D in mm. Feed follows from Vf = n × fz × z, where fz is feed per tooth in mm and z the flute count. The speeds below are illustrative; take real ones from your tooling supplier’s data.
For a Ø12mm four-flute carbide end mill at fz = 0.05mm, comparing 6061-T6 at Vc 300 m/min with Ti-6Al-4V at Vc 50 m/min:
- 6061-T6: n = (1000 × 300) ÷ (π × 12) = 300,000 ÷ 37.70 = 7,958 rev/min; Vf = 7,958 × 0.05 × 4 = 1,592 mm/min.
- Ti-6Al-4V: n = (1000 × 50) ÷ (π × 12) = 50,000 ÷ 37.70 = 1,326 rev/min; Vf = 1,326 × 0.05 × 4 = 265 mm/min.
- Ratio 1,592 ÷ 265 = 6.0. One 300mm path: 300 ÷ 1,592 = 0.19 min in aluminum, 300 ÷ 265 = 1.13 min in titanium.
The geometry did not change. The same path costs six times the spindle time because the grade will not tolerate the speed, and that factor compounds across every pass and every tool change it forces. That is why a material substitution lands on a quote as a large number with no visible cause — see also our note on tool wear by material type.
The five alloy families and what each is actually for
Aluminum alloys
Aluminum alloys are the default when the part is not temperature-limited and stiffness-to-weight matters. 6061-T6 machines quickly, welds and anodizes well, and covers most housings and brackets. 7075-T6 roughly doubles tensile strength but does not weld usefully and is more sensitive to stress-corrosion cracking, so it belongs on loaded structure rather than general hardware.
Austenitic stainless steels
304 and 316L are corrosion grades, not strength grades. 316L adds molybdenum, which is what buys chloride and marine resistance, and its low carbon content protects the weld heat-affected zone from sensitization. Both work-harden aggressively, so they need positive, committed cuts and rigid fixturing rather than the light finishing passes that instinct suggests.
Alloy and tool steels
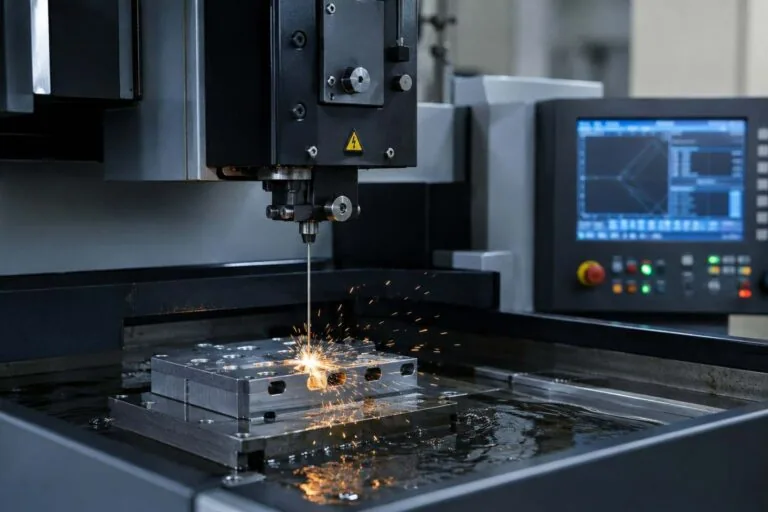
4140 is the workhorse for shafts, gears and gearbox parts, machined in the quenched and tempered condition and hardened locally where wear demands it. H13 is a hot-work tool steel used where thermal fatigue and die wear govern. Both are usually machined soft and finished hard, which puts wire and sinker EDM and grinding into the process plan.
Precipitation-hardening stainless
17-4 PH is the answer when a part needs both corrosion resistance and high strength — valve internals, pump shafts, instrument bodies. It is normally machined in the solution-treated condition and then aged, which raises hardness with modest and predictable dimensional movement. Specify the aging condition, because H900 and H1150 are different materials in service.
Titanium and nickel superalloys
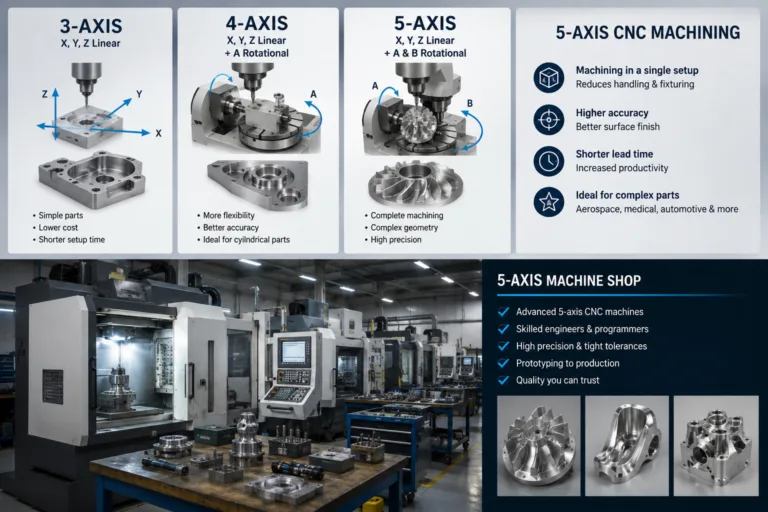
Ti-6Al-4V is chosen for strength-to-weight and biocompatibility; Inconel 718 for strength retention at temperature. Both are expensive to buy and more expensive to cut, so they earn their place only where a cheaper family fails the governing property. Where they are required, reducing setups on a 5-axis machining centre matters more than in any other family.

What tolerance and surface finish can each process hold?
Milling and turning cover the general and precision tolerance classes; EDM, grinding and honing are what you reach for when a feature is hardened, unreachable by a cutter, or must hold a critical band. MW+ holds general machining to ±0.01mm under ISO 2768-m, precision features to ±0.005mm and critical features to ±0.001mm, with surface finish from Ra 3.2µm as-machined to Ra 0.1µm polished.
| Process | Tolerance class it comfortably holds | Achievable surface finish (Ra µm) | Where it is the right tool |
|---|---|---|---|
| 3-axis and 5-axis CNC milling | ±0.01mm general, ±0.005mm precision | 3.2 as-machined, 0.4 fine-machined | Prismatic and sculpted geometry, multi-face parts |
| CNC turning and Swiss-type turning | ±0.01mm general, ±0.005mm precision | 3.2 to 0.4 | Rotational parts, long slender shafts, high-volume pins |
| Wire and sinker EDM | ±0.005mm, ±0.001mm on critical features | 0.4 and below | Hardened material, sharp internal corners, thin webs |
| Grinding and honing | ±0.001mm critical band | 0.4 to 0.1 polished | Bearing journals, sealing faces, post-hardening correction |
| Deep-hole drilling | General class on diameter, straightness governed by depth ratio | 3.2 | Cooling passages, hydraulic bores, gun-drilled features |
Two cautions. A tolerance class is achievable on a feature, not on a drawing: applying ±0.001mm globally multiplies inspection time across every dimension. And a finish number is meaningless without its parameter, defined in ISO 21920-2 (superseding ISO 4287) — Ra, Rz and Rmax are not interchangeable. See CNC turning and Swiss machining.
Should a part be machined before or after heat treatment?
Machine before heat treatment when the geometry is complex and the tolerances are ordinary, because cutting soft material is faster and cheaper. Machine after heat treatment — or finish after it — when a feature must hold a precision or critical tolerance, because hardening moves material. The usual answer is both: rough soft, heat treat, then finish the controlled features by grinding or EDM.
The step buyers most often omit is stress relief between roughing and finishing. Heavy material removal releases residual stress from the mill product, and a part that was in tolerance on the machine can walk out of it overnight. On thin-walled parts machined from plate, that operation is cheaper than the scrap it prevents.
Practical sequencing rules
- Leave grinding stock on any feature that must hold ±0.005mm or tighter through a hardening operation.
- Specify the delivered condition on the drawing, not just the grade: 17-4 PH in H900 and H1150 machine and behave differently.
- Expect subcontracted heat treatment and plating queues to sit outside the machine shop’s control, so treat them as fixed schedule, not negotiable schedule.
- Where a hardened feature is unreachable by a cutter, plan EDM into the route at quotation rather than discovering it at first article.
Material certification and traceability
A material certificate is the document that ties the metal in your part to a specific mill heat and its measured chemistry and mechanical results. It is the difference between believing a bar is 316L and being able to demonstrate it. Every MW+ order ships with a certificate of conformance, a CMM inspection report and material certificates as standard.
Name the governing material specification on the drawing and require the certificate to reference it. Most industrial grades are covered by an ASTM specification that defines chemistry, mechanical properties and permissible forms, and citing it removes the ambiguity that “316 stainless” alone leaves open. Where dimensional evidence must be defensible, the measurement chain behind it should be traceable to national standards such as those maintained by NIST.
Programme-level documentation goes further. First article inspection to AS9102 and PPAP Level 3 are available on request and quoted per program, and MW+ operates to ISO 9001:2015, AS9100D, ISO 13485, IATF 16949 and NADCAP. The inspection regime behind these documents is set out on the MW+ quality assurance page.

When the high-performance alloy is the wrong choice
The high-performance alloy is the wrong choice whenever the governing property is already satisfied by a cheaper grade, or whenever its real weakness is the one your application exposes. Upgrading a material is a habit that feels safe and is often the opposite: superalloys creep less but cost more to cut, titanium is light but galls, and 7075 is strong but cracks under sustained stress in the wrong environment.
| Situation | Why the upgrade hurts | Do this instead |
|---|---|---|
| Bracket carrying modest load at ambient temperature | Titanium multiplies machining cost for strength the part never uses | Aluminum 6061-T6, with more section if stiffness is short |
| Corrosion part with no strength requirement | 17-4 PH costs more and adds an aging operation for strength you do not need | 316L, specified against its ASTM material specification |
| Wear surface on an otherwise ordinary part | Making the whole component from tool steel prices the entire part at the wear rate | Machine the body in 4140 and harden or coat the wear surface |
| Sliding titanium-on-titanium interface | Titanium galls against itself and can seize regardless of strength | Change one side of the interface, or specify a surface treatment |
| Sustained tensile load in a humid or chloride environment | 7075-T6 is susceptible to stress-corrosion cracking in that condition | A lower-strength temper, or 6061-T6 with more section |
| Prototype for form and fit only | Cutting the production superalloy consumes budget on a part that will be scrapped | Prototype in an easier grade — see CNC prototyping — and switch for qualification |
There is also a supply argument. A common grade in a common bar size ships from stock; an exotic grade in a non-standard section becomes the critical path and stays there. MW+ machines 70+ grades, and the shortlist that includes availability beats the one that ignores it. See machine parts manufacturing.
Alloy selection: frequently asked questions
Why is my Inconel part quoted so much higher than the same geometry in stainless?
Inconel 718 combines high strength with a nominal thermal conductivity near 11.4 W/m·K, so heat stays at the cutting edge and the machine must run slower. Tool consumption rises, cycle time rises, and the inspection routine usually deepens because the risk of a scrapped part is higher. The material price is real but it is rarely the largest part of the difference.
Can I substitute 6061-T6 for 7075-T6 to reduce cost?
Only if the governing property is stiffness or corrosion rather than strength. Nominal tensile strength drops from roughly 572 MPa for 7075-T6 to about 310 MPa for 6061-T6, while stiffness is nearly identical because both are aluminum. A deflection-limited design usually tolerates the substitution; a strength-limited one does not.
What tolerance can be held on a hardened part?
On a hardened part, the controlled features are normally finished after heat treatment by grinding, honing or EDM rather than by cutting, and MW+ holds critical features to ±0.001mm by those routes. The determining factor is whether grinding stock was left before hardening; without it, a feature that moved during heat treatment cannot always be recovered.
Do I need to specify a material standard, or is the grade name enough?
Specify the standard. A grade name such as “316 stainless” leaves chemistry limits, product form and mechanical requirements open to interpretation, and different mills will supply material that is legitimately different. Naming the governing ASTM specification and the required condition on the drawing makes the material certificate checkable rather than decorative.
Why did my stainless part come back with a poor surface finish in one area?
Austenitic stainless steels such as 304 and 316L work-harden under a rubbing tool, so a pass that is too light, a worn edge, or a dwell at the end of a cut produces a hardened layer and a smeared finish. The fix is a heavier committed depth of cut, a rigid setup and a fresh edge — not a lighter finishing pass, which is the instinctive and wrong response.
How do I know whether a supplier can actually machine a superalloy?
Ask three specific questions: which grades they hold in stock, what coolant delivery the machines have, and how tool life is monitored on that grade. A supplier who machines superalloys routinely answers with detail; one who does not answers about the machine rather than the material. MW+ machines 70+ grades across 60+ machining centres — see MW+ capabilities.
Are published property tables good enough to design against?
Published values from references such as MatWeb are nominal and are appropriate for shortlisting candidate grades. They are not appropriate for a load-bearing calculation, because real heats vary within specification limits and the delivered condition matters. Design against the mill certificate for the heat supplied, and require that certificate as part of the order — as MW+ supplies with every shipment. A wider grade list, including engineering plastics, is in our CNC materials guide.
To review a grade against a drawing before committing, send the model and material requirement through MW+ contact.