Copper busbar design should connect three decisions: the electrical duty, the bolted interface and the machinable drawing. Start with the assembly owner’s current, temperature and qualification requirements. Then define the contact zones, hole pattern and inspection responsibilities. A larger overlap or a tighter machining tolerance does not, by itself, establish an acceptable electrical joint: interface condition and clamping pressure also matter. [1]
Application-guide disclosure: This is an illustrative engineering study, not a MetalWorksPlus customer case study. Every dimension, current and resistance used in the worked examples is assumed. The calculations are reproducible arithmetic, not measurements, a current rating, a fastening specification or evidence of a tested MW+ assembly.
Contents
Start with the electrical interface and its design owner
Use the following design-review approach for a solid, machined copper bar with a bolted lap connection. Keep the component drawing and the assembly specification linked by revision. The drawing should tell the machinist what to make; the assembly specification should tell the responsible team what connection must be demonstrated. This guide does not select a conductor size or prescribe an installation procedure.
Before requesting a machining quote, ask the electrical designer to identify the operating current and waveform, permissible temperature rise, ambient and enclosure conditions, mating component, insulation arrangement and applicable qualification requirements. Record which values are approved and which remain open. Avoid filling an unanswered field with a convenient catalog value from a different assembly.
Next, name the owner of each interface decision. Who releases the copper grade and temper? Who approves any coating? Who defines the fastener stack and tightening procedure? Who accepts dimensional results, and who qualifies electrical performance? A concise responsibility list is more useful than a blanket note asking the machine shop to “ensure good conductivity.”
Keep the scope visible when comparing published guidance. The Copper Development Association’s joint discussion distinguishes interface resistance from resistance associated with current spreading, and treats alternating-current effects separately. Its 2014 handbook is useful engineering background; it is not an approval document for this hypothetical connection. [1]
Define the contact faces before choosing a finish
Mark the intended mating zone on each bar. Define its boundaries from recognizable features, and distinguish that zone from cosmetic surfaces and mounting areas. Ask whether acceptance applies before coating, after coating or after final preparation. Those are drawing decisions to resolve with the assembly owner, rather than details to leave until the first inspection.
The nominal overlap is not the microscopic conducting area. The handbook explains that current crosses discrete contact locations and that surface condition and applied pressure affect interface resistance. Therefore, use overlap dimensions to describe geometry; do not relabel their product as verified electrical contact area. [1]
COMSOL’s bolted-busbar example illustrates how contact pressure can vary around a fastener and influence electrical resistance. It also models a particular AC current distribution. That example supports reviewing the interface as a coupled problem; its geometry, loading and simulation results do not establish a universal bolt pattern or MW+ performance claim. [2]
For the drawing review, ask the designer to specify the required face geometry, surface texture and permitted surface condition using the applicable drawing conventions. Define how the zone will be inspected and what condition the part must be in during inspection. Do not select a universal roughness number simply because another busbar drawing uses it.
Worked geometry: what two holes remove
Assumed layout: Consider a rectangular overlap 40 mm wide and 50 mm long on a bar 5 mm thick. Two separate, circular, through-holes have nominal diameter 9 mm. Measured from the same side and overlap end, their centers are at (10, 25) mm and (30, 25) mm. The holes therefore lie across the width at one longitudinal station. This deliberately simple layout is a geometry exercise, not a recommended fastener arrangement.
For a rectangle, area is width multiplied by length; for a circular hole, projected area is πd²/4. The following results use nominal dimensions, disregard tolerances, edge treatment and deformation, and assume both circular holes remain entirely inside the overlap. The calculations describe removed material only.
| Geometry question | Illustrative calculation | Calculated result |
|---|---|---|
| What is the gross overlap footprint? | 40 × 50 mm² | 2,000 mm² |
| What projected area do the two holes remove? | 2 × π × 9² / 4 mm² | 127.23 mm² |
| What nominal projected face area remains? | 2,000 − 127.2345 mm² | 1,872.77 mm² |
| What is the unperforated bar cross-section? | 40 × 5 mm² | 200 mm² |
| What material area remains in a transverse plane through both hole centers? | (40 − 2 × 9) × 5 mm² | 110 mm² |
The transverse section is 90 mm² smaller than the unperforated section, a 45% geometric reduction at that plane. This percentage is not a 45% reduction in ampacity, joint strength or conducting contact area. The actual electrical and mechanical response requires an applicable model and validation. Do not divide the assumed current by this section and treat the result as a sufficient joint design criterion.
Use this example to ask a better drawing question: does the selected hole layout preserve the interfaces and material paths the responsible designers intended? If holes move, recalculate the geometry and review the assembly. Changing from two holes across the width to holes at different longitudinal stations would also change which holes intersect a particular transverse section. The calculation must follow the actual coordinates, not merely the total hole count.
Worked electrical sensitivity: resistance, voltage and loss
A second example asks a different question: what would an assumed joint resistance imply for voltage drop and resistive power at a fixed DC current? For the simplified resistive model, V = IR and P = IV = I²R. OpenStax derives these relationships. [3] The example assumes a constant 200 A and evaluates three hypothetical resistance values; none is an acceptance limit or predicted property of the illustrated bar.
| Assumed current | Assumed joint resistance | Calculated voltage drop, IR | Calculated power, I²R |
|---|---|---|---|
| 200 A DC | 10 µΩ | 2.0 mV | 0.40 W |
| 200 A DC | 25 µΩ | 5.0 mV | 1.00 W |
| 200 A DC | 50 µΩ | 10.0 mV | 2.00 W |
Check the units explicitly. In the middle row, 25 µΩ is 25 × 10−6 Ω. Multiplying by 200 A gives 0.005 V, or 5 mV. Multiplying the same resistance by 200² A² gives 1 W. Under the same fixed-resistance assumption, doubling the current would multiply the calculated resistive power by four. [3]
The practical review question is what evidence will establish an acceptable resistance under the required conditions. Do not choose one of the illustrative values as a drawing limit. Ask the assembly owner to define the measurement boundary, operating conditions, allowable results and validation sequence. The machining drawing alone cannot supply those missing requirements.
Turn functional requirements into a machining drawing
Identify the material and the finished condition
Specify the approved material designation, temper, stock form and any required material documentation. State whether thickness and contact-face requirements apply to incoming stock or the finished component. If a proposed substitution is commercially attractive, send it for engineering approval rather than silently treating all copper grades or tempers as interchangeable.
For a coated component, identify the governing finish specification, controlled regions, masking boundaries and the condition in which final dimensions are accepted. Ask the coating owner to confirm how preparation and deposited layers are accounted for. This guide does not select a coating or assign an unsupported universal thickness.
Locate holes from functional references
Choose reference features that let manufacturing and inspection reconstruct the intended assembly interface. Define hole sizes, location requirements and orientation clearly. Separate clearance-hole function from locating function; do not add precision-fit requirements to every mounting hole without an assembly reason. Review the complete mating stack before accepting a nominal hole pattern.
Where a slot is proposed, document the intended adjustment direction and the accepted assembled position. Ask who checks washer support, tool access and the final contact zone. Avoid using a slot as an undocumented fix for an unresolved tolerance stack. If the part includes a formed section, identify which requirements apply after forming and which process owner controls the final interface.
Make face and edge acceptance inspectable
Identify the contact-zone boundary, relevant geometric requirements and any surface-texture callout. Define permitted edge treatment at holes and perimeter edges without allowing an unspecified chamfer to consume the controlled face. Include an acceptance method for raised edges or damage within that zone. Treat these as application-specific release questions, not universal values supplied by this article.
Review machining sequence and handling
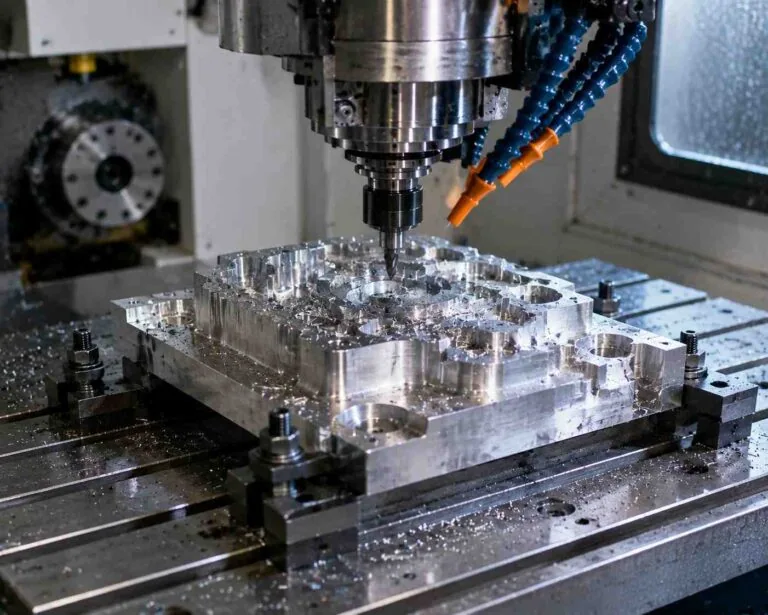
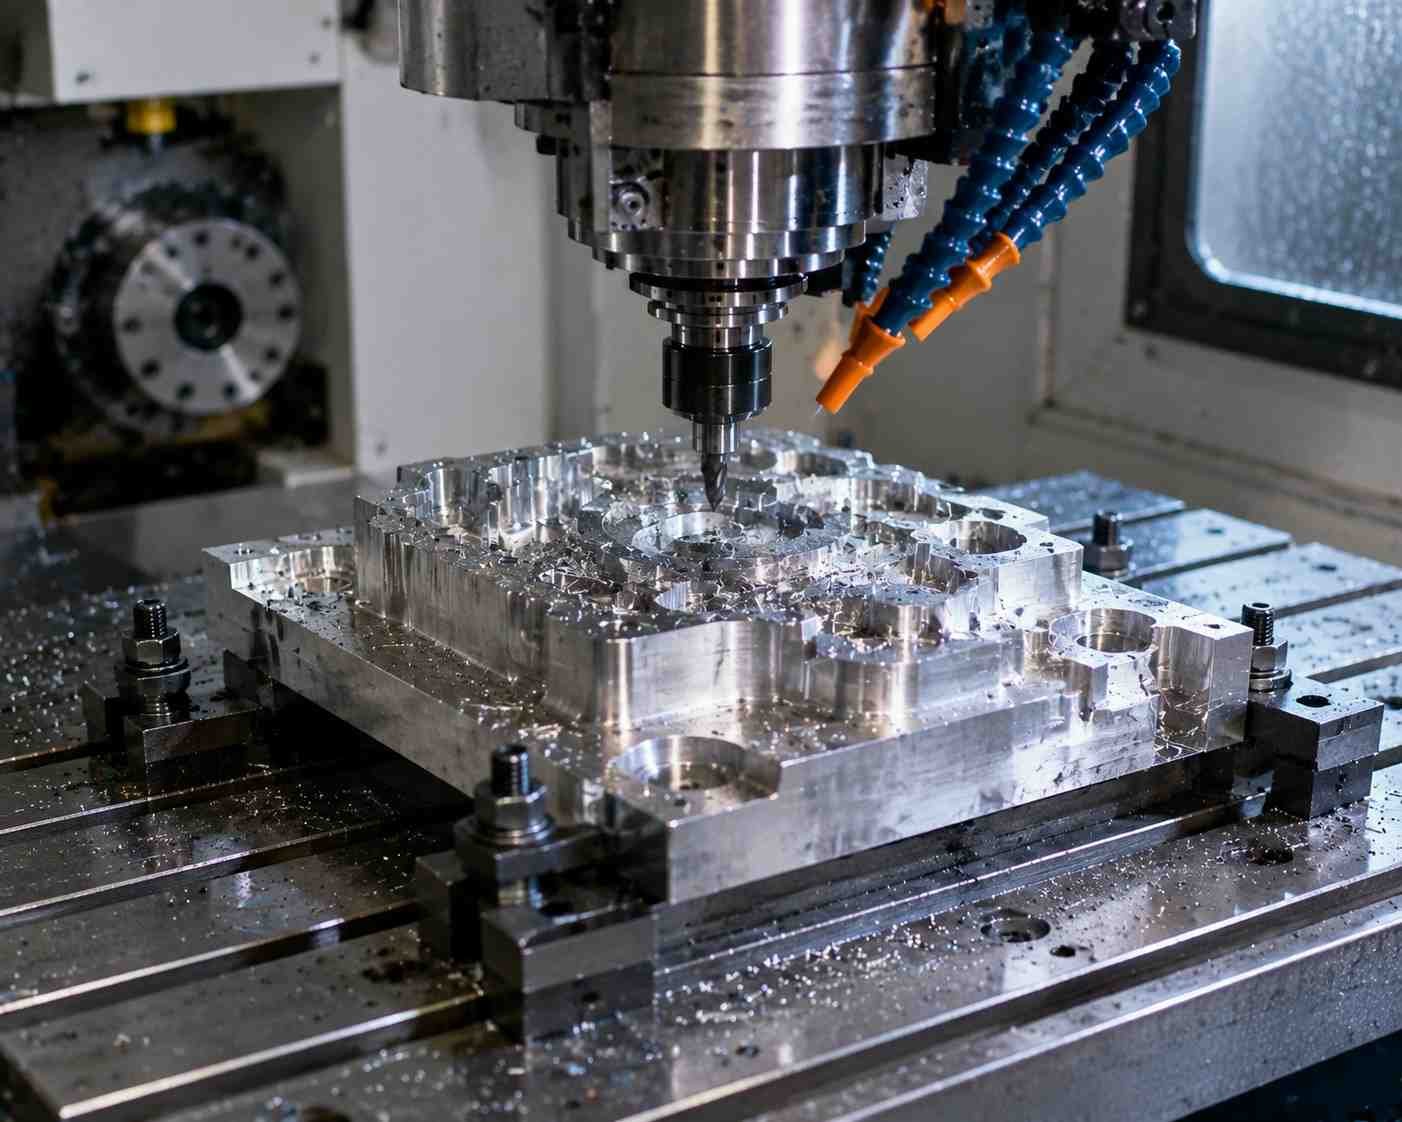
Ask the machining supplier to propose a sequence against the released drawing: blank preparation, reference establishment, contact-zone machining where required, hole production, edge finishing and final inspection. Confirm which faces support the part in each operation and whether those supports lie inside a controlled contact zone. Record any proposed change that requires design approval.
Include handling in the process discussion. Identify which surfaces require protection between machining, inspection, coating and assembly, and agree packaging that preserves the specified condition. Establish what happens if inspection finds a dent, scratch or raised edge in a controlled zone. The acceptance decision should refer to an approved requirement rather than a subjective judgment that the part looks clean.
For procurement, request a quote against a consistent package: drawing revision, model, material requirement, finish scope, inspection record and quantity. Ask suppliers to identify unresolved features and assumptions explicitly. Compare quotations using that same scope; a price comparison is not meaningful when one offer includes contact-face inspection and another assumes acceptance of stock surfaces.
Separate dimensional inspection from joint validation
Build two connected records. The component inspection record should address the released dimensions, hole pattern, controlled face geometry, specified surface condition and finish documentation. The joint-validation record should address the assembled electrical interface under the approved assembly and test plan. Record the responsible organization for each activity; this article does not claim MW+ performs electrical qualification.
For low-resistance measurements, Keysight describes a four-wire arrangement with separate current-source and voltage-sense connections. [4] Keithley explains why a two-wire measurement includes lead resistance and why sensing at the device reduces that contribution. [5] These principles support discussing a suitable measurement method with the test owner; they do not prove that a particular instrument or setup meets the required uncertainty.
As a test-plan recommendation, identify the sense locations on an assembly sketch. State whether the reported value covers only the interface or also includes defined conductor lengths. Specify the test condition, instrument capability, uncertainty treatment, acceptance criteria and record format. Preserve the assembly revision and fastening condition with the result so that later comparisons refer to the same configuration.
Keep geometric acceptance and electrical acceptance distinct in the release decision. An inspector may verify the bar dimensions without establishing joint resistance. Equally, a resistance result should not erase a dimensional nonconformance without approved engineering disposition. Use a documented review to connect the evidence to the requirement it actually addresses.
A practical release review
Before releasing the component, ask the team to answer these questions in writing:
- Interface: Are the mating component, contact-zone limits and assembly revision identified?
- Geometry: Are holes, reference features, face requirements and edge treatment inspectable?
- Material and finish: Are grade, temper, finish condition and substitution approvals resolved?
- Assembly: Has the responsible designer approved the actual fastener stack and tightening procedure? The handbook makes torque dependent on hardware and application conditions; do not copy an isolated value. [1]
- Evidence: Are component inspection and assembly qualification assigned to named owners with acceptance criteria?
- Changes: Will changes to hole position, finish or mating hardware trigger the appropriate interface review?
For the manufactured component, discuss contact faces, mounting holes and critical interfaces within MW+’s precision machined component range. Once the drawing and responsibilities are defined, use the CNC machining service review to resolve manufacturing questions. Send MetalWorksPlus the released drawing, model, material and finish requirements, plus the dimensional inspection scope. Confirm any additional validation service separately.
Copper busbar design FAQs
Does a larger overlap prove lower busbar contact resistance?
No. Nominal overlap describes geometry. The handbook identifies surface condition and applied pressure as important interface factors. [1] Require application-specific evidence rather than approving the joint from its footprint alone.
Can the two-hole calculation establish a current rating?
No. It calculates nominal projected area and one transverse material section for assumed dimensions. It does not calculate current distribution, temperature rise, contact pressure or qualification results. Use it to check the drawing geometry and identify questions for the electrical and mechanical designers.
What torque should be specified for a copper busbar joint?
Use the value and procedure approved for the actual assembly. Hardware, lubrication and operating conditions belong in that review. [1] This guide supplies no universal torque because no approved fastener stack or joint qualification has been provided.
Why discuss four-wire measurement?
A separate voltage-sense pair helps avoid including force-lead voltage drops in the measured device resistance. [4] [5] The test owner must still define sense locations, conditions, uncertainty and acceptance criteria for the actual assembly.
Is this a completed MW+ busbar project?
No. It is an application guide using clearly assumed geometry, current and resistance. No customer, manufacturing run, electrical test or performance improvement is claimed. The next step is a drawing and responsibility review for the reader’s own component.
Technical references
- Copper for Busbars: Guidance for Design and Installation (2014), Section 6. Joint resistance, surface condition and pressure; application-dependent fastener torque. Historical technical guidance, not a current product qualification.
- COMSOL: Modeling Electrical Contact Resistance at Bolted Joints. Illustrative coupled contact/electrical model; nonuniform pressure and current distribution. No model result transferred to MW+.
- OpenStax: Electrical Energy and Power. V=IR and P=IV=I²R; assumed example calculations only.
- Keysight: How to Measure Resistance Using Four-Wire Measurement. Separate force and sense leads; low-resistance measurement principle.
- Keithley/Tektronix: Two-Wire vs. Four-Wire Resistance Measurements. Lead-resistance effects, R=V/I and positioning sense leads at the device.
Sources reviewed for this guide on 24 October 2026. Engineering review questions and worked examples are original recommendations and illustrations; the references do not validate the hypothetical assembly.