A prototype exists to answer a question. If you cannot say which question it answers, you are not prototyping, you are spending money on a model. The question decides everything else: the process, the material, the tolerance you pay for, and whether you need one part or a bridge tool that makes two hundred.
This guide separates two things that get sold together and behave completely differently. CNC prototype machining validates a design in the material you intend to ship. Rapid tooling produces a working tool so you can make quantities before your production tooling exists. They serve different questions, cost differently, and fail differently.
Key takeaways
- A standard machined prototype runs 3–5 business days, with a 48-hour express route when a test rig is waiting. Volume production is a separate 10–15 business day commitment.
- Machine the prototype in the production alloy. A printed part in a substitute resin answers questions about geometry, not about strength, fatigue or corrosion.
- Do not put production tolerances on a first prototype. Use ISO 2768-m as the general class and tighten only the features whose fit you are actually testing.
- Prototyping and rapid tooling answer different questions. A prototype tells you whether the design works. A bridge tool tells you whether the design can be made repeatably, and gets you shippable quantity.
- Rapid tooling stops making sense when your design is still moving. Every change after a tool is cut is paid for twice.
- Ask what ships with the parts. A certificate of conformance, a dimensional inspection report and material certificates should be standard; first article inspection to AS9102 and PPAP Level 3 are quoted separately.
- What CNC prototype machining actually gives you
- Machining or 3D printing: which prototype do you need?
- What tolerance should a prototype be held to?
- Prototyping in the alloy you will actually ship
- How fast is a prototype, really?
- Rapid tooling: what it is and what it costs you
- Bridge tooling or production tooling: how do you decide?
- When CNC prototyping is the wrong choice
- How do you evaluate a prototyping partner?
- Frequently asked questions
What CNC prototype machining actually gives you
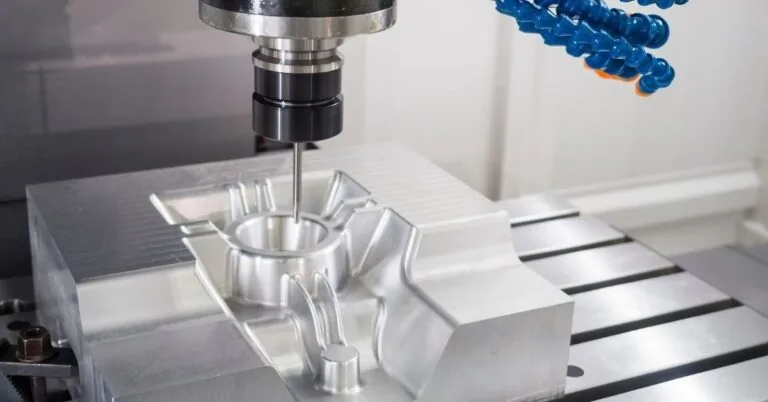
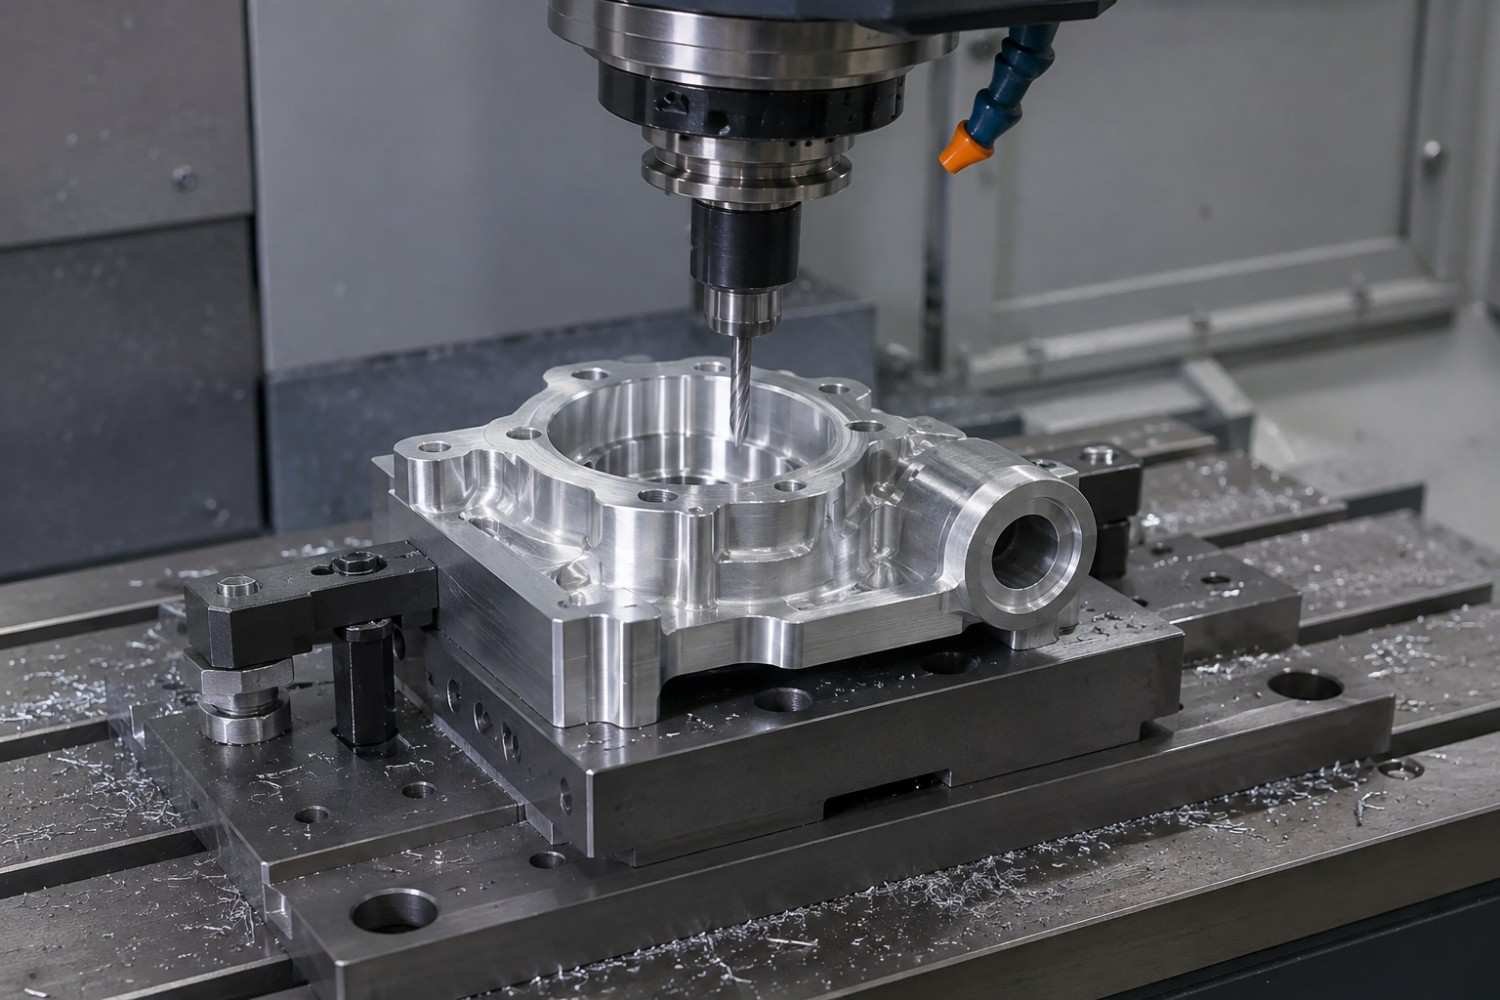
Machining removes material from solid stock, so the prototype has the grain structure, the heat treatment condition and the mechanical properties of the bar or plate it came from. That is the entire point. You are not looking at a representation of the part; you are looking at the part, made subtractively instead of at volume.
What the first article is really testing
Be explicit about the question before you order. Are you testing fit against a mating assembly, in which case the interface tolerances matter and nothing else does? Are you testing load or fatigue, in which case material condition and surface finish dominate? Or are you testing manufacturability, in which case the useful output is the supplier’s list of features that will be expensive at volume.
Why DFM feedback is the deliverable
The most valuable thing a prototype supplier returns is often not the part. It is the note saying that the 2 mm internal corner radius forces a small cutter and a slow feed, that the 12:1 deep bore will chatter, or that the datum scheme cannot be inspected as drawn. That feedback is worth more at prototype stage than at any later point, because changing a model costs nothing and changing a tool costs weeks. MW+ returns quoting and DFM notes within 24 hours; the process list sits under CNC prototyping.
Machining or 3D printing: which prototype do you need?
This is not a rivalry. They answer different questions, and a well-run programme uses both, usually in that order.
| Question you are asking | Better answer | Why |
|---|---|---|
| Does it look right, and does it fit in the hand? | Printing | Cheapest and fastest route to a shape you can hold |
| Does it assemble with the mating parts? | Either, if the interface tolerance is loose | Printed dimensional accuracy is adequate for clearance fits, not for press fits |
| Will it survive the load case? | Machining | Wrought material has properties a printed or cast substitute does not replicate |
| Will it seal, slide or wear correctly? | Machining | Surface finish and dimensional stability drive all three |
| Can I certify it for a regulated application? | Machining | Material certificates trace back to a mill heat and a published standard |
| Do I need ten of them next week? | Machining | Once programming is done, the second through tenth parts are cheap |
What tolerance should a prototype be held to?
Over-tolerancing a prototype is expensive and, worse, it hides information. If everything is held to ±0.005 mm you learn nothing about which features actually need it.
| Level | Achievable on | Use it for | Cost impact |
|---|---|---|---|
| ±0.1 mm | Standard milling, single setup | Non-functional outlines, clearance holes, first-look prototypes | Baseline |
| ±0.01 mm (ISO 2768-m class work) | Well-maintained CNC in a controlled shop | The general class on almost every prototype drawing | Small |
| ±0.005 mm | Precision milling and turning with in-process gauging | The interfaces you are specifically validating | Adds a finishing pass and inspection |
| ±0.001 mm | Grinding, honing, wire EDM, controlled metrology | Gauge surfaces and high-pressure sealing only | Substantial; one feature at a time |
| Geometric callouts | Fixturing built around your datums | Anything whose repeat assembly you are testing | Often cheaper than the equivalent ± stack |
Put a general class on the drawing under ISO 2768 so unmarked dimensions are defined, and express the features that matter geometrically under ISO 1101 or ASME Y14.5. Where a shaft meets a bore, call the fit class from ISO 286 instead of dimensioning both halves separately. Specify surface roughness to ISO 4287 on faces that seal or slide, and leave everything else as-machined at Ra 3.2 µm.
One prototype held to a tolerance proves the shop can do it once. Cpk ≥1.67 on a critical characteristic is what predicts the hundredth part, and it is the number to ask about when the prototype becomes a production intent.
Prototyping in the alloy you will actually ship
Values below are published nominal figures, useful for shortlisting. Where a property carries load in your design, work from the mill certificate for the heat you were shipped rather than a handbook number.
| Material | Density (g/cm³) | Nominal tensile strength (MPa) | Why prototype in it |
|---|---|---|---|
| Aluminium 6061-T6 | 2.70 | ~310 | Fast and cheap to cut; the default first-iteration alloy |
| Aluminium 7075-T6 | 2.81 | ~570 | When 6061 is not strong enough and weight still matters |
| Stainless 303 | 8.00 | ~620 | Free-machining; good for turned prototype hardware |
| Stainless 316L | 8.00 | ~485 | Corrosion and biocompatibility testing |
| Titanium Ti-6Al-4V | 4.43 | ~950 | Strength-to-weight and implant work; slow and costly to cut |
| PEEK | 1.30 | ~100 | Chemical resistance, insulation, sterilisable components |
Compare grades on MatWeb, then name the stock on the drawing against a published ASTM designation — B211 for aluminium bar, A276 for stainless bar, B348 for titanium bar — and require the certificate with the parts. A prototype validated on an unknown grade has validated nothing you can rely on later. MW+ processes 70+ material grades, so the shortlist is rarely limited by what is available.
How fast is a prototype, really?
| Phase | Standard | Expedited | What drives variance |
|---|---|---|---|
| Quote and DFM review | Within 24 hours | Same day | Missing tolerances, no material callout, model and drawing disagreeing |
| Machined prototype | 3–5 business days | 48-hour express | Stock availability; number of setups |
| Finishing and heat treatment | Adds days | Sometimes parallelised | Outside processes are the usual delay, not the cutting |
| Volume production | 10–15 business days | Quoted per programme | Quantity, fixturing, outside processes |
| FAI or PPAP documentation | On request | — | Adds calendar time; quote it with the parts, not after |
The realistic bottleneck on a fast prototype is almost never the machine. It is a drawing that needs a question answered, a material that has to be ordered, or an anodising line with a queue. Send a complete package — STEP or IGES model, dimensioned drawing, material and standard, finish, quantity, required date — and the express route becomes usable rather than theoretical.
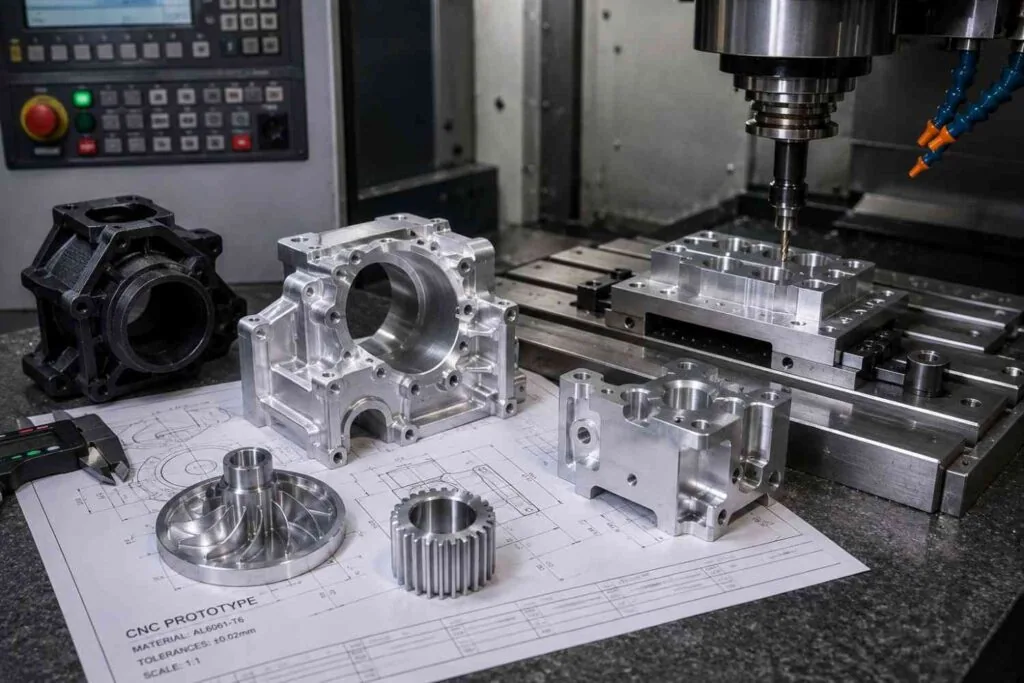
Rapid tooling: what it is and what it costs you
Rapid tooling is a different purchase from prototyping. You are no longer buying a part; you are buying a machined tool — a mould, a die, a jig or a fixture — that produces parts. The tool is made faster and cheaper than a production tool by accepting a shorter life and a narrower process window.
Where the savings come from, and what they cost
Three levers make a tool fast. Softer tool material, typically aluminium instead of hardened steel, cuts machining time substantially but reduces the number of shots the tool will survive. Simplified tool architecture — fewer slides, hand-loaded inserts instead of automatic actions — removes weeks of build. And looser tolerance on non-critical tool surfaces means fewer finishing operations.
Each lever has a price. A softer tool wears, so the last parts off it are not identical to the first. Hand-loaded actions slow the cycle and add operator variability. If your programme is about proving repeatability rather than just getting quantity, be explicit about that, because it changes which corners can be cut.
Fixtures are the underrated case
Not all tooling makes parts. Machining fixtures, inspection gauges and assembly jigs are usually the cheapest tooling you will ever commission and the most reliable way to hold a tolerance repeatably. A well-designed fixture that locates on your drawing datums removes a class of variation that no amount of machine capability compensates for. Fixture work runs through the same CNC machining services as the parts themselves.
Bridge tooling or production tooling: how do you decide?
The decision is a function of three things: how many parts you need before production tooling exists, how settled the design is, and how much repeatability you have to prove.
| Situation | Recommendation | Why |
|---|---|---|
| Under about 50 parts, design still moving | Machine them directly | No tool to obsolete when the next revision lands; with no minimum order quantity you can order what you need |
| Hundreds of parts needed before production tooling is ready | Bridge tooling | Amortises across enough parts to beat unit machining cost, and protects the launch date |
| Design frozen, volume confirmed, multi-year programme | Production tooling | Hardened steel tools hold tolerance across the life you actually need |
| You must prove process capability to a customer | Production-intent tooling and PPAP | Capability data from a soft tool does not transfer to a hard one |
| Geometry is complex but volume stays low | Keep machining | 5-axis work on multi-axis machining centres often beats tooling economics below a few thousand parts |
When CNC prototyping is the wrong choice
A supplier who never tells you the process is wrong will sell you the wrong process cheerfully. Here is where machined prototyping loses.
| Your situation | Better answer | Why |
|---|---|---|
| You need to check ergonomics or proportion on a shape that will change tomorrow | 3D printing | Cheaper per iteration, and the material is irrelevant to the question |
| The part has internal channels no cutter can reach | Additive, then machine the critical faces | Conformal cooling and internal lattices are not accessible to a tool |
| You need thin-walled, high-volume geometry and know it | Go straight to tooling with a casting or moulding trial | A machined version of a moulded part validates geometry but not the moulding process |
| The design is not settled and you order a bridge tool anyway | Wait, and machine the interim parts | Every revision after a tool is cut is paid for twice |
| Features are finer than a cutter can produce | Micro-machining or wire EDM | Standard milling has a practical floor set by tool diameter and deflection |
| You need one part from stock you already hold, today | Manual machining | Programming and setup overhead can exceed the cut time on a single piece |
How do you evaluate a prototyping partner?
| What to ask | A good answer sounds like | Red flag |
|---|---|---|
| Will you review my model before quoting? | Written DFM notes naming specific features and risks | A price by return with no questions |
| What ships with the parts? | Certificate of conformance, CMM inspection report, material certificates | “Documentation is available on request” |
| Can the same shop take this to production? | Yes, with the programme and fixture archived against the part number | Prototype-only shop with no volume path |
| How is metrology calibrated? | Scheduled calibration with a traceable chain and records | No interval named |
| Which certifications, to what registered scope? | Named standards, certificate numbers, the scope statement | Logos with no certificate offered |
| What is the real express lead time? | A named route with its conditions stated | “As fast as you need” |
Read the scope statement, not the logo. ISO 9001:2015 is the baseline quality management system; AS9100D adds aerospace configuration management and counterfeit-part control; ISO 13485 governs medical device quality systems; IATF 16949 covers automotive supply. MW+ holds all four, operating from a 15,000 m² facility in GuangMing District, Shenzhen with 120+ engineers and machinists serving customers in 50+ countries.
Ask what the CMM is calibrated against; the chain should terminate at a national metrology institute, which is what NIST traceability means in practice. Every MW+ order ships with a certificate of conformance, a CMM inspection report and material certificates, with first article inspection to AS9102 and PPAP Level 3 available on request and quoted per programme. The inspection workflow is set out on the quality assurance page.
Frequently asked questions
Why is my second prototype cheaper than the first?
Because the first one paid for programming, fixturing and the first-off inspection. Those are one-time costs against the part number, not against each piece. That is also why ordering three prototypes instead of one rarely triples the price, and why it is usually worth ordering a spare for destructive testing while the setup is still on the machine.
Can I go straight from prototype to production with the same supplier?
You should want to. The value is in what carries over: the programme, the fixture, the inspection plan and the accumulated knowledge of which features are fragile. Ask specifically whether these are archived against your part number and whether the same quality system applies to both, because a prototype shop that hands you off to a different production supplier discards all of it.
Is rapid tooling actually cheaper than machining the parts?
Only above a crossover quantity, and the crossover moves with geometry. A simple part machined in a single setup stays cheap for a long time, so tooling may not pay back until well into the thousands. A complex part with many setups reaches the crossover much sooner. Ask your supplier to price both at your real quantity rather than assuming tooling wins.
What happens if my design changes after the tool is cut?
It depends entirely on the direction of the change. Removing material from the part means adding material to the tool, which is a weld-and-remachine job or a new insert. Adding material to the part means removing it from the tool, which is often straightforward. Discuss the likely direction of your remaining changes before the tool is designed; it can be built to accommodate them.
Do I need to send a drawing if I have a 3D model?
Yes. The model carries geometry; the drawing carries intent. Tolerances, datums, surface finish, material standard, heat treatment condition and which dimensions are critical are all invisible in a STEP file. Accepted formats are STEP, IGES, DXF, DWG, SolidWorks and PDF, and sending the model without the drawing guarantees the supplier will guess at exactly the things you care about.
How many prototypes should I order?
More than one, almost always. One part gives you no information about variation and no spare when a test destroys it. Three is a practical minimum for anything you intend to load-test: one for inspection, one for fit, one to break. Since there is no minimum order quantity, the constraint is your budget rather than the supplier’s policy.
Will a prototype tell me what production will cost?
Not directly, and treating the prototype price as a volume indicator is a common budgeting error. Prototype pricing carries the full setup on very few parts. Ask for a volume quote at your target quantity alongside the prototype quote, and ask which features are driving that number, because those are the ones worth redesigning while it is still free.
How do I get a prototype quoted quickly?
Send a complete package in one message: 3D model, dimensioned drawing, material with its standard, finish, quantity and the date you need parts in hand. Say what the part does and which feature you are validating, because that lets a supplier propose a cheaper route that still answers your question. Send it through contact us for a quote with DFM notes within 24 hours; tight-tolerance production examples are shown under CNC precision parts.