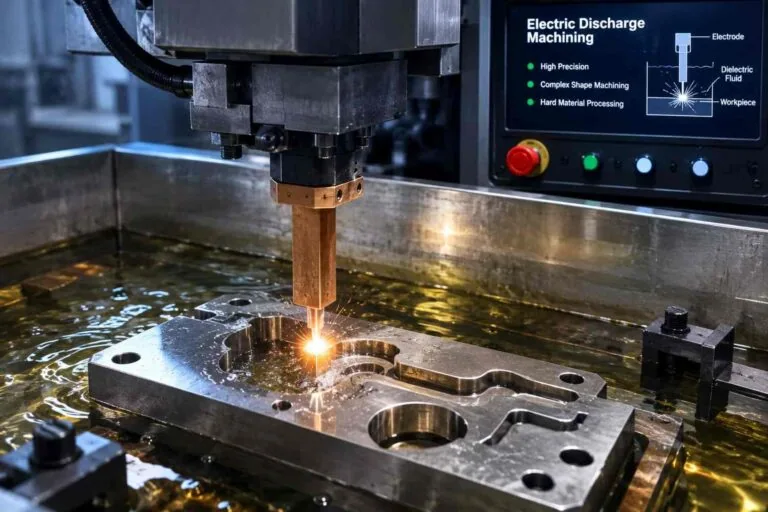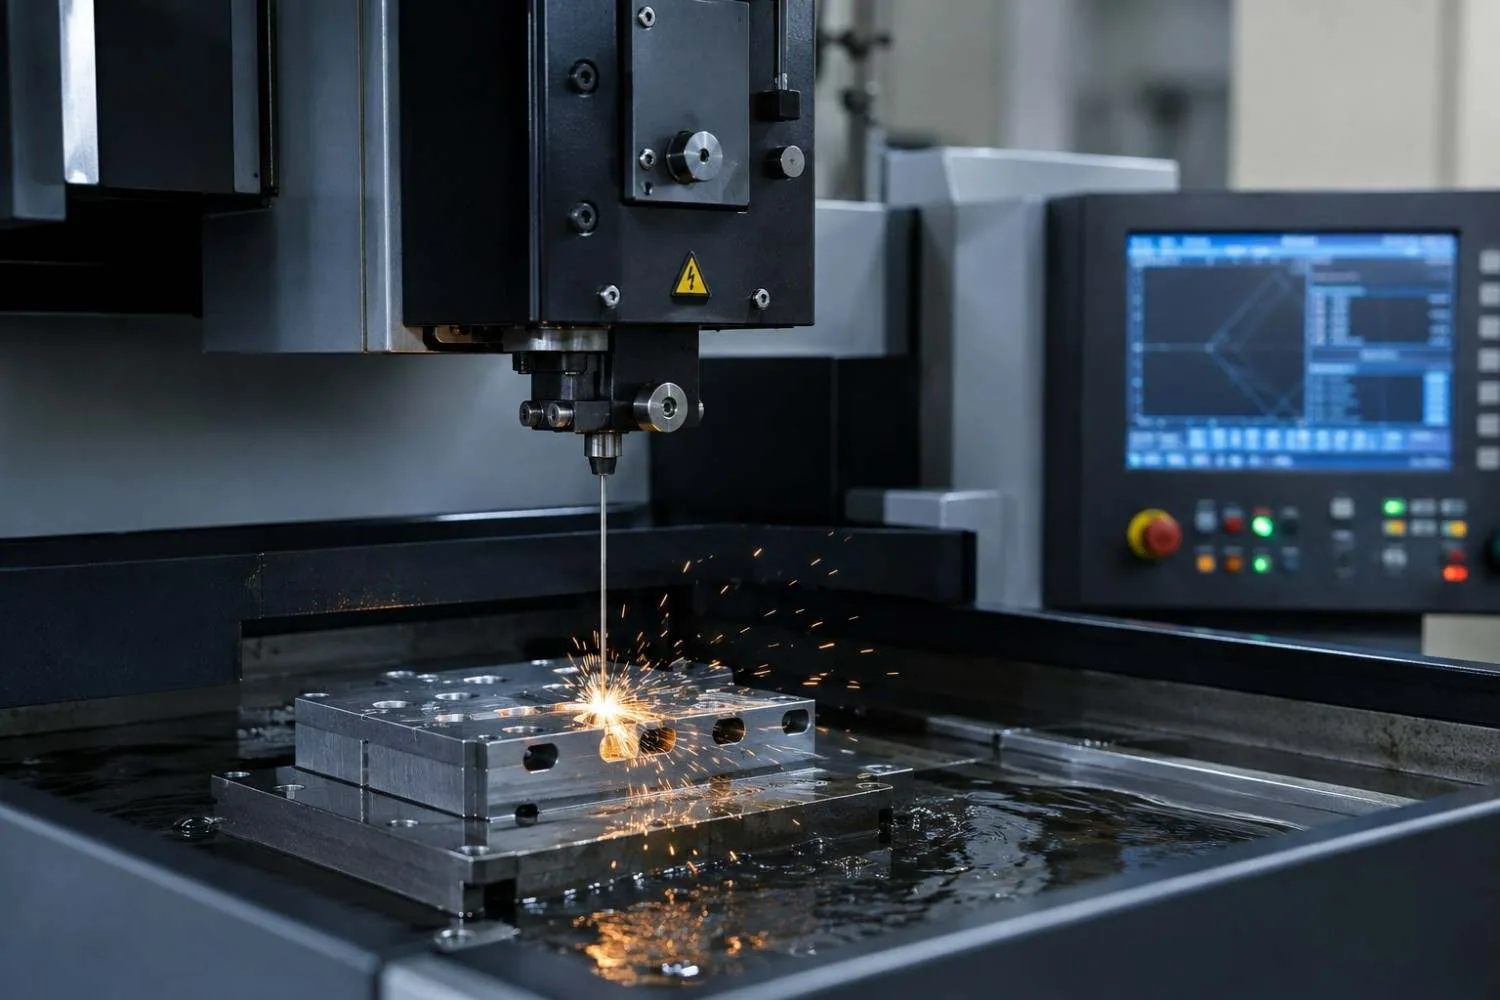
Wire EDM cuts by eroding metal with controlled electrical sparks rather than by pushing a tool through it. Because there is no cutting force, hardness stops being a constraint and geometry that would snap an end mill becomes routine. It is also slow, leaves a modified surface layer, and cannot cut anything that does not conduct electricity. This page covers how wire EDM works, what it holds, what it costs, how to specify it, and when to use something else.
Key takeaways
- Wire EDM works only on electrically conductive material. Hardness is irrelevant, so 62 HRC tool steel and tungsten carbide cut as readily as annealed stock.
- The smallest internal corner radius equals the wire radius plus the spark gap. With a 0.25 mm wire that is roughly 0.15 mm; finer wire gets tighter and cuts slower.
- MW+ holds ±0.005 mm on wire EDM work and ±0.001 mm on selected features, with general tolerances to ISO 2768-m.
- Cost is driven by cut height multiplied by path length, and by the number of skim passes. Each skim pass improves finish and accuracy and adds machine time.
- Wire EDM is the wrong process for open pockets, non-conductive materials, large stock removal and anything a mill can reach in one pass.
- How does wire EDM actually cut?
- What tolerance and finish can wire EDM hold?
- Which materials can be wire cut?
- What drives the cost of a wire EDM part?
- When is wire EDM the wrong process?
- Wire EDM against the alternatives
- How do you specify a wire EDM part?
- How MW+ runs wire EDM work
- Frequently asked questions
- What to send us
How wire EDM works: the spark, the wire and the cut
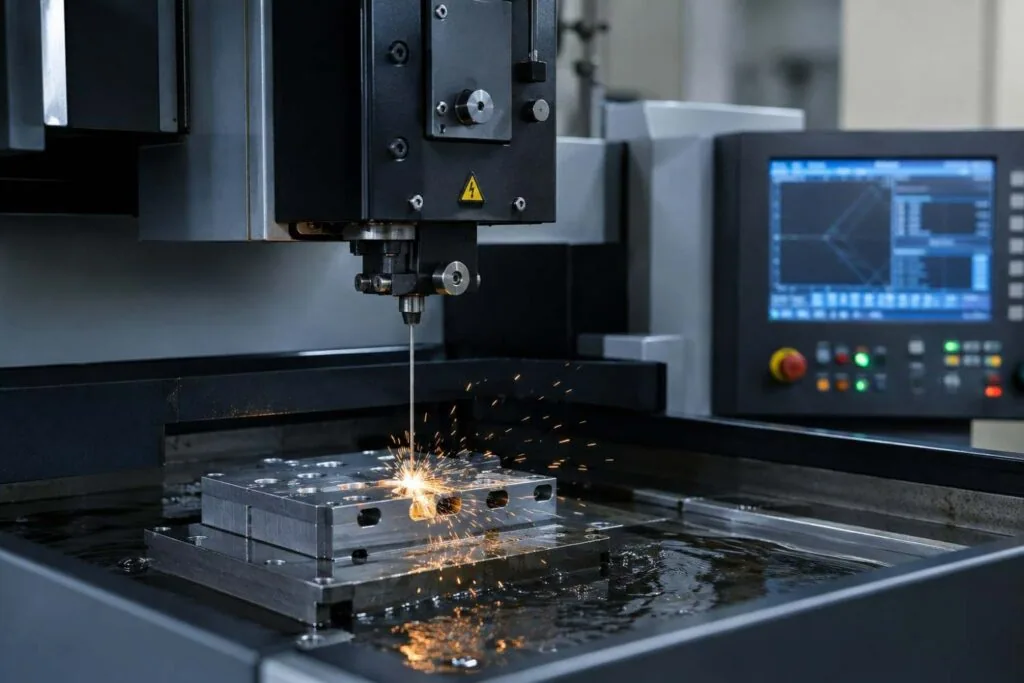
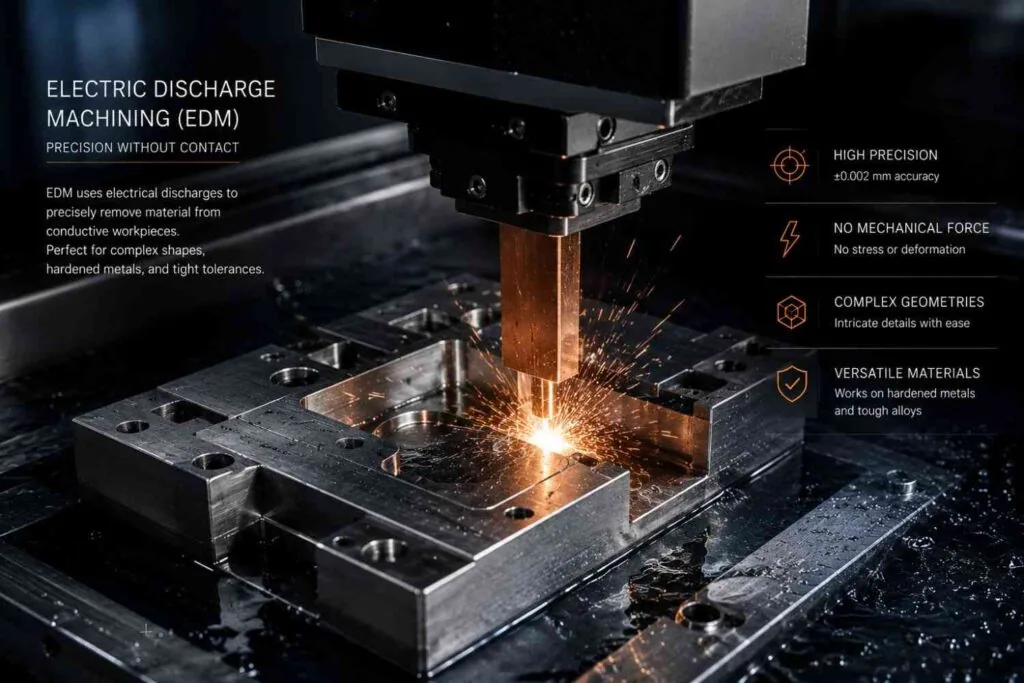
A thin wire, typically 0.02 to 0.3 mm in diameter, unspools continuously between an upper and a lower guide. The workpiece is submerged in deionised water. A voltage is applied across the tiny gap between wire and workpiece, and when the gap breaks down, a spark jumps and vaporises a microscopic crater of metal. Repeat that tens of thousands of times a second while the table moves, and you have a cut.
The wire never touches the part
There is always a spark gap, usually a few hundredths of a millimetre, between the wire and the material. Nothing presses on the workpiece, so there is no deflection, no chatter and no clamping distortion of a thin section. This is the whole reason wire EDM exists: it machines shapes that would fail mechanically under any cutting tool.
The dielectric does more than cool
Deionised water insulates the gap until the voltage is high enough to break it down, then flushes the eroded debris away. Flushing quality is what separates a clean cut from a wire break. Tall parts, blind slots and interrupted cuts all make flushing harder, which is why cut height affects both speed and reliability.
Rough cut, then skim passes
The first pass removes the bulk at high pulse energy and leaves a relatively coarse surface. Each subsequent skim pass runs at lower energy along an offset path, taking off a few microns and improving both accuracy and finish. Skim passes are the main lever on a wire EDM quote: one rough cut is fast and adequate for a fixture plate, four passes are slow and appropriate for a die.
What tolerance and finish can wire EDM hold?
The honest answer depends on how many passes you are willing to pay for, how tall the part is, and how well the material behaves when internal stress is released. Here is the working ladder.
| Level | Typical passes | Surface finish | Typical use | Cost impact |
|---|---|---|---|---|
| ±0.01 mm, ISO 2768-m | One rough cut | Around Ra 3.2 µm | Fixture plates, spacers, blanks | Baseline |
| ±0.005 mm | Rough plus two skims | Ra 0.4 µm | Punches, gauges, medical components | Roughly double the machine time |
| ±0.001 mm on selected features | Rough plus three or four skims | Ra 0.1 µm | Die inserts, optical seats, press fits | Quoted per feature, not per part |
Surface roughness parameters are defined in ISO 4287, and Ra alone is not always the right callout. An EDM surface has a distinctive random texture with no directional lay, which is often better for a sealing face than a ground surface of the same Ra value. If the function depends on it, state the parameter you actually need rather than defaulting to Ra.
Two limits are worth knowing before you draw the part. Internal corners cannot be sharper than the wire radius plus the spark gap, which is around 0.15 mm with a common 0.25 mm wire. Taper cuts are possible to roughly ±30 degrees on a modern machine, but taper accuracy degrades as the angle increases and as the part gets taller.
Which materials can be wire cut?
Any material that conducts electricity, and only those. Hardness is irrelevant to the process, which is why wire EDM is the default route for hardened tool steel and carbide. What does vary between materials is cutting speed and how the part behaves when residual stress is released.
| Material | Cuts well? | What to watch |
|---|---|---|
| Hardened tool steel, D2 and A2 up to 62 HRC | Yes, the classic application | Stress release can move the part; rough cut before final heat treat where possible |
| Tungsten carbide | Yes | Cobalt binder can be leached at the cut edge; specify skim passes |
| Stainless 304, 316, 17-4 PH | Yes | Good general behaviour; recast layer matters for implantable work |
| Titanium Ti-6Al-4V | Yes | Slower than steel; flush quality is critical on tall sections |
| Inconel and other nickel alloys | Yes | Slow, and cost scales directly with cut height |
| Aluminum | Yes, fast | Often cheaper to mill unless the geometry demands EDM |
| Ceramics, plastics, composites | No | Not conductive. Use laser, waterjet or milling |
Published values for hardness, conductivity and thermal properties are nominal. MatWeb is a reasonable first reference, and grade definitions come from ASTM or the equivalent AMS specification, but when a property is load-bearing you should work from the mill certificate for the lot actually supplied. Every order we ship includes material certificates for that reason.
What drives the cost of a wire EDM part?
Wire EDM is priced on machine hours, and machine hours are governed by how much material the spark has to remove. That is the cut height multiplied by the length of the path, multiplied again by the number of passes.
| Driver | Effect on price | What you can do about it |
|---|---|---|
| Cut height (stock thickness) | Directly proportional | Stack parts and cut several at once where tolerance allows |
| Path length | Directly proportional | Remove decorative detail that serves no function |
| Number of skim passes | Each pass adds roughly a third to the cut time | Specify tight finish only where it is needed |
| Corner radius | Finer wire is slower and breaks more often | Open the radius to 0.2 mm where function allows |
| Start holes | Each internal cut needs one drilled first | Consolidate internal features; ask about open-sided cuts |
| Material | Nickel alloys and carbide cut slowly | Confirm the grade genuinely needs to be that material |
The most common saving we find in a design review is stacking. If your part is 3 mm thick and the tolerance permits it, cutting ten parts in one stack costs roughly what one 30 mm part costs, not ten times a 3 mm part. Tell us the quantity when you send the drawing and we will tell you whether stacking is viable.
When is wire EDM the wrong process?
Wire EDM is frequently specified for parts that a mill would produce faster and cheaper. Here is where we would route you elsewhere, including away from EDM entirely.
| If your part… | Use this instead | Why |
|---|---|---|
| Has open pockets with a floor | CNC milling | The wire cuts right through; it cannot leave a floor |
| Is a non-conductive material | Laser, waterjet or milling | No conduction, no spark, no cut |
| Needs large volumes of stock removed | Milling, then EDM the critical features | Spark erosion is slow per cubic millimetre |
| Is a simple 2D profile in thin soft sheet | Laser cutting or stamping | Orders of magnitude faster at the same tolerance |
| Is a blind cavity or 3D form | Sinker EDM | A through-cutting wire cannot make a blind form |
| Is slender, turned and made in thousands | Swiss machining | Cycle time is a fraction of the EDM equivalent |
There is one more caveat that matters in regulated work. Spark erosion leaves a thin recast layer, metal that melted and re-solidified, often with a heat-affected zone beneath it. On most parts it is irrelevant. On fatigue-critical aerospace components and implantable devices it is not, and it must be removed by skim passes, polishing or etching. If your specification limits recast depth, say so on the drawing; it changes the process plan and the price.
Wire EDM against the alternatives
Most parts can be made several ways. The question is which process gets you the feature you actually care about at the lowest total cost.
| Process | Typical tolerance | Handles hardened stock | Best at | Weakness |
|---|---|---|---|---|
| Wire EDM | ±0.005 mm | Yes | Sharp internal corners, tall profiles, fragile sections | Slow; through-cuts only; conductive materials only |
| Sinker EDM | ±0.005 mm | Yes | Blind cavities, 3D forms, deep ribs | Needs a bespoke electrode for each form |
| CNC milling | ±0.005 to ±0.01 mm | Poorly | Bulk removal, pockets, 3D surfaces | Corner radius limited by cutter; tool deflection |
| Laser cutting | ±0.05 mm | Yes | Fast 2D profiles in sheet | Heat-affected edge; thickness limited |
| Waterjet | ±0.1 mm | Yes | Thick stock, any material, no heat | Taper and a rougher edge |
In practice the two often combine. Mill the bulk of the part, heat treat it, then wire cut the features that must stay accurate after hardening. Our electric discharge machining cells sit alongside the milling and turning lines for exactly that reason.
How do you specify a wire EDM part?
Four things on a drawing decide whether a wire EDM quote comes back fast and firm or slow and hedged.
Give the internal corners a real radius
A drawing that shows a perfectly sharp internal corner is not manufacturable by wire EDM or anything else. State the maximum radius you can tolerate. If 0.2 mm is acceptable, a standard 0.25 mm wire cuts it quickly. If you genuinely need 0.05 mm, that means fine wire, slower feed and more wire breaks, and the price should reflect it.
Declare datums and mark the critical dimensions
Reference the geometry to a datum frame per ISO 1101 or ASME Y14.5. Then put a general tolerance block on the drawing, typically ISO 2768-m, and call out only the handful of features that need ±0.005 mm or tighter. Tightening everything is the most reliable way to double a wire EDM quote for no functional gain.
Say where the tab can go
A profile cut from a plate has to be held until the cut finishes, so a small tab is left and removed afterwards, leaving a witness mark. On automated machines the slug can sometimes be caught instead. Tell us which faces are cosmetic or functional and we will place the tab somewhere harmless rather than guessing.
State the heat treatment sequence
Hardening moves parts. Cutting before heat treatment risks distortion; cutting after it means the wire is doing all the work at hardened speed. For most tool steel components the right answer is rough machining, heat treat, then wire cut the accurate features. Tell us the intended sequence, or ask and we will recommend one.
How MW+ runs wire EDM work
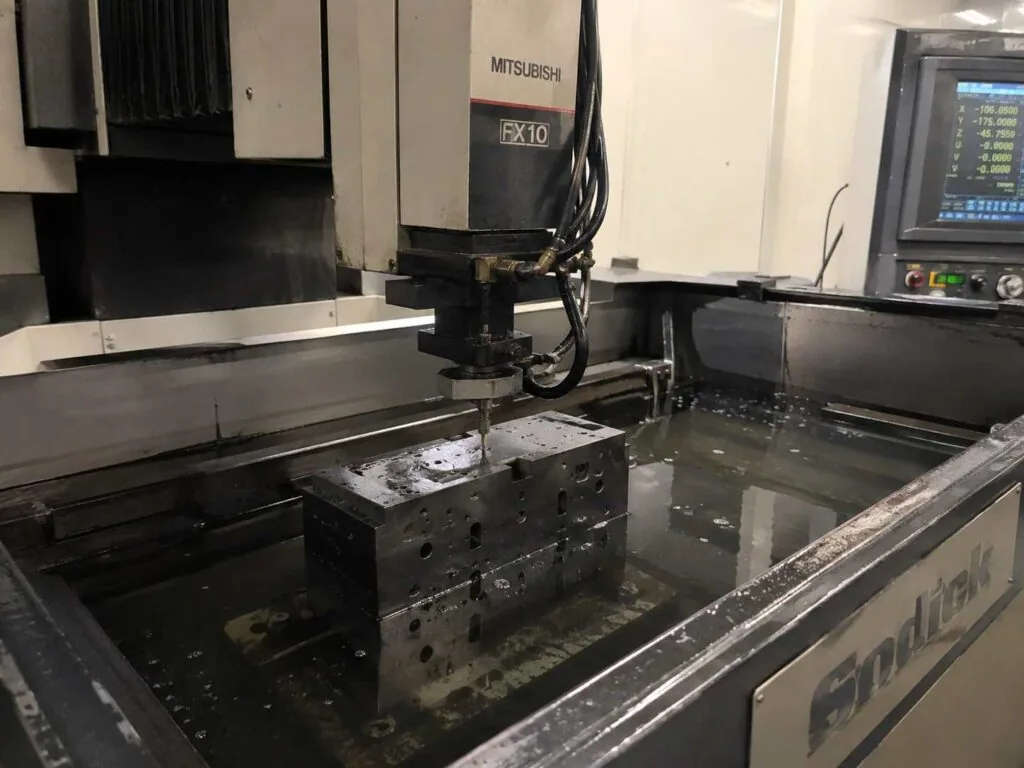
MW+ (MetalWorks Plus) was founded in 2015 and operates a 15,000 m² facility in GuangMing District, Shenzhen, with 60+ machining centres and 120+ engineers and machinists. The EDM cells run Sodick wire machines with automatic wire threading and adaptive servo control, in a temperature-controlled workshop, alongside sinker EDM and small-hole drilling for blind forms and high-aspect-ratio holes.
Certifications are ISO 9001:2015, AS9100D, ISO 13485, IATF 16949 and NADCAP. Process capability is held at Cpk ≥1.67 on controlled characteristics, and dimensional reports come from a CMM whose calibration chain is traceable in the sense NIST defines. Every order ships with a certificate of conformance, a CMM inspection report and material certificates; first article inspection to AS9102 and PPAP Level 3 are available on request and quoted per programme.
| Phase | What happens | What you get |
|---|---|---|
| DFM review | Geometry checked for corner radii, start holes, tab placement and stacking | Written feedback with the quote, within 24 hours |
| Programming | Path, offsets and pass count set for the specified tolerance | Confirmation of achievable tolerance per feature |
| Rough cut | Bulk removal at high pulse energy | Profile established, stock still oversize |
| Skim passes | Two to four low-energy offset passes as specified | ±0.005 mm and Ra 0.4 µm, finer on request |
| Inspection | CMM verification of critical dimensions | COC, dimensional report, material certificates |
| Delivery | Prototype or production release | 3–5 business days on prototypes, 48-hour express available; 10–15 business days on volume, no minimum order quantity |
Where a part needs both processes, the same facility handles CNC machining, micro-machining and finishing, so a component does not travel between vendors between operations. Inspection standards are set out on our quality assurance page.
Frequently asked questions
Why is my wire EDM quote so much higher than the milled version?
Because spark erosion removes material far more slowly than a cutter does, and you are paying for machine hours. If the part could be milled and you specified EDM for a feature that does not need it, ask for both routes to be quoted. Where EDM genuinely wins is hardened material, sharp internal corners, tall thin sections and parts that would distort under cutting force. If none of those apply to your part, you are probably buying the wrong process.
What is the smallest internal corner radius you can cut?
The minimum equals half the wire diameter plus the spark gap. With a standard 0.25 mm wire that lands near 0.15 mm. Finer wire down to 0.02 mm gets tighter still, but it cuts more slowly, breaks more often and cannot handle tall sections. Tell us the largest radius your design can accept rather than the smallest we can produce; it usually saves real money.
Does the recast layer matter for my part?
For most industrial components, no. For fatigue-critical aerospace parts, implantable medical devices and anything with a fracture-mechanics case behind it, yes. Recast is metal that melted and re-solidified during the spark, with a heat-affected zone below it. Skim passes reduce it substantially, and polishing or chemical etching removes it. If your specification sets a limit, state it on the drawing so it is planned in rather than discovered late.
Can you cut a blind pocket with wire EDM?
No. The wire passes through the workpiece from one side to the other, so every wire EDM feature is a through-cut. Blind cavities, 3D forms and deep ribs need sinker EDM, which uses a shaped graphite or copper electrode burned into the surface, or conventional milling if the material is soft enough. We run both, so send the model and we will tell you which is appropriate.
Should I harden the part before or after wire cutting?
Usually after rough machining and before wire cutting. Heat treatment distorts parts, so any feature cut before hardening may move out of tolerance. Wire EDM does not care about hardness, which is exactly what makes it the right finishing process for hardened tool steel. Rough mill, heat treat, then wire cut the features that must be accurate on the finished part.
What documentation ships with wire EDM parts?
Every order includes a certificate of conformance, a CMM inspection report covering the critical dimensions, and material certificates for the lot supplied. Full first article inspection to AS9102 and PPAP Level 3 submissions are available on request and quoted per programme, because both consume real engineering hours and should be priced openly rather than assumed.
Is there a minimum order quantity for EDM work?
No, and single pieces are common in this process because die inserts and punches are made one at a time. Be aware that programming and setup are largely fixed, so quantity one carries all of it. If you expect repeats, say so at quote stage and ask for pricing at two quantities so you can see how the fixed cost amortises across a batch.
What to send us
A STEP file, a dimensioned drawing with datums declared and internal corner radii stated, the material and its condition, the stock thickness, the quantity, and a note of which dimensions are genuinely critical. That is enough for a quote and written DFM feedback within 24 hours, including whether stacking will cut your unit price and whether the tolerance you asked for is one we can hold.
If you are not sure EDM is the right process, send the part anyway and say so. We would rather quote it on the cheaper route and keep the work than sell you machine hours you do not need.