In metal surface finishing, a callout that reads “black anodize” is not a specification. It does not say which anodize, how thick, whether the thickness is per surface or per diameter, what corrosion performance is required, or which surfaces must stay bare. Every one of those gaps is filled in by someone else, usually by the cheapest interpretation, and the part that comes back is defensible and wrong.
This guide is for the engineer writing the finish line on a drawing for an end-use component. It compares the main processes, explains what each one does to the part’s dimensions, sets out what a complete callout contains, and states where a coating is the wrong answer entirely. For the machining side of the same part, see MW+ CNC machining services.
Key takeaways
- Anodizing grows into the part as well as outward, so roughly half the coating thickness is consumed from the original surface. On a close-fitting bore, that is a tolerance change, not a cosmetic one.
- Corrosion performance is a test result, not an adjective. State a required salt-spray duration against ASTM B117 rather than asking for a coating that is “corrosion resistant”.
- Passivation of stainless steel is a cleaning and chemical treatment, not a coating, and adds no measurable thickness. Specify it against ASTM A967/A967M, naming nitric or citric acid.
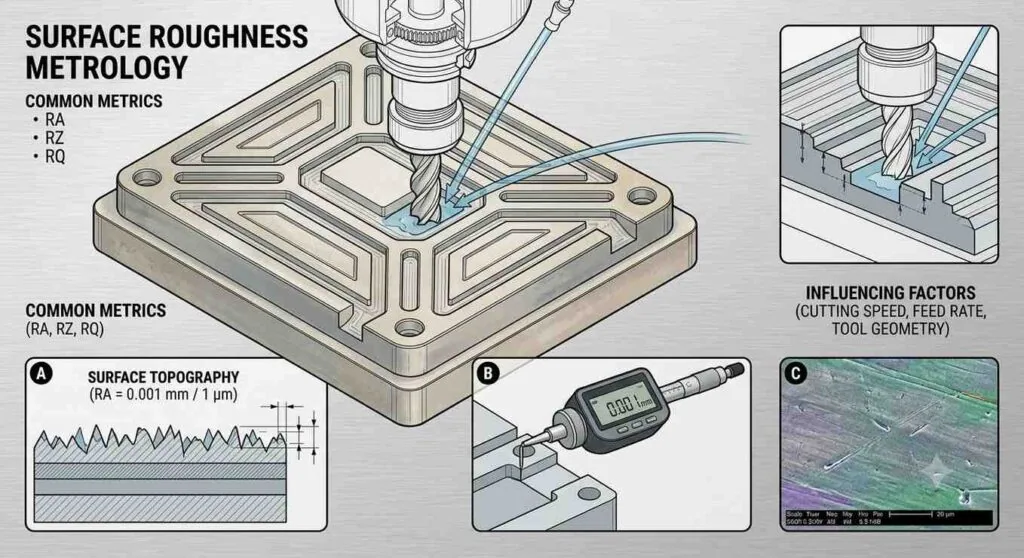
- Machined surface texture and applied finish are separate requirements. MW+ machines to Ra 3.2µm as-machined, Ra 0.4µm fine-machined and Ra 0.1µm polished; roughness parameters are defined in ISO 21920-2 (superseding ISO 4287).
- Masking is a line item, not an assumption. Threads, bearing bores, sealing faces and electrical contacts must be named on the drawing if they are to stay uncoated.
- Finishing is usually a queue, not a machine. Its lead time is set by the finisher’s batch schedule and process cycle, which is why an expedite premium on machining rarely moves the finish date.
- What does a surface finish actually do for a machined part?
- Comparing the main finishing processes
- Anodizing, plating and conversion coatings
- What does passivation do, and when is it required?
- How does a finish affect the part’s tolerances?
- What a complete finish callout must contain
- How much does finishing add to cost and lead time?
- When a coating is the wrong answer
- Frequently asked questions
What does metal surface finishing actually do for a machined part?
A surface finish on a machined part performs one or more of five jobs: it resists corrosion, it increases surface hardness and wear life, it changes electrical behavior by insulating or improving conductivity, it controls appearance, and it changes friction at a sliding interface. Naming which of the five you actually need is the whole specification problem, because processes that excel at one are often poor at another.
Hard anodize is a good example. It is an excellent wear surface and an electrical insulator, which makes it wrong for a part that must earth through its mounting face. Zinc plate protects steel well and looks acceptable, but it is soft and will not survive a bearing interface. The finish is not a grade of quality; it is a function.
Comparing the main finishing processes
Use this table to shortlist a process against your substrate and the job you need it to do. Thickness ranges are typical specification bands rather than limits, and the dimensional column is the one most often overlooked at drawing stage.
| Process | Substrate | Primary function | Typical thickness (µm) | Effect on dimensions |
|---|---|---|---|---|
| Sulfuric acid anodize | Aluminum alloys | Corrosion resistance, dye color, mild wear | 5 to 25 | Grows both into and out of the surface |
| Hard anodize | Aluminum alloys | Wear resistance, electrical insulation | 25 to 75 | Significant; must be allowed for before machining |
| Zinc electroplate | Iron and steel | Sacrificial corrosion protection | 5 to 25 | Adds material; thickness classes defined in ASTM B633 |
| Electroless nickel | Steel, aluminum, copper alloys | Uniform corrosion and wear protection | 10 to 50 | Adds material very evenly, including inside bores |
| Powder coat | Steel, aluminum | Appearance, weathering, edge protection | 60 to 120 | Thick; unsuitable for close-fitting features |
| Passivation | Stainless steel | Restores the passive chromium oxide layer | No measurable build-up | None |
| Bead blast | Most metals | Uniform matte texture, removes tool marks | Surface treatment only | Slight material removal; can round sharp edges |
Anodizing, plating and conversion coatings
Anodizing
Anodizing is an electrochemical process that converts the surface of an aluminum part into a hard, porous oxide layer which is then sealed. Because the layer is grown from the parent metal rather than deposited onto it, roughly half its thickness is consumed from the original surface and half stands proud. Anodic oxide coatings on aluminum are specified in ASTM B580.
Three items decide the result and all three must appear on the drawing: the coating class or type in common industry use, the thickness, and the seal. Alloy matters too — the same process on 6061 and on 7075 will not produce the same color, so specify the alloy in the finish note as well as the material block.
Electroplating
Electroplating deposits metal onto the part from solution using an applied current, so it adds thickness rather than converting the surface. The current density is uneven, which means outside corners plate thicker than inside corners and deep bores plate thinly or not at all. Where a bore must be protected, electroless nickel is the more predictable choice because it deposits chemically and therefore evenly.
Conversion coatings
A conversion coating chemically reacts with the substrate to form a thin protective film, most commonly as a paint pretreatment or as a conductive finish on aluminum. Its value is that it adds almost no thickness and, in the conductive variants, keeps a surface electrically usable. It is the right answer when a part must be both protected and grounded.
Powder coating
Powder coating applies a dry polymer electrostatically and cures it under heat, producing a thick, tough, decorative film. Its thickness is its limitation: at 60 to 120 µm it swamps precision features, will not hold a thread, and must be masked away from anything that locates or seals. It suits enclosures, frames and covers rather than fitted components — see MW+ machine parts.

What does passivation do, and when is it required?
Passivation removes free iron and other contaminants from the surface of a stainless steel part and allows the protective chromium oxide layer to re-form fully. It is a chemical treatment rather than a coating, adds no measurable thickness, and changes no dimension. It is required whenever machining, grinding or handling has embedded iron particles into a stainless surface, which is almost always.
Specify it against ASTM A967/A967M and state whether nitric acid or citric acid treatment is acceptable, because they are not interchangeable for every application. State the verification test as well; without one, “passivated” is an unverifiable claim on a certificate. Machined stainless components are covered on the CNC precision parts page.
How does a finish affect the part’s tolerances?
A finish changes the finished size of every coated feature, and the change is not always equal to the coating thickness. Plating adds its full thickness per surface, so a diameter grows by twice the thickness. Anodizing grows outward by roughly half its thickness while consuming the other half, so a bore both shrinks and hardens. Neither effect is visible on the machining drawing unless you put it there.
| Process | Dimensional effect per surface | How to handle it on the drawing |
|---|---|---|
| Sulfuric anodize | Grows out by about half the coating thickness | State whether the dimension applies before or after finish |
| Hard anodize | Same behavior, larger magnitude at 25 to 75 µm | Machine undersize deliberately, and say so in the note |
| Electroplate | Adds the full deposited thickness | Give the thickness class and mask fitted features |
| Electroless nickel | Adds thickness evenly, including in bores and threads | Allow for it on both mating parts, not just one |
| Powder coat | Adds 60 to 120 µm and bridges small radii | Mask all fitted, threaded and sealing features |
| Bead blast | Removes a small amount and rounds sharp edges | Exclude sealing edges and datum surfaces from the callout |
The safest convention is to state explicitly whether each toleranced dimension is before or after finishing. MW+ holds general machining to ±0.01mm against ISO 2768-m, precision features to ±0.005mm and critical features to ±0.001mm — and a 25 µm coating is 0.025mm, which is five times the precision band. Coating thickness is not a rounding error.
Worked example: what a 25µm hard anodize does to a sliding fit
Take a Ø20.000mm aluminum spigot that has to run inside a Ø20.030mm bore, a nominal diametral clearance of 0.030mm. Specify hard anodize at 25µm (0.025mm) per surface, on the spigot only:
- The coating grows outward by about half its thickness: 0.025 ÷ 2 = 0.0125mm per surface.
- A diameter has two surfaces, so the spigot grows by 2 × 0.0125 = 0.025mm, finishing at 20.000 + 0.025 = Ø20.025mm.
- Clearance left: 20.030 − 20.025 = 0.005mm, against 0.030mm before coating. (0.030 − 0.005) ÷ 0.030 = 83% of the fit consumed.
Now coat the bore to the same specification. It closes by the same 0.025mm: 20.030 − 0.025 = Ø20.005mm. Against a Ø20.025mm spigot that is an interference of 0.020mm, and the two parts will not assemble at all. The fix is arithmetic rather than chemistry: machine the pre-finish spigot at 20.000 − 0.025 = Ø19.975mm and the pre-finish bore at 20.030 + 0.025 = Ø20.055mm, then state on the drawing that the toleranced dimensions apply after finishing.
Electroplating does not behave the same way. It is additive rather than conversion, so it deposits its full thickness on each surface: the same 25µm specification would grow that diameter by 0.050mm, twice the anodize figure. Run the number for the actual process before assuming a coating is thin enough to ignore.
What a complete finish callout must contain
A complete callout removes every decision the finisher would otherwise make on your behalf. Work down this table when writing the note, and the quote that comes back will price the part you meant rather than the safest reading of an ambiguous line.
| What to state | Why it matters | What happens if you omit it |
|---|---|---|
| Process and class or type | Distinguishes decorative from wear-rated coatings | The cheapest variant is supplied |
| Thickness, with tolerance | Sets both corrosion life and dimensional growth | Minimum thickness is applied, and fits change unpredictably |
| Surfaces included and excluded | Threads, bores, sealing faces and earth points usually must stay bare | Everything is coated, and fitted features need rework |
| Corrosion requirement | Turns “corrosion resistant” into a testable number | No acceptance criterion exists, so nothing can be rejected |
| Color and gloss | Dye and gloss vary by alloy, batch and supplier | Batch-to-batch color variation becomes your problem |
| Seal or post-treatment | An unsealed anodize is porous and stains readily | The coating fails early in service rather than at inspection |
| Before or after finish dimensions | Decides who compensates for coating build-up | Both parties assume the other did, and the fit is wrong |
Add the documentation requirement in the same note. A certificate of conformance, a CMM inspection report and material certificates ship with every MW+ order, and any finishing-specific evidence — thickness readings, adhesion or salt-spray results — should be requested explicitly rather than assumed. The inspection regime is set out on the MW+ quality assurance page.

How much does finishing add to cost and lead time?
Finishing adds cost in proportion to surface area, masking labor and batch handling, and it adds lead time in proportion to the finisher’s queue and process cycle rather than to your part count. That distinction matters: a single small part and a hundred of them often carry a similar schedule impact, because both wait for the same tank and the same batch.
| Cost or schedule driver | Why it costs | What reduces it |
|---|---|---|
| Masking | Manual work applied per part, per feature | Reduce the number of excluded features; group them |
| Surface area | Chemistry, energy and rack space scale with area | Coat only the surfaces that need it |
| Batch scheduling | The finisher runs racks in tank order, not in your order | Book capacity in advance; avoid split shipments |
| Color or gloss matching | Setup, sample approval and possible rework | Accept a standard color where function allows |
| Test evidence | Salt-spray and adhesion testing take real elapsed time | Test on a coupon batch rather than per shipment |
| Rework after coating | Stripping and recoating consumes a second full cycle | Get the masking and thickness right the first time |
Because the finishing queue sits outside the machine shop’s control, paying to expedite machining rarely pulls in a finished delivery date. MW+ quotes within 24 hours and completes volume production in 10 to 15 business days; a finish requirement should be added to that window rather than assumed inside it. For early-stage parts where finish is cosmetic only, see MW+ CNC prototyping.
When a coating is the wrong answer
A coating is the wrong answer whenever it defeats a function the part already performs, or whenever the real problem is material selection rather than surface protection. Adding a finish “for protection” without checking what it does to fit, conductivity, fatigue or cleanliness is one of the most common ways a well-machined part fails in service.
| Situation | Why the coating hurts | Do this instead |
|---|---|---|
| Part must earth through its mounting face | Hard anodize is an electrical insulator | Use a conductive conversion coating, or mask the contact face |
| Close-fitting bore or press fit | Coating build-up consumes the fit clearance | Mask the feature, or machine undersize and state the intent |
| Fine external threads | Coating bridges the flanks and the thread no longer gauges | Mask the thread, or coat before thread cutting |
| Cyclically loaded steel part | Some plating processes can degrade fatigue performance | Review the process with the design authority before specifying |
| Corrosion problem caused by the wrong alloy | A coating hides the issue until the first scratch | Change the substrate — see MW+ material capability |
| Sub-millimeter features | Coating thickness is a large fraction of the feature itself | Leave bare, or use passivation — see micro-machining |
The general rule is that a finish should be the last decision, not the first. Establish the material, the fits and the electrical requirements, then choose the smallest surface treatment that closes the remaining gap.
Frequently asked questions
Should I dimension the part before or after finishing?
State it explicitly, either way. Dimensions after finish are the normal convention for functional features, because that is the condition the part is used in, and the shop then machines undersize to allow for build-up. Dimensions before finish are acceptable if the note says so. What causes failures is leaving it unstated, because both parties assume the other has compensated.
How do I specify corrosion resistance in a way a supplier can be held to?
Give a test method and a duration rather than an adjective. A salt-spray requirement stated against ASTM B117, with the hours to first corrosion and the acceptance criterion, is measurable and therefore enforceable. “Corrosion resistant” is not a specification and cannot be the basis of a rejection.
Why did the same anodize color come out differently on two batches?
Anodize color depends on the alloy, the mill batch of the material, the coating thickness and the dye process, so variation between runs is normal rather than a defect. If color matters, specify the alloy in the finish note, fix the thickness with a tolerance, and approve a physical reference sample that later batches are compared against.
Can threads be anodized or plated?
They can, but the coating adds material to both flanks and the effective pitch diameter grows, so a thread that gauged correctly before finishing may not afterwards. On fine threads the usual solutions are masking, or cutting the thread after coating. Decide which at drawing stage, because it changes the process route and the price.
Is bead blasting a finish or a preparation step?
It is both, which is why it needs stating clearly. As a final finish it gives a uniform matte appearance and hides tool marks; as a preparation step it provides the key that anodize or paint adheres to. Specify the media and the intent, and exclude sealing edges and datum surfaces, because blasting rounds sharp corners.
Does a machined surface finish requirement replace a coating requirement?
No — they are separate axes and both may be needed. Machined texture describes the surface the cutter leaves, from Ra 3.2µm as-machined through Ra 0.4µm fine-machined to Ra 0.1µm polished under ISO 21920-2 (superseding ISO 4287). The coating then sits on that surface, and a rough substrate will show through a thin coating rather than being hidden by it. The texture requirement is a separate exercise from the coating requirement, and it is set out in our Ra guide for CNC parts and in the detail on specifying surface finish Ra.
What documentation should I ask for with a finished part?
Ask for coating thickness readings with the measurement locations named, the process record identifying the chemistry and the batch, and any test evidence you specified such as adhesion or salt-spray results. A certificate of conformance, a CMM inspection report and material certificates ship with every MW+ order; finishing evidence should be requested explicitly. To review a drawing and its finish note, use MW+ contact.