The main difference in 304 vs 316 stainless steel is molybdenum alloying: 316-family grades offer improved resistance to pitting and crevice attack compared with 304-family grades in relevant chloride exposure. Both are austenitic stainless steels. That difference supports considering 316 when the environment requires it, but does not make 316 immune to corrosion or automatically the stronger, more machinable choice. The selected product, condition and environment must be checked together. [1] [2] [9]
This guide helps engineers and procurement teams compare grade requirements for a machined component. It separates manufacturer data, engineering recommendations and a hypothetical calculation. It does not establish a service-life prediction, an approved material substitution or an MW+ customer result.
Photos are existing MW+ library illustrations; they do not identify alloy grade or document a customer project.
Contents
304 vs 316 stainless steel: the practical comparison
| Question | 304 / 304L family | 316 / 316L family | Decision implication |
|---|---|---|---|
| Alloy family | Chromium-nickel austenitic stainless | Chromium-nickel-molybdenum austenitic stainless | Identify the full grade rather than ordering “stainless.” |
| Representative grade | 304: UNS S30400 / EN 1.4301 | 316: UNS S31600 / EN 1.4401 | Specify the governing product standard and permitted equivalence. |
| Low-carbon variant | 304L: UNS S30403 / EN 1.4307 | 316L: UNS S31603 / EN 1.4404 | Review welding and subsequent thermal exposure separately. |
| Chloride-related localized corrosion | Lower resistance than the molybdenum-alloyed comparison | Improved resistance; still exposure-dependent | Check fluid, temperature, deposits and crevice conditions. |
| Machining | Austenitic work-hardening behavior requires process planning | The same family-level issue applies | Use actual stock, tooling and operation data; do not assume a universal cost ratio. |
A useful first decision is whether the corrosion requirement has been defined well enough to select either family. If the only requirement is “must not rust,” stop and ask for the fluid, cleaning process, temperature and installation details. That request is an engineering recommendation based on the environment dependence described by Outokumpu. [5]
Specify the grade, variant and product form
Outokumpu’s representative typical compositions are 18.1% chromium and 8.1% nickel for Core 304/4301, versus 17.2% chromium, 10.1% nickel and 2.1% molybdenum for Supra 316/4401. These are producer typical values by mass, not the universal composition limits of every heat. Do not use them as purchasing acceptance ranges. [3] [4]
The practical callout should identify the required designation, product specification, delivery condition and documentation. Alleima lists ASTM A276 and A479 among the standards for its cited bar products; Outokumpu’s flat-product datasheets address different product forms. A sheet-property table therefore should not silently become the acceptance requirement for a machined bar component. [3] [8] [9]
For the drawing review, write down whether substitutions are allowed, who approves them and which properties must be preserved. Matching a familiar grade name is only the beginning of that review. Ask the material supplier to confirm the ordered standard and condition on the quotation and certificate rather than relying on an informal cross-reference alone.
Compare corrosion resistance against the actual exposure
Separate corrosion resistance from immunity
Stainless steel relies on a passive surface film, but its behavior depends on chemistry and the environment. Outokumpu identifies temperature, pH, surface condition, contamination, fabrication and maintenance as relevant factors. Its corrosion overview also explains that molybdenum benefits localized-corrosion resistance without establishing a universal performance guarantee. [5]
As a design recommendation, build an exposure record with separate entries for normal operation, shutdown, cleaning and accidental contact. Record the actual chemicals, concentrations and temperature ranges. Mark unknown entries explicitly. A missing cleaning-fluid specification should remain an unresolved requirement, rather than becoming an assumed reason to accept either alloy.
Review deposits and crevices
Pitting is localized attack on an exposed surface; crevice attack develops in confined regions such as joints or under deposits. The two are related to passive-film breakdown, but their geometries differ. A grade upgrade alone should not close a review of trapped liquid or an inaccessible joint. [5]
Outokumpu’s Supra datasheet cautions that aggressive marine splashing, high chloride loading, heat or humidity can require higher-alloyed materials. It also warns that hydrochloric acid can attack these grades. Consequently, “316” should not be used as shorthand for suitable seawater immersion or arbitrary chemical service. [4]
Do not overlook stress corrosion cracking
Alleima identifies susceptibility of austenitic steels to stress corrosion cracking when tensile stress coincides with certain environments, particularly chlorides, at elevated temperatures. Its 316/316L datasheet recommends considering more resistant material families where that failure mode governs. A favorable pitting comparison does not resolve cracking resistance. [9]
The release recommendation is to have the application owner assess the actual failure modes. Keep the record explicit about which evidence covers surface staining, localized attack, cracking or contamination. Avoid treating one successful coupon test as evidence for every assembly condition.
304L and 316L: what low carbon changes
Outokumpu describes 304L and 316L as low-carbon alternatives that reduce carbide precipitation associated with heat input and improve resistance to intergranular corrosion after welding. The L designation addresses that concern; it does not replace the molybdenum distinction between the 304 and 316 families. [1] [2]
For a fully machined component, ask whether welding, brazing or another subsequent thermal operation is part of the released route. For a welded assembly, identify the applicable joining specification and the finished-state requirements. These are review questions, not a recommendation to change every 304 drawing to 304L or every 316 drawing to 316L.
If a supplier proposes dual-certified stock, request the certificate and approval against every ordered requirement. Do not approve it from the stock label alone. Keep the material decision connected to the component’s actual drawing revision and downstream operations.
Compare mechanical data on the same basis
The cited Alleima Sanmac bar datasheets illustrate why “316 is stronger” is an unreliable purchasing rule. At 20°C, both list a minimum 0.2% proof strength of 205 MPa. Their tensile-strength ranges differ slightly, but these values belong to the specified manufacturer products and delivery conditions. They are not general allowables for every 304 or 316 component. [8] [9]
| Published characteristic | Sanmac 304/304L bar | Sanmac 316/316L bar | Limit of comparison |
|---|---|---|---|
| 0.2% proof strength at 20°C | Minimum 205 MPa | Minimum 205 MPa | Specific producer bar data; not a design allowable. |
| Tensile strength at 20°C | 515–680 MPa | 515–690 MPa | Compare the ordered standard, dimension and condition. |
| Published density | 7.9 g/cm³ | 8.0 g/cm³ | Useful for the illustrative mass calculation below. |
For structural acceptance, request the properties required by the governing calculation and product specification. Keep temperature, condition and loading assumptions visible. Specify whether acceptance depends on proof strength, tensile strength or an application-specific fatigue assessment, instead of treating the table as approval.
Plan stainless steel machining around the actual stock
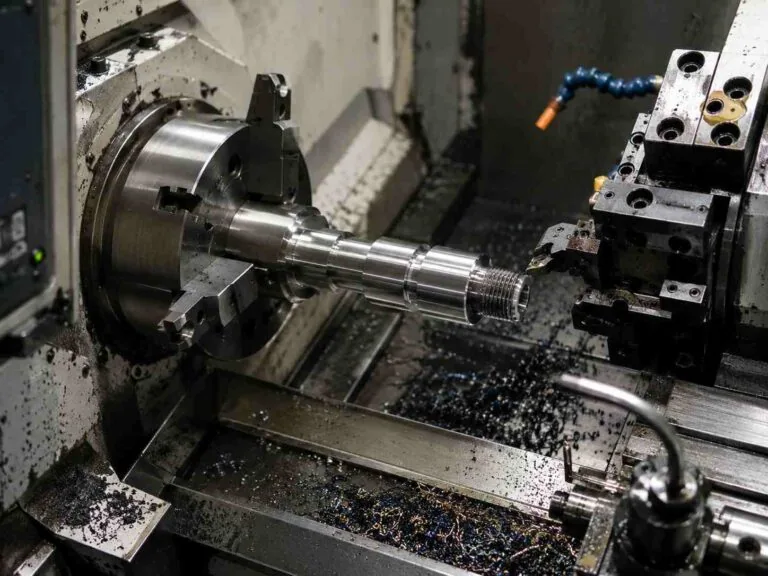
Alleima’s machining guidance identifies pronounced work hardening in austenitic stainless steels, difficult chip breaking and the importance of tool condition, coolant, stable workholding and limited tool overhang. Those issues apply to process planning for both families. [6]
An actionable manufacturing review should ask how chips will leave a deep bore, when a worn cutting edge will be replaced and how the part will be supported during its critical finishing operation. These are engineering recommendations derived from that guidance, rather than universal feeds, speeds or tolerance promises. [6]
A machinability ranking needs its reference conditions
Outokumpu’s standard-grade machining guideline uses a specified reference grade and separates cemented-carbide from high-speed-steel comparisons. Its figures are not a guarantee that a given part will take a fixed percentage longer in 316. Ask for the operation, tool and actual stock behind any quoted machining comparison. [7]
Grade variants matter too. Outokumpu offers Prodec versions with improved machinability, and Alleima describes its Sanmac concept in the cited product sheets. These are manufacturer-specific products. Their existence supports asking about the stock route; it does not establish that MW+ stocks those brands or delivers the same published improvements. [8] [9] [10]
For a fair quotation comparison, give suppliers the same geometry, quantity, approved material condition, finish and inspection requirements. Request separate explanations for stock availability, machining effort and downstream work. An unexplained total-price difference does not establish a universal price premium for one grade.
Worked example: mass and strength screening
Hypothetical inputs: a component has a finished volume of 100 cm³ and an assumed nominal stress of 50 MPa for a simple comparison. Neither value comes from a real customer drawing. Use the manufacturer densities and minimum proof strengths in the preceding table solely to demonstrate arithmetic. [8] [9]
- 304/304L example mass: 100 cm³ × 7.9 g/cm³ = 790 g.
- 316/316L example mass: 100 cm³ × 8.0 g/cm³ = 800 g.
- Mass difference: 10 g; relative to 790 g, 10 ÷ 790 × 100 = 1.27%.
- Minimum proof-strength-to-assumed-stress ratio: 205 MPa ÷ 50 MPa = 4.10 for either cited bar product.
The arithmetic gives no proof-strength advantage to the 316 product under these assumptions. It also shows that the mass difference is small for this particular volume. Neither conclusion resolves the corrosion requirement.
The ratio 4.10 is not an approved safety factor. The example does not include stress concentrations, fatigue, temperature-dependent properties, dimensional variation, manufacturing effects or the application’s acceptance rules. It should prompt a reviewer to request the real analysis, not authorize a substitution. The useful outcome is a list of unresolved requirements with named owners.
A material-selection workflow for a machined component
The following sequence is an engineering recommendation for turning the cited material distinctions into a reviewable decision:
- Define exposure. Separate operating fluids, cleaning chemicals and storage conditions. Record unknowns for resolution.
- Identify failure modes. Ask whether localized corrosion, cracking, contamination or mechanical loading governs the choice.
- Select the candidate product. Identify the full grade, specification and condition, with a documented reason for choosing that family.
- Check manufacturing and downstream work. Include machining access, joining, surface treatment and finished-state inspection.
- Specify evidence. Decide which material certificate, analysis, dimensional report or application test will demonstrate each requirement.
- Approve substitutions explicitly. Record the decision against the drawing revision; leave unresolved conditions open.
Consider a hypothetical washdown bracket: its exposure includes an unspecified cleaner and a bolted crevice. A reviewer can identify 304L and 316L as candidates but cannot responsibly close the selection until the cleaner and service conditions are known. No corrosion result or project success is asserted by this scenario.
Evidence to request before releasing the drawing
| Requirement | Evidence to request | Question the evidence must answer |
|---|---|---|
| Material identity | Certificate tied to the ordered heat and product | Does it match the designation, specification and condition? |
| Low-carbon requirement | Carbon result and an appropriate verification method | Is the L designation substantiated? |
| Corrosion suitability | Applicable producer guidance and application assessment | Does the evidence cover the actual fluids, temperature and joint? |
| Mechanical acceptance | Relevant properties and component calculation | Are the values applicable to the delivered product and service? |
| Finished geometry | Inspection plan with functional datums | Which characteristics are measured after downstream operations? |
| Substitution control | Written approval against the drawing revision | Who authorized the change and which requirements were rechecked? |
For positive material identification, specify what must be measured. Thermo Fisher’s comparison explains that handheld XRF identifies relevant alloying elements but cannot establish carbon-based L/H grade identity; a suitably configured carbon-capable method is needed for that distinction. Instrument selection, calibration and preparation must match the verification task. This guide does not claim that MW+ owns any particular analyzer. [11]
Frequently asked questions
Is 316 always better than 304?
No. Its molybdenum alloying improves the relevant localized-corrosion comparison, but the environment and ordered product still govern suitability. Select against requirements rather than treating the grade number as an overall quality ranking. [2] [9]
Is 316 stainless steel rust-proof in seawater?
No universal seawater guarantee follows from the designation. Outokumpu cautions that aggressive marine conditions may require higher-alloyed materials. Assess the actual exposure, deposits and joint geometry. [4]
Does 316L solve every corrosion problem associated with welding?
No. Low carbon reduces the relevant intergranular-corrosion concern, but that benefit does not establish suitability for every chemical environment or finished assembly. Keep welding and service requirements explicit. [2] [4]
Which grade is easier to machine?
The answer needs the actual stock variant, tooling and operation. Both families require austenitic-stainless process planning; manufacturer machinability comparisons have defined reference conditions. Avoid translating a general ranking into a promised cycle time. [6] [7] [10]
Can XRF confirm that a part is 316L?
Handheld XRF alone cannot substantiate the carbon-based L distinction. Require carbon evidence and a verification method appropriate to that requirement. [11]
Turn the material decision into a machining specification
When the grade is selected, connect it to the component’s critical dimensions, mating interfaces and finished-state inspection plan. The precision machined components page is the relevant component destination. Material choice should accompany those requirements, rather than appearing as an isolated stock note.
For a machining enquiry, provide the drawing, model, approved material specification, quantity, surface requirements and evidence checklist through the CNC machining services page. Use the MetalWorksPlus homepage for company-level context. Ask for review of the stated requirements without assuming a particular stock brand, test facility or guaranteed result.
Technical references
- Outokumpu Core grades.
- Outokumpu Supra grades.
- Outokumpu Core range datasheet.
- Outokumpu Supra range datasheet.
- Outokumpu corrosion resistance overview.
- Alleima machining stainless and duplex steels.
- Outokumpu machining guidelines for standard austenitic grades.
- Alleima Sanmac 304/304L bar datasheet.
- Alleima Sanmac 316/316L bar datasheet.
- Outokumpu Prodec range.
- Thermo Fisher: selecting tools for stainless steel analysis.