Wire EDM & Sinker EDM Services
Electrical Discharge Machining
Electrical discharge machining for hardened alloys up to 65 HRC, tungsten carbide and Inconel — holding ±0.001 mm on wire-cut profiles. Wire EDM, sinker EDM and small-hole drilling under one roof in Shenzhen, from rapid prototypes to certified production runs, with precision CNC machining and documented quality control on the same site.
Wire EDM · Sinker EDM · EDM Drilling
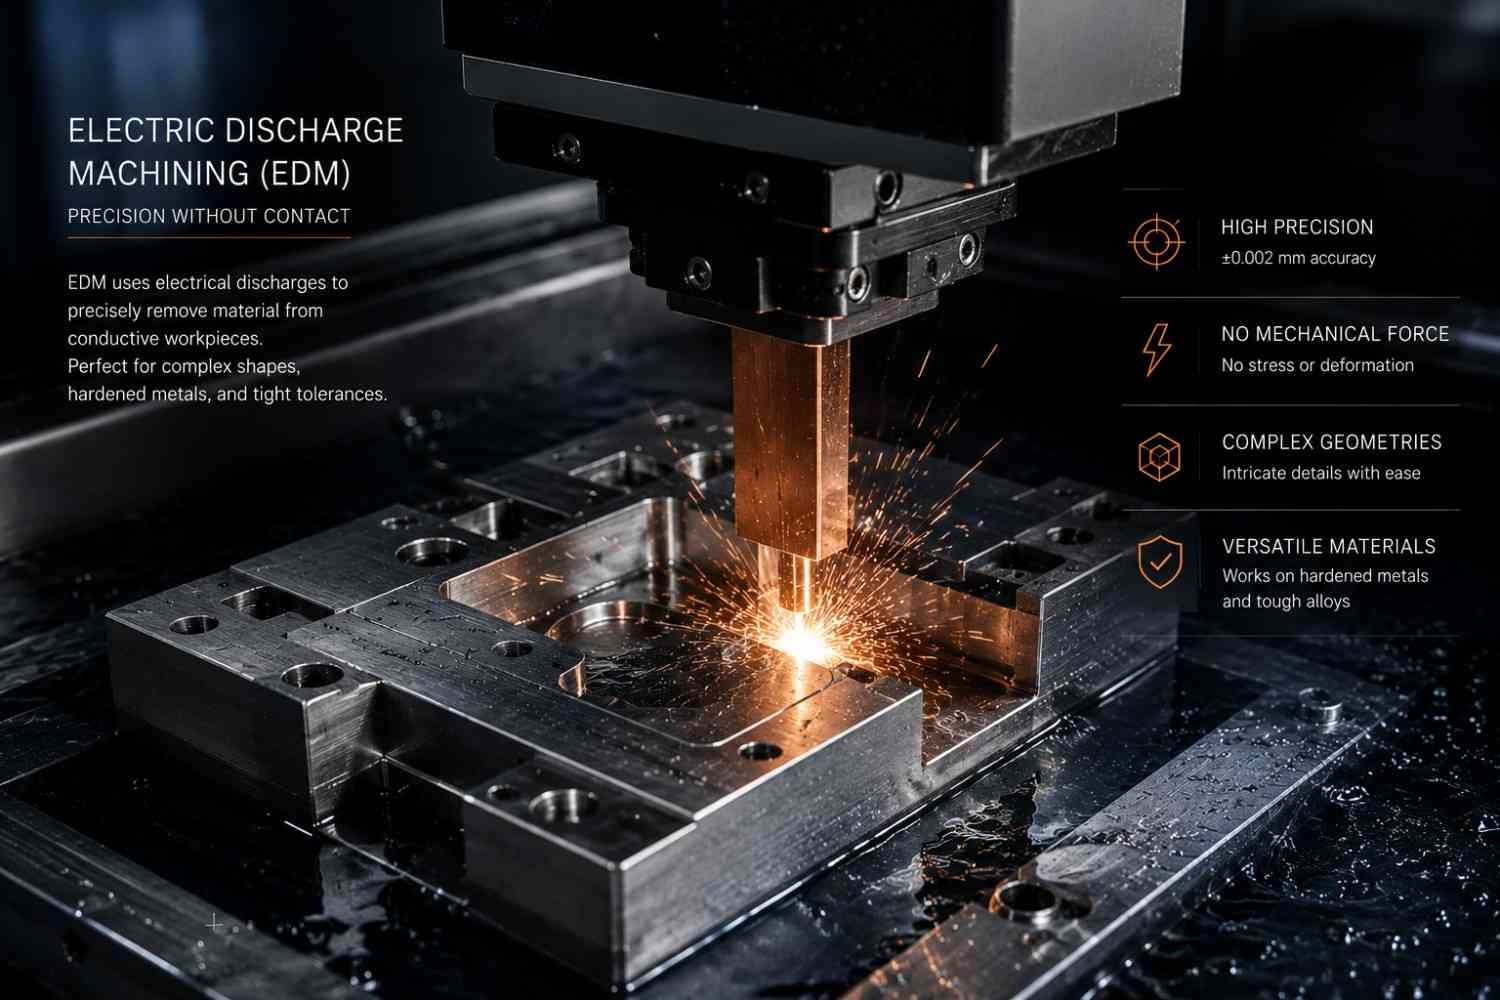
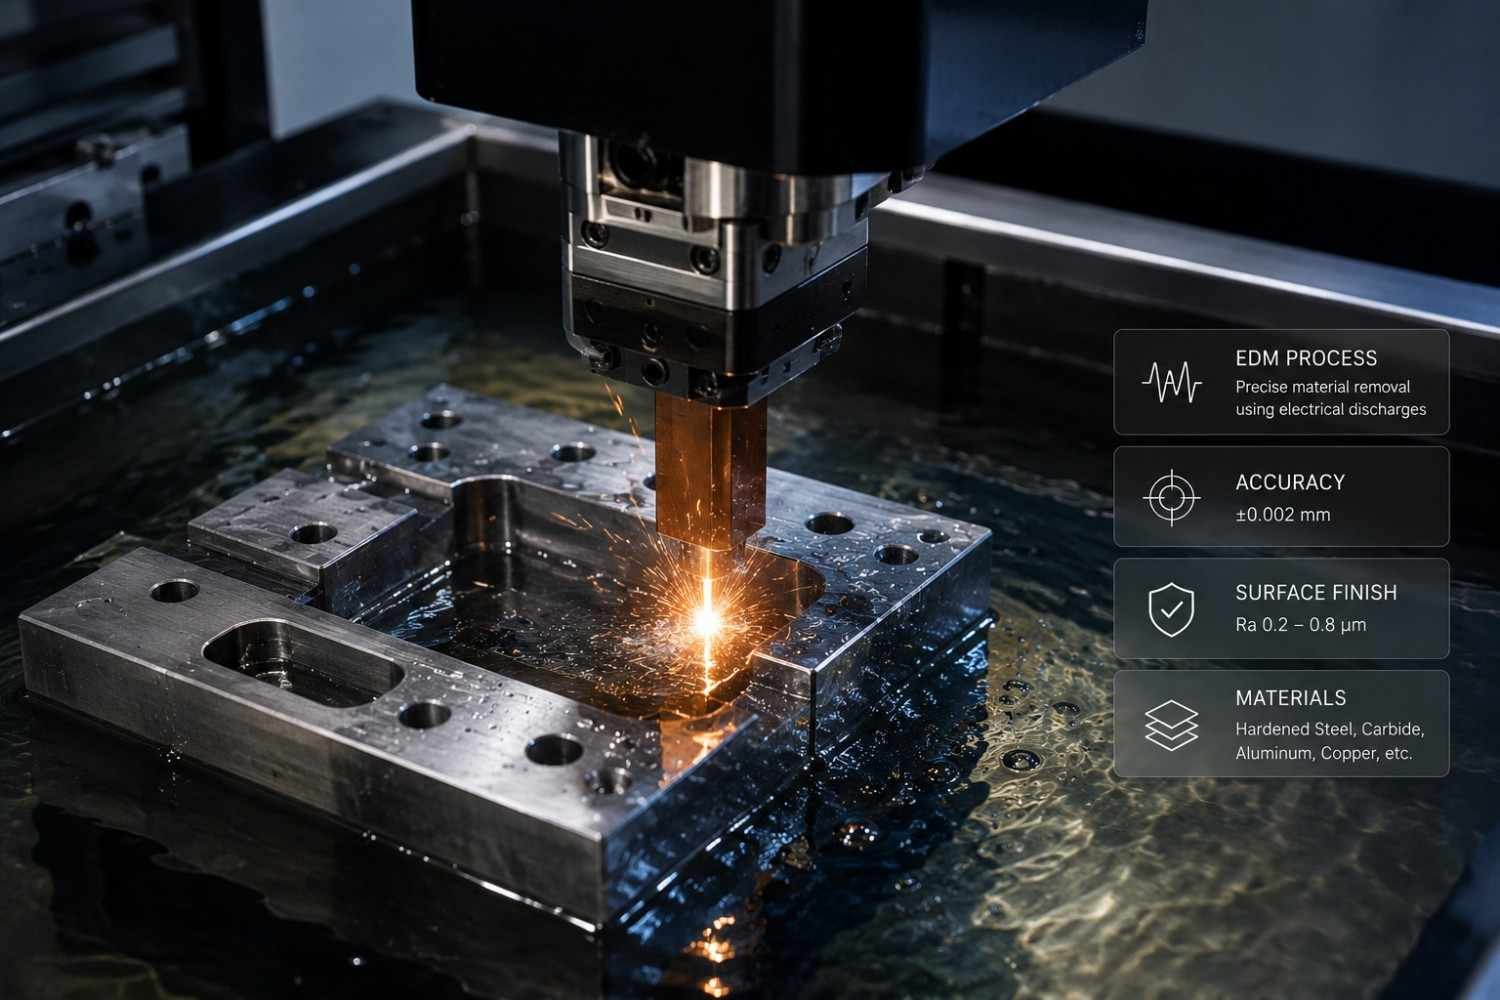
Electrical discharge machining (EDM) removes metal with controlled electrical sparks instead of a cutting edge, so the tool never touches the part and hardness stops being a limit — which is how it holds sharp internal corners and ±0.001 mm profiles in material no cutter will take. MetalWorksPlus runs Sodick AQ750L wire EDM and Makino EDAF3 sinker platforms with adaptive servo control, automated wire threading and real-time spark-gap optimisation, plus a 5-axis small-hole drilling cell for compound-angle work — EDM machining services for tool and die, carbide and Inconel applications.
Wire Electrical Discharge Machining
A continuously fed brass or copper wire (Ø0.02–0.30 mm) cuts through conductive workpieces by controlled spark erosion. Ideal for through-profiles, punch-and-die sets and tool-and-die work with sharp internal corners no grinding wheel can reach. Our engineering guide explains how wire EDM works and what it can hold.
Sinker / Die-Sinking EDM
A shaped graphite or copper electrode descends under controlled Z-axis motion to transfer its geometry into the workpiece — producing blind cavities and 3D features for injection mould cavities, carbide tooling and undercuts. If you are choosing between the two processes, read wire EDM vs sinker EDM: trade-offs and limits.
Small Hole EDM Drilling
High-speed drilling with rotating tubular electrodes creates holes from Ø0.1 mm at depth-to-diameter ratios beyond 50:1 — used for Inconel turbine-blade film-cooling holes and fuel injector nozzles. For features below Ø0.1 mm we move the job to micro-machining.
Our Workshop & Precision Parts
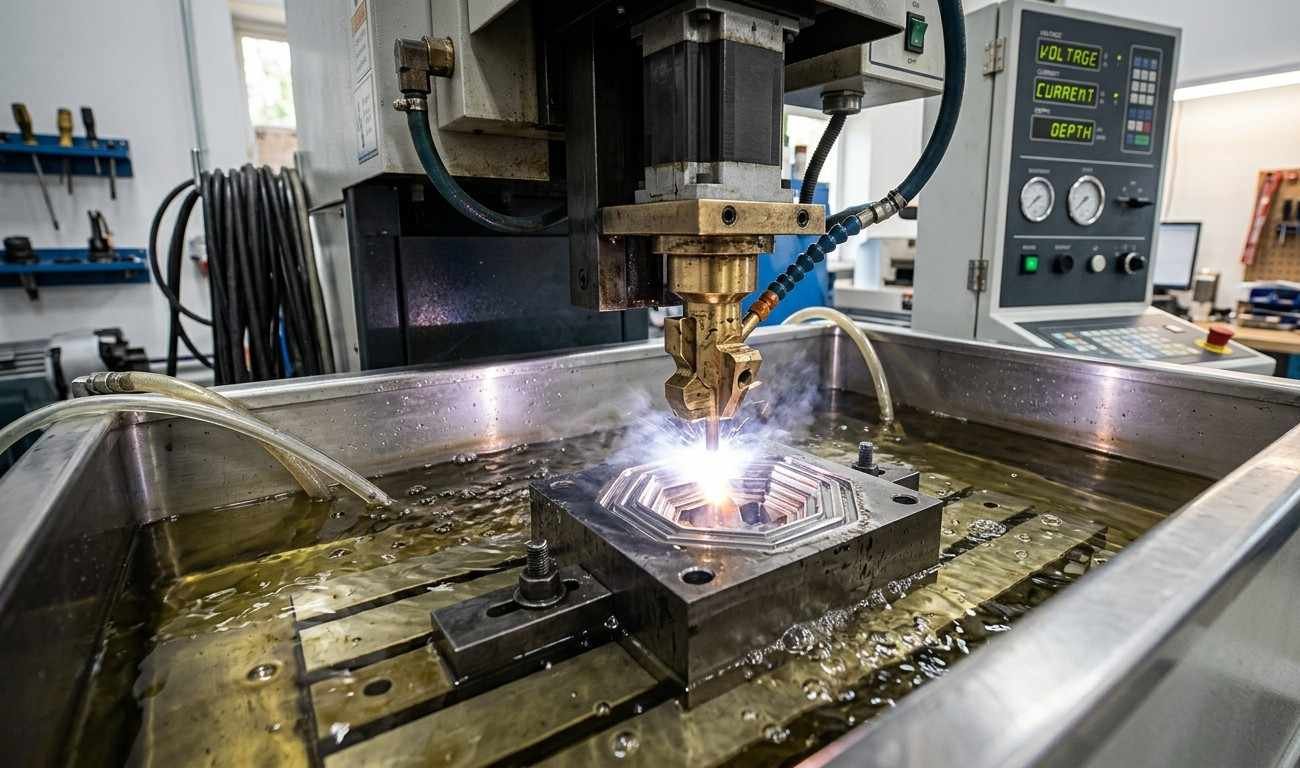
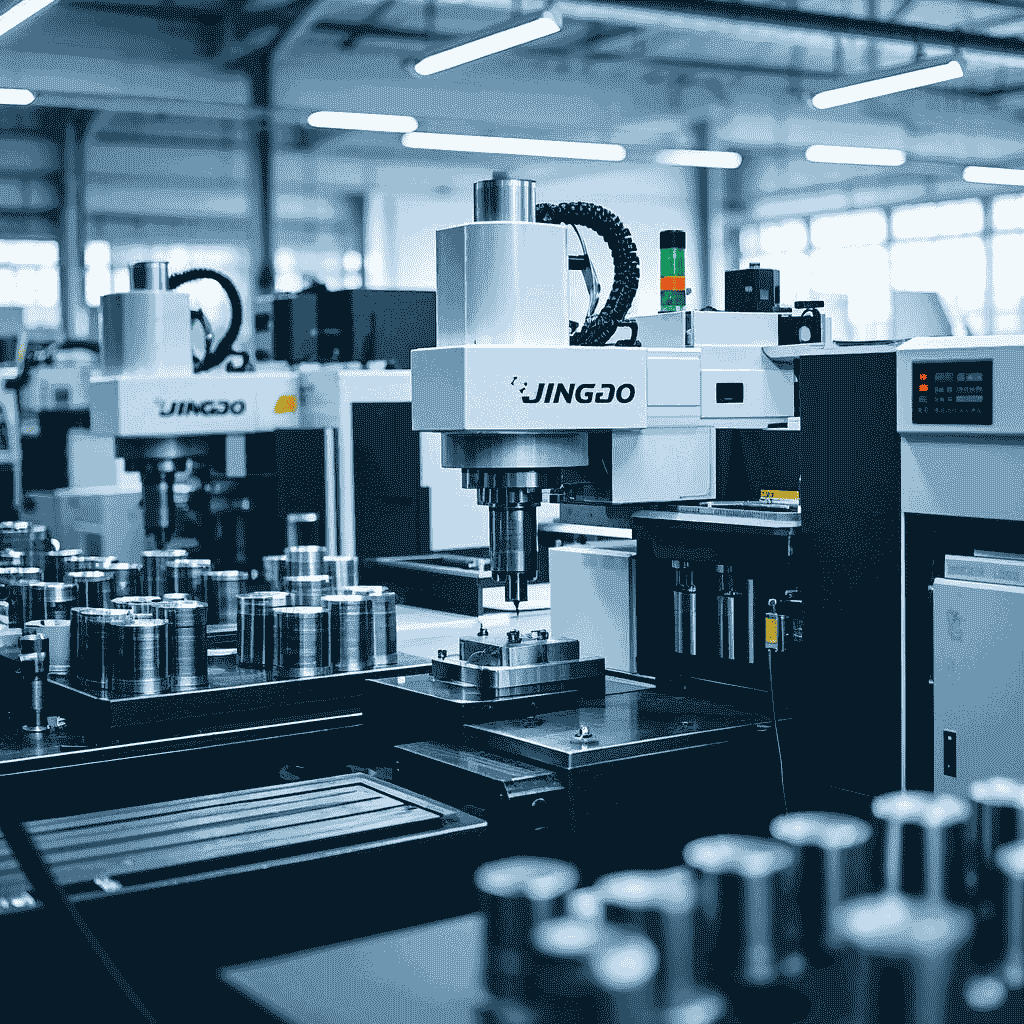
Inside the MetalWorksPlus precision EDM facility, where Sodick and Makino machines deliver micron-level accuracy around the clock.
Why Engineers Trust MetalWorksPlus for Precision EDM
We're not a job shop that does EDM on the side. EDM is our core competency — dedicated machines, dedicated EDM application engineers, and expertise across aerospace, medical, automotive, and precision tooling. Buyers choose MetalWorksPlus as their EDM supplier in China because the wire, sinker and small-hole work, the electrode shop and the CMM inspection all sit under one roof in Shenzhen.
What We Actually Make by EDM
These are the parts leaving our EDM cells week after week — with the process each one runs on and the tolerance it is held to. If your part looks like one of these, we have cut it before and the quote comes back faster.
Progressive & Stamping Dies
Punch plates, die plates, strippers and inserts cut after hardening at 58–65 HRC, so nothing moves afterwards. Internal corners down to R0.05 mm and land clearances built into the cutting path, not ground in later.
Injection Mould Cavities & Inserts
Blind cavities, ribs, undercuts and text detail sunk with graphite and copper electrodes we design and cut in house. Finished to Ra 0.4 µm off the machine, or polished below Ra 0.1 µm for optical and medical tooling.
Turbine & Injector Cooling Holes
Compound-angle film-cooling holes and fuel nozzle orifices at depth-to-diameter ratios beyond 50:1 — the geometry conventional drilling cannot reach in a superalloy without deflecting or work-hardening the wall.
Carbide Extrusion & Wear Dies
Profile dies, drawing dies and wear inserts in tungsten carbide, run on carbide-specific discharge parameters with extra skim cuts so the binder phase at the cut edge is left intact.
Gears, Splines & Form Tools
Involute profiles, spline forms, broaches and gear cutters wire-cut from fully hardened high-speed steel — no post-hardening distortion to grind out, and identical profiles part to part across a batch.
Precision Fixtures & Contacts
Test fixtures, lead frames, RF shielding and sprung contacts where the feature is too fine or too hard to mill. Often paired with our machined connector pins on the same assembly.
MetalWorksPlus vs. a Typical EDM Job Shop
EDM is our core competency, not a side service. Here is what that means when you are evaluating a supplier for a tool-and-die, carbide or Inconel programme — and how it sits alongside the rest of our in-house manufacturing capability.
| Evaluation Criteria | MetalWorksPlus | Typical Job Shop |
|---|---|---|
| Dedicated EDM engineering | ✓ In-house DFM review on every RFQ | Often operator-run, no dedicated review |
| Electrode manufacturing | ✓ Designed & CNC-machined in-house | Frequently outsourced, adds lead time |
| Hardened steel & carbide capability | ✓ Up to 65 HRC steel, 90 HRA carbide | Varies, often limited to softer steels |
| Inconel & superalloy EDM | ✓ Inconel 718, Hastelloy, Waspaloy proven | Limited superalloy experience |
| Dimensional documentation | ✓ Zeiss CMM report + AS9102 FAIR on request | Basic or no inspection report |
| Minimum order quantity | ✓ No MOQ — 1 piece to volume production | Often has minimums for wire EDM |
| Quote response time | ✓ 24-hour guarantee | 2–5 business days is common |
| Certifications | ✓ ISO 9001:2015, AS9100D, ISO 13485, IATF 16949, Nadcap | Varies by shop |
The EDM Machining Process — Step by Step
From CAD file upload to CMM-verified delivery — a transparent, quality-driven engineering workflow for every EDM services order.
Precision EDM — Technical Performance
Verified by Zeiss Contura CMM
Ra <0.1µm Mirror After Polishing
Any Electrically Conductive Alloy
Machines Run Unattended Overnight
EDM Tolerances & Metrology Standards
Traceable measurement via Zeiss Contura CMM, Keyence IM-7030 vision system, and Mitutoyo SJ-410 profilometer. First Article Inspection (FAIR) per AS9102 available.
| EDM Process | Standard Tolerance | High-Precision Capability | Surface Finish Ra | Typical Applications |
|---|---|---|---|---|
| Wire EDM (WEDM) Sodick AQ750L |
±0.01mm | ±0.001–0.005 mm (0.0002") | 0.2 – 0.8µm | Extrusion dies, gears, splines, punch plates and die profiles |
| Sinker EDM (Ram) Makino EDAF3 |
±0.015mm | ±0.008mm | 0.4 – 1.2µm | Mold cavities, blind pockets, aerospace cooling channels, medical tooling |
| EDM Drilling High-Speed |
±0.02mm | ±0.01mm | 0.8 – 1.6µm | Turbine blade cooling holes, fuel nozzles, superalloy micro-holes ≥ Ø0.1 mm |
| GD&T — True Position AS9102 FAIR |
±0.01mm | ±0.001–0.005 mm | — | Flight-critical parts, medical devices, precision fixtures |
All dimensions verified by Zeiss Contura CMM with traceable calibration. Material certifications (MTR) and full traceability documentation provided on request.
Materials We Machine by Precision EDM
Any electrically conductive material — from soft C110 copper to 90 HRA tungsten carbide and Inconel 718 — is processed with equal precision, because spark erosion does not care how hard the workpiece is. Where a part also needs conventional cutting, our CNC machining services cover the same alloy list.
Tool & Die Steels
High wear resistance for punch dies, forging tools, and injection mold inserts — cut after heat treatment at 58–65 HRC, which is where spark erosion earns its keep.
Titanium & Superalloys
Aerospace structural parts and hot-section engine components. Because nothing touches the workpiece, spark erosion avoids the work-hardening and residual stress that conventional cutting leaves behind in these alloys.
Carbides & Conductive Ceramics
Ultra-hard wear parts, cutting tool inserts and guide elements. At commercial scale spark erosion is the only practical way to hold precision in these grades.
Copper, Brass & Alloys
EDM electrodes, electrical connectors, and heat sinks — complex precision geometries machined from solid billets with minimal waste.
Stainless Steels
Medical devices, food-processing equipment and pharmaceutical components. Supplied with mill certificates and full material traceability so your ISO 10993 biocompatibility evaluation has the documentation it needs.
High-Speed Steels
Broaches, form tools, gear cutters, and hobs — post-hardening EDM avoids thermal distortion after full hardening cycle.
The Machines That Cut Your Part
EDM is a dedicated cell here, not a machine borrowed between milling jobs. Every platform below is ours, in our Shenzhen plant, run by EDM engineers rather than shared operators — which is what lets us quote in 24 hours and hold the tolerances on this page.
| Platform | Process | Held Tolerance | Surface Finish Ra | What It Runs |
|---|---|---|---|---|
| Sodick AQ750L Submerged wire |
Wire EDM · Ø0.02–0.30 mm wire | ±0.001–0.005 mm | 0.2 – 0.8 µm | Die plates, punches, gear and spline profiles, carbide dies, taper cuts to ±30° |
| Makino EDAF3 Ram / die-sinker |
Sinker EDM · graphite & copper electrodes | ±0.008 mm | 0.4 – 1.2 µm | Mould cavities, blind pockets, undercuts, ribs, cavity text and logos |
| High-speed drilling cell 5-axis positioning |
Small-hole EDM · rotating tube electrode | ±0.01 mm positional | 0.8 – 1.6 µm | Cooling holes from Ø0.1 mm, start holes, injector orifices, aspect ratios past 50:1 |
| Electrode shop In-house CNC |
Graphite & copper electrode milling | Designed per cavity | — | Rough, semi and finish electrode sets, stored for repeat orders |
| Zeiss Contura CMM Metrology |
Dimensional verification · Keyence IM-7030 · Mitutoyo SJ-410 | Traceable calibration | Measured, not estimated | First articles, in-process checks, AS9102 FAIR, SPC on repeat production |
Need a part larger than a standard EDM envelope, or a cut height beyond the usual range? Send the model — we will confirm fit against the actual work tank before quoting, rather than after you have placed the order.
What Ships With Every Order
The paperwork is part of the deliverable, not an extra you have to chase. This is what lands in your inbox and in the box.
CMM Inspection Report
Every dimension on the drawing, measured on the Zeiss Contura against traceable calibration — issued with the parts, not on request.
Certificate of Conformance
Signed COC referencing your drawing and revision, so incoming inspection can close the receipt without a phone call.
Material Certificates
Mill certificates (MTR) with heat-lot traceability on every alloy — the documentation your ISO 13485 or AS9100 file needs.
AS9102 FAIR
Full First Article Inspection Report to AS9102 for aerospace and defence programmes, forms 1–3 completed, available on request.
SPC & Cpk on Repeats
Recurring production runs carry statistical process control data and capability indices so you can see the process staying centred.
NDA Before Files Move
We sign your NDA, or ours, before you send a single drawing. Uploaded CAD stays on our server and is never shared or published.
Commercial terms in one paragraph. No minimum order — one prototype or a repeat production schedule, same inspection standard either way. Quotes come back within 24 hours of a readable CAD file. Wire EDM prototypes run 3–5 days, sinker work 5–8 days including electrode manufacture, production batches 5–10 days. We ship DDP to more than 50 countries, so duty and delivery are settled before the parts arrive. Blanket orders and JIT release schedules are welcome, and the electrode set for a repeating cavity stays on our shelf so the second order is faster than the first.
EDM Surface Finishes & Secondary Operations
Complete part finishing under one roof — from as-EDMed surfaces to mirror polish, coatings, and laser marking. No secondary suppliers needed.
As-EDMed Finish
Consistent matte texture, burr-free, recast layer present. Ra 0.8–3.2µm straight off the rough cut with no skim pass — ready for tooling and structural applications. Skim passes take the same surface to Ra 0.2–0.8µm.
Polishing & Lapping
Hand polishing or vibratory lapping achieves Ra <0.1µm mirror finish for optical mold surfaces and medical implants.
Electropolish & Passivation
Electropolishing removes the EDM recast (white) layer; passivation then restores the chromium-oxide film that gives stainless its corrosion resistance — both specified routinely on aerospace and medical parts.
PVD / CVD Coatings
TiN, TiAlN, DLC, and CrN coatings for enhanced hardness and reduced friction in forming and cutting applications.
Post-EDM Heat Treatment
Stress-relief tempering restores bulk material properties and prevents micro-cracking in hardened steels.
Laser Marking & Kitting
Permanent part ID, serial numbers and custom kitting on the same laser equipment we use for sheet work — cleanroom-compatible packaging available.
How EDM Creates Micron Precision
Understanding discharge physics helps engineers design better EDM parts — leveraging unique advantages in materials, geometry, and surface integrity.
EDM Applications Across Key Industries
From flight-critical aerospace components to medical device tooling — MetalWorksPlus EDM serves demanding applications worldwide with ISO-certified precision.
Aerospace & Defense
Turbine blades, cooling holes, flight-critical components, AS9100 programs
Medical Devices
Surgical instruments, implant components, micro-features, biocompatible materials
Tool & Die
Punch-and-die sets, injection mould inserts, extrusion and progressive stamping dies — often supplied with matching machined components
Automotive
Injection molds, gear profiles, fuel system components, transmission parts
Electronics & Semiconductor
Precision connectors, lead frames, test fixtures, RF shielding
EDM Case Studies — Real Engineering Results
Complex precision EDM challenges solved by the MetalWorksPlus engineering team across industry verticals.
Turbine Blade Film Cooling Holes — Inconel 718
Progressive Die in D2 Steel — 62 HRC
Surgical Instrument Mold Cavity — Mirror Finish
Tungsten Carbide Extrusion Die — 89 HRA
EDM Services — Prototype to Production
Flexible EDM service models built around your production requirements — from urgent 3-day prototypes to certified JIT production supply agreements.
Custom EDM Components & Tooling
Complete precision EDM from drawing to finished part — electrode design, wire profiling, sinker cavity work, small-hole drilling and secondary finishing. Parts that need turning or milling after the spark work move straight onto our CNC precision parts line without leaving the building.
- No minimum order — 1 piece to high volume
- Wire EDM prototypes in 3–5 business days
- Complex 3D cavities, deep slots and tool-and-die work
- Tolerances from ±0.001 mm, surface finish to Ra 0.2 µm
- In-house electrode design and CNC manufacturing
- Full CMM inspection report on every delivery
Production EDM & JIT Supply
Recurring production runs for punches, dies, gears, and precision inserts. JIT scheduling, SPC process control, and certified first articles per AS9102.
- Production turnaround: 5–10 business days
- Volume pricing and blanket order agreements
- SPC reports, Cpk analysis, statistical control
- Electrode library stored for instant repeat orders
- DDP shipping worldwide — 50+ countries
- ISO 9001:2015 certified supply chain
Frequently Asked Questions
Common technical and commercial questions about wire EDM, sinker EDM, and EDM drilling — answered by our application engineering team.
Wire EDM uses a continuously moving brass or copper wire (0.02–0.30mm) to cut electrically conductive metal through controlled spark discharges — also called wire erosion. The wire never touches the workpiece; material is removed in a dielectric fluid bath, holding ±0.001–0.005 mm on the cut profile with a Ra 0.2 µm skim finish.
Sinker EDM (ram EDM / die-sinking EDM) lowers a shaped graphite or copper electrode into the workpiece to transfer its geometry — producing blind cavities and 3D features that wire EDM cannot reach. It is the standard method for injection mould cavities and complex tooling.
Yes. EDM is one of the few practical ways to machine tungsten carbide, since spark erosion isn't limited by hardness. We run carbide-specific discharge parameters for extrusion dies, wear parts, and cutting tool components up to 90 HRA.
Yes. EDM is routine for Inconel aerospace and turbine components, avoiding the work-hardening that conventional cutting causes. EDM drilling is also used for high-aspect-ratio holes such as turbine blade film-cooling holes in Inconel 718, Hastelloy, and Waspaloy.
Wire EDM holds ±0.001–0.005 mm (0.0002"), sinker EDM ±0.008mm, and EDM drilling ±0.01mm positional accuracy — each verified by CMM. Surface finish ranges from Ra 0.2 µm after skim passes to Ra 3.2 µm as-EDMed; polishing takes it below Ra 0.1 µm.
Yes. We are based in Shenzhen and ship DDP to more than 50 countries, so duties and delivery are handled before the parts reach you. Standard paperwork with every shipment is the CMM inspection report, a certificate of conformance and the material certificate; AS9102 First Article Inspection Reports are issued on request.
STEP, IGES, DWG, DXF, and PDF drawings are all accepted. 3D STEP files are preferred for sinker EDM electrode design; 2D DXF profiles are sufficient for wire EDM quoting.
Typical lead times: wire EDM prototypes 3–5 days, sinker EDM with electrode manufacturing 5–8 days, EDM drilling 3–5 days, production runs 5–10 days — with a 24-hour quote response guarantee.
Yes. MW+ holds ISO 9001:2015 and AS9100D aerospace quality management certification, plus ISO 13485:2016 for medical device work and IATF 16949:2016 for automotive, with Nadcap accreditation for special processes. Every EDM order ships with a certificate of conformance, a Zeiss CMM inspection report and material certification; AS9102 First Article Inspection Reports are available for aerospace and defence programmes.
Ask for the machine list and the inspection kit before you ask for a price. Check that wire EDM services, sinker work and small-hole drilling run in-house rather than being subcontracted, that electrodes are cut on site, and that the shop can hand you a CMM report measured against your drawing rather than a pass or fail note. Confirm the quality system covers your industry — ISO 9001:2015 for general work, AS9100D for aerospace, ISO 13485:2016 for medical — and agree Incoterms and documentation before the first order. MetalWorksPlus runs all of that from one plant in Shenzhen and ships DDP to more than 50 countries.
Start Your EDM Project Today
Upload your CAD files or send specifications — 24-hour quote response guaranteed. Our EDM application engineers personally review every inquiry for DFM feedback, realistic tolerances, and competitive pricing.
Electric Discharge Machining quote request
EDM earns its place on hardened steel, sharp internal corners and geometry a cutter cannot reach. Send the drawing and we will confirm the right process.