
A machine shop rate looks like one number, but it is really a stack of costs the supplier has to recover for every hour a machine is running. Understanding what is in that stack tells you which parts of a quote you can move with a design change and which parts you cannot move at all.
This article takes the rate apart, then follows the arithmetic that turns an hourly rate into the price of your part. It is written for engineers and buyers who have two quotes in front of them and need to know why they differ.
Key takeaways
- A machine shop rate is built from capital recovery, direct labor, energy, maintenance, tooling, quality-system overhead and margin. Only some of those differ between machines.
- Part price is the machine rate multiplied by cycle time, plus material, plus non-recurring setup divided by the batch quantity, plus secondary operations and inspection.
- The rate is set by the machine; the cycle time is set by your drawing. Design changes move cycle time, not the posted rate.
- Setup, programming, fixturing and first-article inspection are charged per batch, which is why the same part has two very different prices at 10 and 1,000 pieces.
- Certification to AS9100D, ISO 13485 or IATF 16949 sits inside the rate as quality-system overhead. MW+ holds all of these plus ISO 9001:2015 and NADCAP.
- MW+ quotes within 24 hours, has no minimum order quantity, and runs volume production in 10–15 business days.
- What is a machine shop rate, and what is inside it?
- How does an hourly rate become a part price?
- Why do different machines carry different rates?
- What moves cycle time, the other half of the multiplication
- Non-recurring costs and why batch size changes everything
- How certifications sit inside the rate
- How to compare two quotes with different rate structures
- When the lowest hourly rate is the wrong choice
- How MW+ prices custom CNC parts
- Frequently asked questions
What is a machine shop rate, and what is inside it?
A machine shop rate is the hourly charge a supplier applies to time spent on a specific machine. It is assembled from capital recovery on the machine and its tooling, the direct labor to set and run it, energy, maintenance and calibration, consumable cutting tools, the overhead of the quality system, and margin. It is not a price for your part; it is the price of an hour of that machine’s capacity.
The table below separates the parts of the rate that differ between machines from the parts that are roughly constant across a shop. That distinction is what explains why one supplier’s 3-axis rate can be close to another’s while their 5-axis rates are far apart.
| Component of the hourly rate | What it pays for | Varies between machines? |
|---|---|---|
| Capital recovery | Purchase price of the machine, spindle, controller, pallet system and probing | Yes — the largest single difference between a 3-axis mill and a 5-axis machining center |
| Direct labor | Setter and operator time, and how many machines one person can attend | Yes — automated cells and bar-fed lathes need less attendance per hour |
| Tooling and consumables | Cutting tools, holders, coolant, replacement inserts | Yes — driven by what the machine cuts, not by the machine itself |
| Maintenance and calibration | Servicing, ball-bar and laser calibration, spindle rebuilds | Yes — higher on machines held to tighter positional accuracy |
| Energy and facility | Power, compressed air, floor space, climate control | Partly — larger machines and controlled areas cost more per hour |
| Quality-system overhead | Metrology equipment, quality engineers, documentation, audits | No — spread across the whole shop |
| Margin | The supplier’s return | No — usually a shop-wide policy |
How does an hourly rate become a part price?
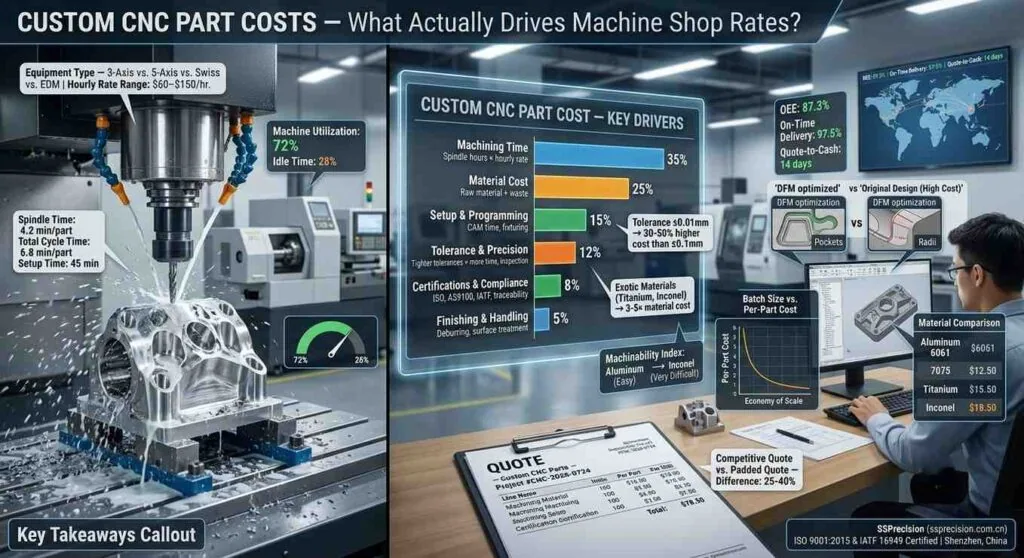
A CNC part price is the machine shop rate multiplied by the cycle time, plus the material blank, plus the non-recurring setup and programming divided by the batch quantity, plus any secondary operations and inspection. The rate is set by the supplier and the machine; the cycle time is set by your drawing. That is why a design change moves the price even though the posted rate never changes.
Two consequences follow. First, comparing suppliers on hourly rate alone is meaningless, because a higher rate on a faster or better-automated machine can produce a lower part price. Second, the lever you actually hold is cycle time and setup count, both of which live on your drawing rather than in the supplier’s rate card.
Why the same part has two prices at two quantities
Setup, programming, fixture build and first-article inspection are non-recurring: they are paid once per batch regardless of how many parts come off. At ten pieces those costs are divided by ten. At a thousand they are divided by a thousand and effectively vanish, leaving cycle time and material to set the price. Our CNC machining cost per part breakdown follows the same arithmetic line by line.
This is why a prototype quote and a production quote for the same model can look like different parts. Always state the quantity and the expected annual volume when you request a price, and ask the supplier to break out the non-recurring line so you can see it.
Worked example: the same part at 10 pieces and at 1,000
Work the arithmetic in machine-hours rather than currency and the quantity effect separates cleanly from the rate. Take a part with an 18-minute cycle that needs 4 hours of CAM programming, 2 hours of fixture build, 1 hour of program proving and 1 hour of first-article inspection.
Step 1. Convert the cycle: 18 ÷ 60 = 0.30 machine-hours per piece. Step 2. Total the non-recurring work: 4 + 2 + 1 + 1 = 8 hours, charged once per batch. Step 3. Spread it across 10 pieces: 8 ÷ 10 = 0.80 hours per piece, giving 0.30 + 0.80 = 1.10 charged hours per piece.
Step 4. Spread the same 8 hours across 1,000 pieces: 8 ÷ 1,000 = 0.008 hours per piece, giving 0.308 charged hours. Step 5. Compare the two: 1.10 ÷ 0.308 = 3.6, so the hour content behind each piece falls roughly 3.6-fold while the hourly rate, the material and the drawing stay identical. Non-recurring work is 73% of the charged hours at ten pieces and 2.6% at a thousand.
The same arithmetic shows what a design change can and cannot do. Cutting two minutes from the cycle saves 0.033 hours per piece at any quantity; removing one setup takes hours out of the non-recurring block, which is worth most at low volume and close to nothing at high volume.
Why do different machines carry different rates?
Different machines carry different rates because they represent different capital investments and require different amounts of operator attention. A simultaneous 5-axis machining center costs far more to buy, maintain and calibrate than a 3-axis vertical mill, and that difference is recovered per hour of use. Rate is a proxy for capability, not for quality. The machine-by-machine picture behind those numbers is set out in our breakdown of the CNC machine hourly rate in China.
| Machine type | Relative hourly rate | Why the rate sits there | Best suited to |
|---|---|---|---|
| CNC lathe (turning) | Lowest | Modest capital cost; bar feeding reduces operator attendance | Shafts, pins, bushings, cylindrical components |
| 3-axis vertical mill | Low | The commodity machine in most shops | Flat parts, plates, enclosures, through features |
| 4-axis mill | Middle | Adds a rotary axis and its own calibration | Features arranged around a cylinder |
| Simultaneous 5-axis mill | High | High capital cost, complex kinematics, longer programming | Compound angles, sculpted surfaces, multi-face parts in one setup |
| Swiss-type lathe | High | Specialised machine and setup, but very low attendance once running | Small, slender, high-volume turned parts |
| Wire EDM | Middle to high | Slow cutting rate, but almost unattended and no cutting force | Hardened material, sharp internal corners, fine details |
Read this table as an ordering, not as a price list, and remember that the highest-rate route is often the cheapest part. A component needing four setups on a 3-axis machine may run complete on a multi-axis machining centre in one, and the setup savings can more than cover the higher hourly rate. The same logic applies to Swiss machining on small turned parts and to wire EDM services on hardened material.
What moves cycle time, the other half of the multiplication
Cycle time is the number of minutes a part occupies the machine, and it is the factor you control from the drawing. Four things move it: the volume of metal to be removed, the machinability of the grade, the tolerance and finish called out, and the number of setups. Each maps to a specific decision you can revisit before requesting a quote.
| Driver | Effect on cycle time | What you control |
|---|---|---|
| Volume of metal removed | Directly proportional; a block that mostly becomes chips is mostly machine time | Stock form — round bar, plate thickness, near-net blank |
| Material machinability | Harder and work-hardening grades run at lower speeds and wear tools faster | The specified grade, where the load case allows an alternative |
| Tolerance class | Tight bands add a finishing pass and in-process gauging | Which features carry ±0.005mm and which sit at the general tolerance |
| Surface roughness | Each step below as-machined is a separate operation | Applying a roughness callout per surface rather than as a blanket note |
| Number of setups | Each setup adds handling, re-datuming and program proving | How many directions a tool must approach the part from |
| Feature accessibility | Small corner radii and deep pockets force small tools at low feed rates | Corner radii, pocket depth, tool clearance |
Two of these deserve a specific note. Tolerance should default to the general class in ISO 2768, with tighter values marked only where a fit or a seal depends on them. Roughness should be specified per surface, because a blanket fine finish converts one finishing operation into one per face. Name the governing standard as well: ISO 4287:1997, which defined Ra for decades, was superseded by ISO 21920-2:2021, and drawings in circulation still use either convention, so the drawing must state which one governs.
Non-recurring costs and why batch size changes everything
Non-recurring engineering on a machined part covers CAM programming, fixture design and build, tool selection, program proving, and the first-article inspection that releases the batch. None of it repeats per piece, and all of it repeats per part number. It is the single biggest reason low-volume precision work feels expensive.
Amortisation and repeat orders
On a repeat order the program and the fixture already exist, so the non-recurring line should shrink dramatically. Ask explicitly whether a repeat order is priced with the setup amortised, because a supplier quoting every batch as if it were the first is quietly charging you twice for work already done.
First article inspection is the other line to watch. Full first article inspection to AS9102 and PPAP Level 3 are documentation packages produced once per part number, and at MW+ they are available on request and quoted per programme rather than bundled into every piece.
How certifications sit inside the rate
A certified quality system is overhead spread across every machine hour in the shop: metrology equipment and its calibration, quality engineers, documented procedures, internal audits and external surveillance. It does not appear as a line on your quote, which is exactly why an uncertified supplier can look cheaper on paper while offering a different product.
| Certification | Sector | What the system adds to the shop |
|---|---|---|
| ISO 9001:2015 | General industrial | Documented quality management, corrective action, supplier control |
| AS9100D | Aerospace | Configuration and risk management, foreign object debris control, first article inspection |
| ISO 13485 | Medical devices | Process validation, device history records, material lot traceability |
| IATF 16949 | Automotive | Advanced product quality planning, statistical process control, PPAP submission |
| NADCAP | Aerospace special processes | Accreditation of individual special processes rather than the whole system |
Capability is the measurable output of that overhead. MW+ holds process capability at Cpk ≥1.67, an index defined and worked through in the NIST/SEMATECH engineering statistics handbook. Ask for a capability study on a comparable feature; it tells you far more than the certificate on the wall.
How to compare two quotes with different rate structures
- Ask both suppliers to quote the same quantity and to state the assumed number of setups and the assumed cycle time.
- Ask for the non-recurring line separately from the per-part price, and ask what a repeat order costs.
- Ask which machine the part is quoted on, because that determines the rate that was applied.
- Ask whether inspection is per batch or per part, and whether the inspection report is included.
- Ask whether finishing is in-house or subcontracted, since an outside process adds both a margin and a queue.
- Ask what documentation ships with the parts, and what is quoted as an extra.
A quote that answers the first two questions is comparable. One that does not is a single number with no structure behind it, and the difference between two such numbers tells you nothing useful about either supplier’s CNC machining services.
When the lowest hourly rate is the wrong choice
The lowest hourly rate is the wrong choice whenever the cheaper machine needs more hours, more setups or more inspection to produce the same part. Rate is only half of the multiplication, and a low rate applied to a long cycle time and four setups routinely loses to a high rate applied to one setup.
| Situation | Recommendation | Why |
|---|---|---|
| The part needs four or more 3-axis setups | Quote it on a 5-axis machine as well | Removing setups usually beats the lower hourly rate |
| Small slender turned parts at volume | Quote Swiss-type turning | Very low attendance per part once running, despite a higher rate |
| Hardened material or sharp internal corners | Quote wire EDM | Milling cannot produce the feature at any rate |
| Regulated aerospace, medical or automotive part | Use a certified supplier | A non-conforming lot or a failed audit costs more than the rate difference |
| The quote omits inspection and documentation | Treat it as incomplete, not cheap | Those costs reappear later, usually at the worst moment |
| Prototype quantities | Compare total batch price, not per-part price | Setup dominates, so the per-part figure is misleading |
| Finishing is subcontracted | Ask for the queue as well as the price | An outside process adds lead time you cannot see in the number |
How MW+ prices custom CNC parts
MW+ is a precision CNC machining supplier operating a 15,000 m² facility at No. 39 Xishi Road, Hewan Community, Guangming, Shenzhen, founded in 2015, with 120+ engineering and quality professionals, 60+ CNC machining centres and 70+ materials, serving customers in 50+ countries. MW+ has no minimum order quantity and runs volumes to 1,000,000+ units.
MW+ returns quotes within 24 hours with the setup and cycle-time assumptions stated, so you can see which half of the multiplication is driving your price. Express prototypes ship in 48 hours, standard prototypes in 3–5 business days, and volume production in 10–15 business days. Process detail sits under CNC milling services and CNC turning services.
MW+ holds general machining to ±0.01mm to ISO 2768-m, precision features to ±0.005mm and a ±0.001mm floor, with surface finish from Ra 3.2µm as-machined to Ra 0.4µm fine-machined and Ra 0.1µm polished. Every order ships with a certificate of conformance, a CMM inspection report and material certificates, under a system certified to ISO 9001:2015, AS9100D, ISO 13485, IATF 16949 and NADCAP. See how that is verified under CNC machining quality control, or request a CNC machining quote with a model and drawing in STEP, IGES, DXF, DWG, SolidWorks or PDF.
Frequently asked questions
Why is a supplier with a higher hourly rate quoting me a lower part price?
Because part price is rate multiplied by cycle time, plus setup divided by quantity. A supplier on a faster or better-automated machine can finish your part in fewer minutes and fewer setups, which more than offsets the higher rate. Compare the quoted part price at a fixed quantity, and ask each supplier how many setups they assumed.
Should I ask my supplier for their hourly rate?
Ask for the assumptions rather than the rate. The useful questions are how many setups the part needs, what cycle time was assumed, what the non-recurring setup costs, and whether inspection is per part or per batch. Those four answers let you compare two quotes; a bare hourly rate on its own does not, because it says nothing about how many hours your part will take.
Why did my price per part fall so sharply at a higher quantity?
Setup, programming, fixture build and first-article inspection are charged once per batch, so they are divided by the number of parts. At low quantities they dominate the per-part figure; at production quantities they are spread thin enough to disappear, leaving cycle time and material. The steeper the drop, the more non-recurring content the part carries.
Does material choice change the hourly rate or the cycle time?
Material changes cycle time and tooling consumption, not the posted rate. Harder and work-hardening grades cut at lower speeds and wear tools faster, so the same geometry occupies the machine for longer and consumes more consumables. Choosing a more machinable grade, where the load case allows it, reduces the hours your part needs rather than the price of an hour.
Is a certified supplier always more expensive?
A certified quality system is real overhead carried in the rate, so on a simple commercial part an uncertified shop can be cheaper. On a regulated aerospace, medical or automotive part the comparison is not like for like, because the certified supplier is delivering traceability and documentation that the other one is not. Compare what ships with the parts, not just the number.
What documentation should I expect to be included in the price?
Every MW+ order includes a certificate of conformance, a CMM inspection report and material certificates at no extra charge. First article inspection to AS9102 and PPAP Level 3 are produced on request and quoted per programme, because both are one-off documentation packages tied to a part number rather than to a piece. Ask every supplier which of these are included.
Which single change usually cuts a custom CNC part price the most?
Reducing the number of setups, because a setup carries handling, re-datuming, program proving and its own positional error budget. After that, moving non-critical features from a blanket tight band to the ISO 2768-m general tolerance is usually the largest single saving, since it removes finishing passes and inspection points across the whole part at once.
A machine shop rate is a capacity price, not a part price. Once you separate the rate from the cycle time, the levers become obvious: fewer setups, a more machinable grade, a stock form closer to the finished envelope, and tight tolerances only where function needs them. Ask suppliers for their assumptions, and the quotes become comparable.



